HSINCHU, Taiwan — June 3, 2021 — Experienced silicone product manufacturer General Silicones (GS) is proud to share the creation of luxury fashion handbags and tote bags using Compo-SiL® vegan leather. The prototypes are designed and manufactured by an experienced local OEM bag manufacturer.
It was the first time for the manufacturing partner to use silicone-based vegan leather.
“It was a pleasant surprise how easy it was for our manufacturing partner to work with Compo-SiL vegan leather,” said Allen Yang, head of Business Development of GS. “Thanks to our patented technology, the bag maker combined our silicone leather without difficulty to the bag’s different inner material with HMA adhesives. Compo-SiL is the only silicone rubber began leather that accepts adhesion with HMA adhesives, giving designers the opportunity to explore the many advantages silicone rubber can add to products to the fullest. The prototypes were created to demonstrate that Compo-SiL is an excellent vegan fabric for the luxury fashion industry.”
An Eco-friendly Alternative to PVC Based Faux Leather
The demand for animal cruelty-free leather alternatives is growing each year. Finding high-quality animal leather alternatives without opting for plastic and harmful PVC-based faux leather products is not always easy. Compo-SiL leather by General Silicones is an eco-friendly fabric made of silicone rubber. Silicone has a low carbon footprint during manufacturing and is environmentally friendly. The material is widely used for skin-friendly baby and medical products for its harmless properties.
A Versatile High-quality Vegan Fabric for Luxury Brands
General Silicones developed the patented Compo-SiL technology allowing the company to create silicone rubber sheets suitable for the mass production of leather products. The fabric’s surface can be embossed to create the structure and feel of various types of leather. The pigmentation is adjusted to clients’ demands with eco-friendly pigments. Hot glue adhesions and roll-to-roll processing of large quantities of this silicone leather is possible thanks to unique and patented Compo-SiL technology.
Fashion brands and leather goods manufacturers can contact the sales team of General Silicones at compo-sil@gsweb.com.tw for more information on the prototypes, or visit www.compo-sil.com.
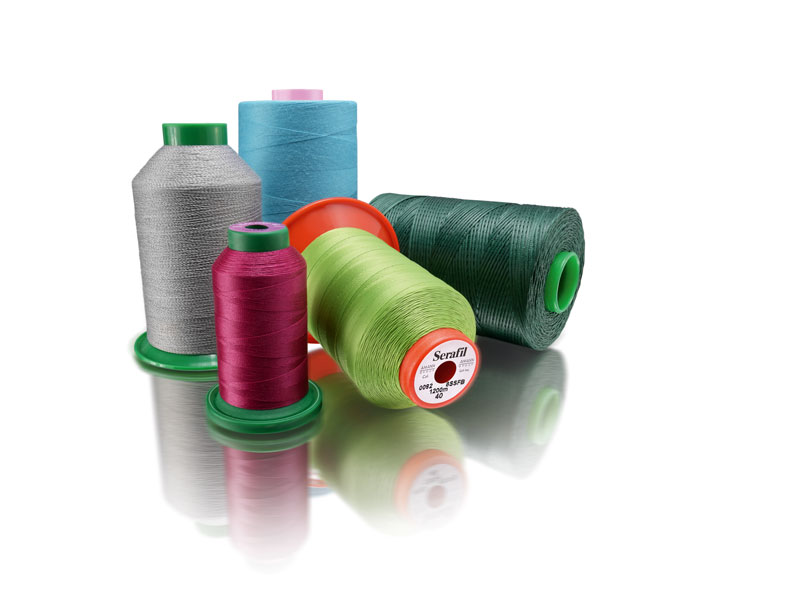
Amann Group is a manufacturer of sewing and embroidery threads, and smart yarns. Image courtesy of Amann Group
By Michael Strittmatter
Digitalization has been on the rise in the textile industry for quite some time, but throughout the recent COVID-19 pandemic, it has taken off at an accelerated pace, especially as the industry continues adapting to non-traditional remote work environments. Because of this shift to digitalization in the industry, more and more textile and apparel companies are starting to embrace the efficiencies of a fully digital color management workflow, which can offer a myriad of benefits.
Take, for instance, the yarn and thread experts from Amann Group, an international manufacturer of high-quality sewing threads, embroidery threads and Smart Yarns. They are a prime example of a company that has benefited tremendously from adopting comprehensive digital color management solutions throughout its entire global structure.
Why Digital?
Yarn quality and consistency is a top priority at Amann. This includes getting color right, every time — when product colors are inconsistent, consumers will view a brand as inferior or cheap. Because quality is so crucial to Amann’s business and their customers, they decided to standardize all of their production locations to guarantee consistent color globally.
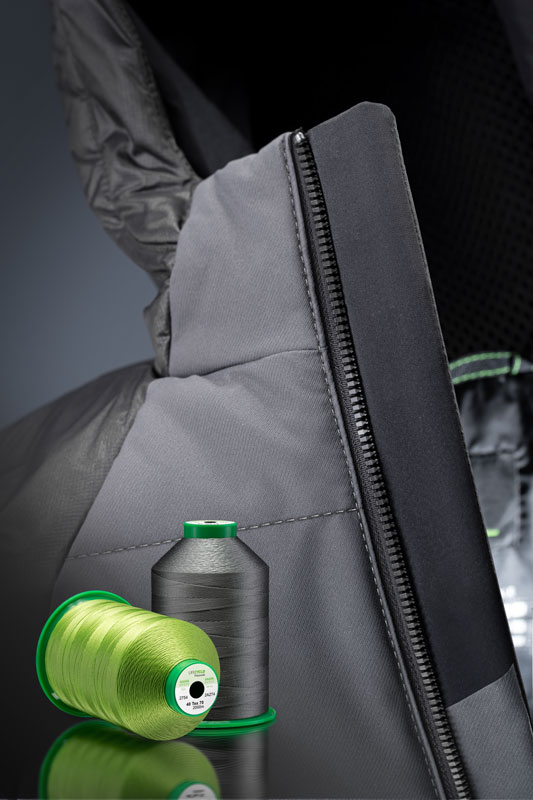
Image courtesy of Amann Group
Achieving consistent color across multiple components of one garment that has different components — such as the zippers, buttons, trims and snaps of a jacket or the lace, mesh, sole and body of an athletic shoe — is challenging. Quality control can be especially difficult when products have different coatings and gloss levels. Additionally, a single garment can contain multiple types of yarns stitched close together, which means a lot can go wrong if color is not controlled properly.
This is why a uniform digital color management approach across the supply chain is crucial to ensuring quality and customer satisfaction. By implementing digital color management solutions, textile and apparel companies can have confidence that colors will be accurate and repeatable.
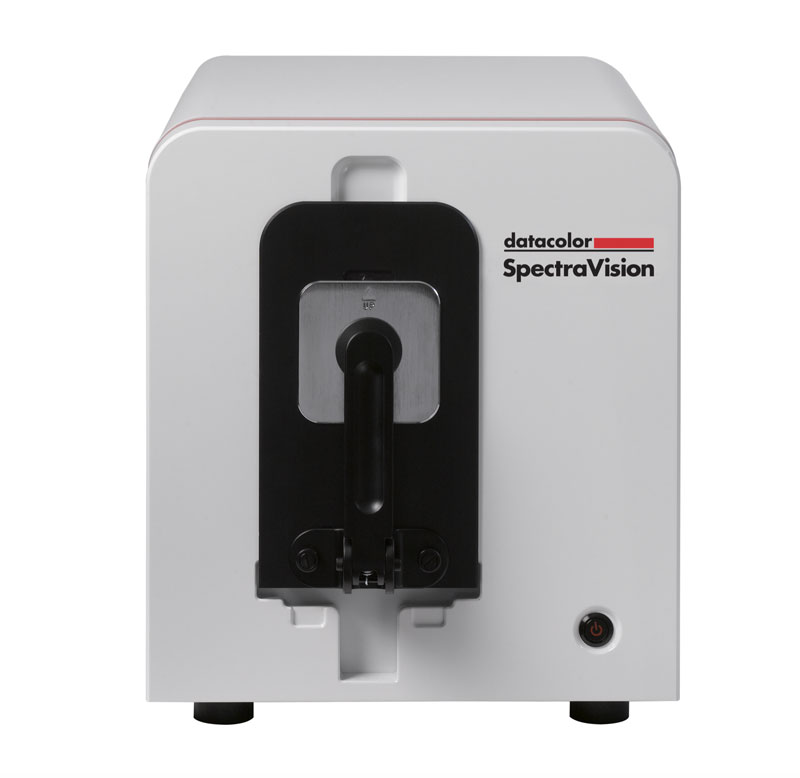
Image courtesy of Datacolor
Controlling Color from Start to Finish
At Amann and other textile companies that implement digital color management throughout the entire supply chain, the process starts at the very beginning with raw materials. Different substrates have different colors and whiteness levels, so it is important to include whiteness tolerances in supplier specifications before dyeing begins.
After a batch is dyed, a sample is prepared to remove temperature and humidity variation. Then, it goes through both visual and digital assessments to ensure the color meets expectations. Adding a digital component to this step is key, as relying on visual evaluations alone can be problematic, leading to potential delays and costly errors. We all see colors differently, so someone may see a perfect match where another sees variation. Digital measurements, combined with visual evaluations, removes the typical subjectivity associated with dyeing (and re-dyeing), resulting in a faster color match.
Amann has finishing machines installed in all dye houses to simulate the process. When the approval process can be done immediately after dyeing, companies can quickly determine if a batch is within specifications or has to be reworked, improving speed and efficiency even further.
A final visual and digital color evaluation check happens before a product leaves Amann’s production site, providing an extra layer of confidence that the customers will receive the highest quality possible.
Amann dye houses span across the globe, from Romania to Germany to China, and they all dye on the same material, so the results must be identical. Amann utilizes virtual samples across the global supply chain, so each dye house can access centralized data for quality checks. With digital color data, recipes can be exchanged among different facilities with a guarantee that results will be identical since every location has access to the same data. We have seen Amann successfully meet important quality requirements by leveraging a full suite of digital color management solutions every step of the way.
Post-Production Best Practices
Even after a product leaves a company’s production site, there are still steps companies must take to ensure quality and consistency down the road. Part of a fully digital workflow includes instrument monitoring to compare measurement values of all devices across all locations, as well as regular maintenance. Amann has seen first-hand how important it is to receive ongoing maintenance and support, to ensure that every device across the supply chain is within the same tolerance range and that the entire digital process is running smoothly.
Image courtesy of Datacolor
Looking Ahead At The Latest Advancements
Textile and apparel companies have come a long way in implementing a fully digital approach to color management. However, there is still room to grow and digitize even further as technology continues to advance. Amann has plans to start using data from previous production lots to increase accuracy of future batches.
As sustainability continues to be a priority in the textile and apparel industry, we expect to see other companies embrace sophisticated digital color management solutions to not only increase efficiencies, but to also decrease the amount of waste they are producing from dyes, water and chemicals. In fact, technology now allows development of an entire season digitally without a single physical sample. Reducing physical samples can help companies drastically minimize environmental impact and with digital color management solutions, they can be eliminated completely.
Digital color management is the future. A fully digitalized workflow offers extensive benefits to textile companies. Thanks to their fully digital workflow, Amann has been able to reach their goal of deciding during the color development process whether the batch is within specifications or needs to be reworked, saving time and money. From speeding up color development and improving quality control to cutting costs and increasing sustainability, a digitized color management system can truly streamline the entire process.
Editor’s Note: Michael Strittmatter is a sales Manager at Datacolor, Lawrenceville, N.J.
SCHMALLENBERG, Germany — June 14, 2021 — Quality, craftsmanship and innovation have always been FALKE’s core maxims. FALKE products are available in the best department stores and specialized trade shops worldwide. After strong growth in the digital business in Europe, the next step is to enter the US market with the full product range online. Socks and tights engineered in Germany and produced in FALKE factories in Europe are shipped directly from the central warehouse in Schmallenberg, Sauerland. Deliveries are initially made to the six populous states of California, Texas, New York, Florida, Illinois and Pennsylvania.
The range includes legwear for men, women and children, as well as a wide selection of functional sports socks. Highlights include the FALKE Luxury Line socks made of particularly high-quality materials, such as cashmere, baby camel and silk. FALKE products are characterized by materials of the highest quality, which are carefully processed in the individual production steps. Timeless, modern products for everyday life and special moments are created. Characteristics are the excellent fit and the outstanding choice of materials.
Founded in 1895, FALKE can look back on a varied and eventful company history. FALKE is run as a family business in the fourth generation and has developed into an internationally active family business. Our expertise in high-quality legwear and fashion is recognized worldwide. It is the result of a long process that led from handicraft tradition, through the special skills of a manufactory, to industrial production. The idea was and still is – to offer uniqueness in series.
This idea is based on a solid foundation of values: unconditional quality, highest craftsmanship and constant innovation accompanied by filigree specialization, creative design and last but not least continuity and absolute reliability.
FALKE Ergonomic Sport System
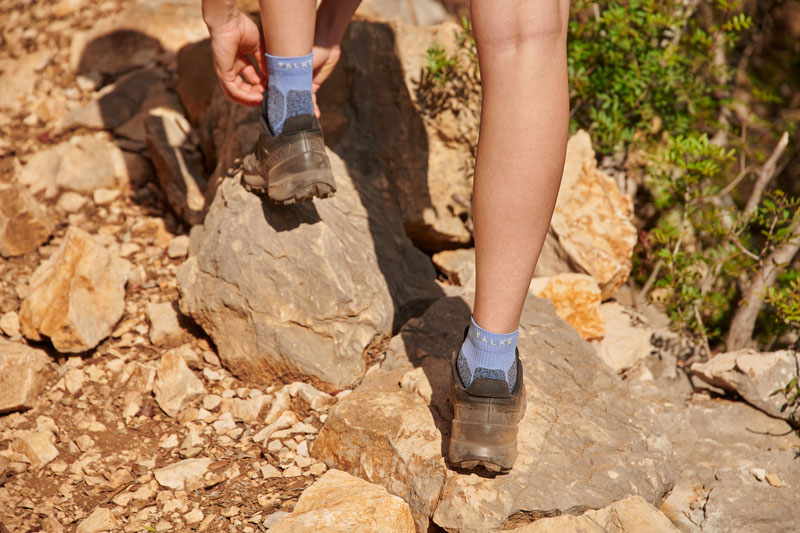
The FALKE Ergonomic Sport System is a concept with the purpose of optimally supporting every athlete and achieving their individual goals. Ergonomic products in sports adapt to body shapes, facilitate movement sequences and create optimal climatic conditions on the body. They also protect during prolonged practice of a sport and prevent injuries. The systematic combination of function, comfort, innovation and design characterizes the unique FALKE products.
The focus is on running, hiking, biking and skiing with a wide range of functional socks and underwear.
RESEARCH TRIANGLE PARK, N.C. — June 14, 2021 — AATCC is happy to announce the winners of the 2021 Pitch It to Win It Student Competition.
The Herman and Myrtle Goldstein Undergraduate Student Competition is intended to highlight projects conducted by students from all areas of the textile/apparel supply chain. Projects submitted may include academic research, technology and/or process investigations, and literature reviews. This competition is designed to enhance the textile education experience for student members of AATCC. The intent is to encourage independent student projects both within the USA and internationally.
First Place ($1,000 prize): Sophia Luu
Project: Optimizing 3D Fashion Design Software for Physically Disabled Populations
Major: Apparel, Merchandising, and Design: Creative and Technical Design
School: Iowa State University
Luu said: “The Pitch It to Win It competition has helped me learn how to communicate very discipline-specific research endeavors into accessible presentations that anyone can understand and glean significance from. Additionally, this competition has further broadened my understanding of 3D fashion CAD systems and aspects that can be improved for inclusive apparel design purposes.”
Trippiedi said, “Participating in the AATCC Pitch It to Win It competition gave me the freedom to ignite my passions and challenged me to explore the limits of endless possibilities.”
Major: Fashion Merchandising & Apparel Product Development
McKee said: “This competition taught me to be thorough in my work and to always back up my claims. As the process went on, I learned more and more about sustainability, humbling me on the amount of information I thought I already knew.”
JÖNKÖPING, Sweden — June 14, 2021 — Coloreel, with its unique patented technology for digital dyeing of textile thread on-demand, is entering the next phase in the efforts to scale up the company globally. Sven Öquist, with a background from Polestar, has recently been recruited as the new vice president of Sales.
Coloreel, a Sweden-based textile innovation brand, has developed a pioneering technology that enables high-quality digital dyeing of textile thread on-demand, creating sustainable and vivid fashion details. Coloreel began efforts to scale up the global presence last year, targeting a market valued over 25 billion Swedish Krona ($3 billion).
At the beginning of 2021, it was clear that Robur Ny Teknik would invest 100 million Swedish Krona (12 million) to support Coloreel’s market expansion and future growth. As a result, recruitment has been done to strengthen the sales organization with a new vice president of sales. Öquist, who previously was responsible for driving the sales expansion at Polestar, has recently taken on the role.
Mattias Nordin, CEO Coloreel, commented: “We are now seeing how the markets are starting to reopen after a period that has been marked by the effects of the pandemic. We operate in the textile and fashion industry and notice clear signs from our customers that production is picking up to a more normal pace again, not least when leading fashion fairs plan to be carried out according to plan during the late summer. This means that we are now scaling up to reach the global market with our innovative product. We have already come a long way, but the time is now right to increase our efforts as our goal is to reach a billion SEK in turnover within five years. Sven Öquist is perfect for the role of Vice President Sales with his previous experience of driving up sales volumes and developing sales organizations both in Sweden and internationally.”
Öquist commented: “Getting the opportunity to enter such a news-thirsty market is very exciting. Coloreel’s product will fundamentally change the industry. My job now will be to build on, strengthen and develop the sales organization with the goal of scaling up the company. The product has a unique patent foundation that gives me the opportunity to do this in the right way. To be able to participate and work with such an innovation, which has an enormous ‘tech height’ and development potential, is extremely motivating for me. The fact that it also provides significant sustainability benefits makes me extra proud to take on my new role.”
More and more customers are also paying attention to sustainability when it comes to fashion and clothing. But garments are more than fabric — after all, there are also yarns, fibers and applications such as zippers. All the better if they are also made from the same biobased solutions: from biobased VESTAMID® Terra.
“The zipper is a rather complicated product,” said Gabriele Mosso, suspecting that his comments will probably surprise some people. This everyday object, that’s so familiar to us all, which we have relied upon for so long to close jackets, bags or bed linen — undoubtedly an ingenious concept, but: complicated, really?
“It’s a fascinating object,” Mosso affirmed. As head of the Italy-based zipper manufacturer Nyguard for 15 years, he calls himself a “zipper maniac” with a wink and knows what he’s talking about. For a zipper to function smoothly a lot of detailed work is required, the right material, the exact shape. The teeth must mesh smoothly, must not get stuck, must not falter. And the fastener must literally integrate seamlessly into the tape. The idea for the zipper was born 125 years ago, at that time using sliding metal clasps. But the first versions all failed because they were cumbersome or quickly snagged. “In recent decades not much has changed about the basic idea for zips,” Mosso said. But the details have. Today, the clasp is mostly made of plastic and the strap is also synthetic.
Circulation Is The Target
This is where material development meets sustainability. More and more consumers feel a lot more comfortable when they feel that their consumption is not contributing to growing mountains of waste. So what could sustainable fashion look like? Recycling garments would be one variant: “Recycling materials is generally difficult when different materials are firmly bonded together,” Mosso said. That’s as true for composite packaging as it is in this case for pants with zippers. Different types of synthetic textiles and accessories are difficult to properly separate.
The same applies for certificates of origin for these various individual parts. The apparel industry is well-known for sourcing numerous components from completely different countries and production locations — from yarn, to buttons and zippers. “The latest challenge in textile is to achieve a complete traceability and circularity in value-chain. A process in which all the synthetic textiles and accessories could be recycled together” said Alan Garosi, head of Marketing at Fulgar, the Italy-based manufacturer from which Nyguard obtains the yarn for its zipper tapes.
Aware of that, Mosso added: “Why not make the zipper out of the same material as the tape it’s attached to? From plastic, sure, but why not from a more sustainable, biobased plastic. And even better: from a material that would also be suitable for use to make the complete garment?” This would at least bring us a decisive step closer to the possibility of recycling clothing. Even if there is still a long way to go before this vision is realized, because some details of clothing recycling still have to be invented — the prerequisites on the part of the manufacturers would be created.
It is precisely for orders like these, for outdoor and luxury clothing, that Fulgar also sees the close cooperation with Nyguard’s zipper manufacturers as a real benefit: “After all, we also have to think about the end of life of our products,” Garosi said. “If it becomes easier to recycle a garment, then that’s a meaningful thing for all sides.” That, in turn, pays into the larger issue of sustainability.
“A few years ago, companies were interested in sustainable zippers but not yet willing to pay for them,” Mosso added — an experience that matches that of Fulgar. But now, that has changed, and in 2020 in particular, demand has increased significantly. For Mosso, this is proof that his decision to fully focus on biobased plastics was the right one.
In the meantime, he is increasingly approaching customers with custom-made model designs of combinations of zipper and yarn, both of which are made using VESTAMID Terra. “We’re sort of doubling our sales strength there,” Mosso said. “It’s true co-marketing. And it’s highly successful because it hits just the right nerve.” Especially since, to his knowledge, he remains the only supplier currently offering zippers made from biobased materials. “That’s because we were early adopters of it, and our production process is already very well set up for it.” He winks. The zipper — that is, after all, a thoroughly complicated product in some details.
Create A Targeted Niche
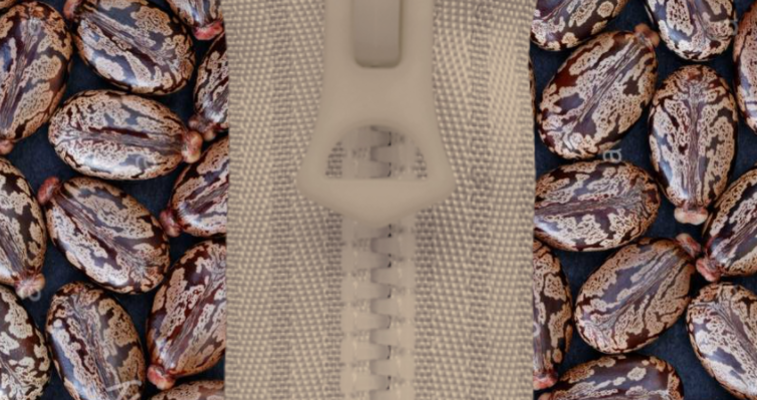
After some market research, Gabriele Mosso found what he was looking for at Evonik. The specialty chemical company’s VESTAMID Terra is a nylon made entirely from biobased material, castor oil to be precise. This is a raw material that is inedible for many animals so is not used as a food source, or as animal feed. Additionally, since the plant known as the “miracle tree,” tolerates dry soils and drought, cultivation of the renewable raw material does not compete with land used to grow food. This makes it an ideal plant for use in biobased solutions. At Nyguard, the decision was made about four years ago to move consistently in this direction. “We can’t compete with really big companies anyway — so we purposefully created a niche for ourselves,” Mosso said. Nyguard still occasionally produces zippers from plastic that is not biobased: “But the proportion of renewable raw materials is moving strongly toward 100 percent.”
Cooperation With Yarn Producer Fulgar
Another special idea of Mosso’s, also contributes to this successful conversion: He has sought cooperation with textile manufacturers in order to help convince his customers of using only products that are made of just one material. In this case, with Fulgar.
“The plastic from Evonik was an extremely good match for the polyamide we had been using,” Alan Garosi said. That’s because spinning a yarn from plastic requires detailed knowledge and expert experience. “Especially for high-quality textiles, plastic yarns need a high level of quality and purity,” he adds. Fulgar entered into a close exchange with Evonik, and both sides learned from each other as he describes: ”After a whole series of trials, we had found the formulation that worked best for us.” As a marketing executive with twelve years of experience at Fulgar and a long-term commitment to sustainability in textiles, he adds, “I’m watching the market and noticing a significant shift toward sustainability in the fashion and apparel industry in recent years.”
Textiles Made Using Bio-Based Fibers: Is It Possible?
Initially, it was just a curious interest from Fulgar’s customers: Textiles made from biobased solutions — would such a thing be possible and what would it look like? “But for about three years now, the topic has been picking up enormously,” Garosi noted. This is especially the case in the premium segment. Fulgar produces 36 million kilos of yarn per year, and here it has made a name for itself in the high-tech yarn sector, as well as with sustainable materials — even if these still make up a comparatively small share. The yarn that Fulgar produces from VESTAMID Terra is marketed under the brand name “EVO® by Fulgar”, an elegant, artistic nod to Evonik.
“Fulgar was the first company to recognize the opportunities for textiles made from VESTAMID Terra,” said Johannes Krampe, manager, Filaments, at Evonik’s High Performance Polymers business line. Evonik, in turn, was the first company on the market to think more broadly about the possible areas of application for a biobased plastic such as VESTAMID Terra: “We are really noticing how much the sustainability topic is now present in the industry,” Krampe said. More and more companies are responding to this desire on the part of their customers “not to be part of the throwaway society,” as Krampe puts it.
Plant Products From The Factory
“Particularly among customers, the term polyamide is still anchored in their minds as something artificial,” Garosi noted. After all, the term “plastic” already expresses that. “For many, it’s not very easy to understand that something made in a factory is actually a thoroughly plant-based thing.” In this regard, Fulgar was particularly excited about the fact that VESTAMID Terra is a 100 percent biobased material — and that its cultivation is not in competition with food production. “Many other fibers are made from sugar cane or similar materials that do place demands on the land. That’s one of the really central strengths and advantages of VESTAMID Terra,” Garosi said.
But for a yarn producer, VESTAMID Terra offers even more advantages. “The synthetic fiber is also extremely good in moisture management and also in coverage,” Garosi elaborates. With a comparatively lightweight fabric made from it, the wearer feels better protected from the wind and cold. In addition, moisture evaporates better with VESTAMID Terra than with comparable petrochemical-based nylons. This makes VESTAMID Terra an interesting alternative for sports and outdoor clothing, among other things, as well as for underwear. “But we also now have enquiries from producers of evening wear and luxury fashion,” Garosi said. In this segment, Fulgar is also well connected due to its high-quality production. Two years ago, Fulgar even supplied its EVO yarn to a shoe manufacturer.
MIGDAL HAEMK, Israel — June 15, 2021 — NILIT has announced that the company will sponsor a pioneering German-Israeli partnership to advance textile circularity. The initiative will officially launch with the Circular Textiles Business Matchmaking Showroom, organized by Re-Fresh Global, opening on 17 June at Expo Tel Aviv. The showroom kicks off a year-long exchange program between German and Israeli experts in sustainability, circularity, and textile waste management. The project is supported by the German[1]Israeli Future Forum Foundation.
“This innovative partnership aligns perfectly with NILIT’s goal to positively influence the textile and apparel industry to use more sustainable products in more responsible ways,” said Ilan Melamed, NILIT general manager. “NILIT has been recognized for improving our manufacturing footprint by increasing our use of clean energy, reducing emissions and waste, and introducing responsible new products that target specific ecological challenges. We look forward to connecting with other sustainability-minded companies to further advance our environmental initiatives.”
“Israel’s image as the Startup Nation has been key to creating tremendous impact on various industries,” said Viktoria Kanar for Re-Fresh. “It’s about time to show our excellence in sustainability and circular economy innovation. This showroom, and the German-Israeli expert exchange program it’s based on, is a first step toward developing new solutions and technologies that will create a new cleaner and circular global fashion and textile industry to benefit all humankind and the environment.”
Under its Total Product Sustainability program, NILIT manufactures the largest portfolio of sustainable premium nylon 6,6 performance and fashion fibers and yarns in the industry. The company recently launched several new products in its Sensil® consumer brand portfolio that are specifically targeted to the industry’s most pressing environmental challenges. Sensil®WaterCare eliminates 100-percent of the water used in the typical wet dyeing process and Sensil® BioCare contains technology that reduces any impact on oceans caused by microfiber shedding.
“The breakthrough ideas in sustainability and circularity require collaboration across the entire textile value chain,” continued Melamed. “At NILIT, we leverage the creativity of our employees and our vendor and customer partnerships. We are confident that this special German-Israeli exchange program will further expand our scope and help achieve dramatic improvements in our industry’s environmental footprint.”
NEW YORK — June 15, 2021 — Ralph Lauren Corp. today announced its goal to achieve net zero global greenhouse gas (GHG) emissions from its operations and its value chain by 2040. The company also published a detailed Net Zero Commitment Statement, its strategy for achieving net zero and advancing established sustainability targets. This new strategy builds on the company’s existing GHG reduction commitment to lower absolute GHG emissions across its operations and supply chain by 30 percent by 2030 compared to Fiscal 2020 levels. It includes scaling investments in credible, nature-based carbon removals, starting with an initial partnership with Indigo Ag, the first scalable, registry-approved carbon credits for agriculture.
“Climate change is one of the most complex and challenging issues of our time — one that will require innovation, collaboration, technology and a fundamental shift in behavior to solve,” said Patrice Louvet, president and CEO, Ralph Lauren Corp. “Our net zero goal and roadmap are anchored in our belief that through deliberate action we can deliver the change required to reduce our climate impact and help create a more sustainable future for generations to come.”
The Company’s net zero approach entails reducing scope 1 and 2 emissions by using 100% renewable power in its stores, offices and distribution centers by 2025. To reduce emissions from scope 3 sources resulting from making its products, Ralph Lauren will collaborate with suppliers through collective actions and strategic programs to drive down GHG emissions in manufacturing facilities. Moreover, it plans to reduce GHG emissions from its raw materials by switching to preferred fibers with lower emissions impact than conventionally-grown fibers.
In the coming years, Ralph Lauren expects to expand its emissions reduction tactics to include collaboration with suppliers through collective action programs that accelerate the standardized approach to setting carbon targets and low-carbon action plans at the factory level, further empowering those partners to establish and implement climate strategies aligned with Ralph Lauren’s net zero objectives. Ralph Lauren’s net zero plan extends beyond reducing GHG emissions from its operations and suppliers in its value chain. For emissions that cannot be reduced through Ralph Lauren’s direct actions and collective initiatives, the company will purchase high-quality, verifiable carbon removals equivalent to its residual GHG emissions by 2040. To that end, beginning in Fiscal 2022, Ralph Lauren will commit to carbon removal projects in partnership with Indigo Ag, an ag-tech company dedicated to improving the profitability, sustainability and social responsibility of the agriculture system. Through the Indigo Carbon program, Indigo Ag supports farmers in adopting new beneficial farming practices; measures and validates the resulting carbon sequestration and emissions abatement; and allows companies to directly support farmers’ transition through the purchase of verified agricultural carbon credits.
Aligned with its commitment to the climate goals identified in the Paris Agreement, Ralph Lauren’s new net zero pledge is its latest significant move to aid in mitigating the impact caused by its global operations and a key component of Design the Change, the company’s Global Citizenship & Sustainability strategy. The company’s net zero progress will be reported yearly in its annual Global Citizenship & Sustainability Report, a fully detailed corporate environmental and social status update on its sustainability approach.
EBENE, Mauritius — May 15, 2021 — One hundred percent digital, CIEL Textile is pleased to present its first sustainability report developed in accordance with GRI standards. The report entitled “Winning Well” provides a transparent overview of the current state of the Group’s sustainability achievements and progress. It demonstrates CIEL Textile’s objective to be a “Sustainable Global Fashion Partner” for leading international fashion brands.
Eric Dorchies
“After a year marked by the COVID-19 pandemic, the publication of this report demonstrates our commitment to sustainable development, which is at the heart of our corporate strategy and vision” said Eric Dorchies, CEO of CIEL Textile.
“We are merely in the starting blocks, yet we are determined to contribute at our level to this global issue, by accelerating our efforts in terms of Sustainable Fashion, by working together with our customers and partners to be more respectful towards our planet and our communities. The stakes are high, whether in terms of reducing our carbon emissions, improving working conditions or product traceability, but we are convinced that this is the only way forward for the future of our Group”, adds Pami Kular, Head of Sustainability for CIEL Textile.
Pami Kular
The report covers the period July 2017 to June 2020 and shares the data for the environmental, social and corporate governance (ESG) of CIEL Textile operations which includes 18 production sites and nearly 18 000 employees. The report introduces the group’s approach and actions implemented to improve its ESG performance.
Activate climate response
Commitments:
Zero Coal as boiler fuel by 2030
Achieve 35% renewable energy by 2030
50% reduction in waste to landfill by 2030
Under this section, it is worth noting that:
CIEL Textile joined the Sustainable Apparel Coalition (SAC) in 2017, becoming the first Sub-Saharan African member of this global alliance.
In 2019, Aquarelle’s factory in Samudra, India, was awarded the LEED Platinum Certification—the highest distinction for green buildings—making it one of the first apparel eco-factories in India.
Around 50,000 trees were planted in 2019 as part of carbon offsetting activities.
100% of the effluents are treated before discharge using effluent treatment plants (ETP).
Foster a vibrant workforce
Commitments:
35% Women at Management level by 2030
100% employees trained on Ethics and Sustainability by 2023
Under this scope, CIEL Textile indicates that:
98% of the workers are permanently employed.
Regular audits of all production sites are carried in accordance with the IFC performance Standards for human rights.
Through its Leadership and Management Academy 361°, CIEL Textile trained 2,500 employees in best practices for operational excellence and managements techniques.
Champion inclusive growth
Commitments:
·Advocate for 30% Certified & Recycled raw material usage by 2025 & 50% by 2030
Advocate for Higg Index tools adoption in our value chain representing 80% of business volume, of which 50% verified by 2030
Under this heading, it is interesting to note that:
91% of the product mix is made out of 100% natural raw materials
18,000 employees spanned in 4 countries participated in the annual group initiative “Act For Our Community” and voluntarily devoted their time to support community driven events.
CIEL Textile provided rigorous control and monitoring over its 1 150 suppliers and partners
CIEL Textile has taken initial steps to develop circular economy solutions, having created a 100% recycled shirt, as well as a 100% “waste-to-wear” sweater
“Save the date for the release of our 2nd report in 2023 which, we hope, will show many positive advances in all our initiatives” said Pami Kular.
“I firmly believe that our future lies in our ability to transform our industry through smart design, innovation and sustainable supply chains while offering products at competitive prices,” concluded Eric Dorchies.
Read the full report and discover the group’s performance and sustainable development initiatives online on: https://www.cieltextile.com/sustainability-report-2020.pdf
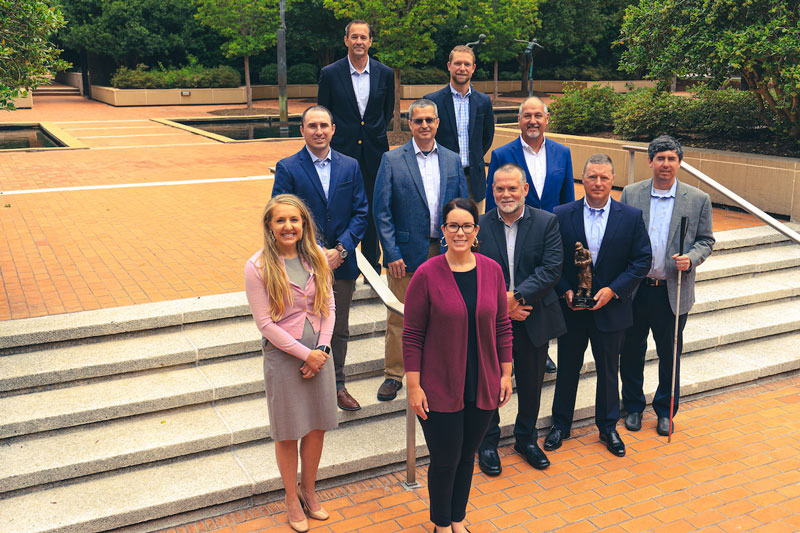
Front row (left to right): Meg Patel, marketing manager, Government and Defense, Milliken; Nicole Ducouer, senior director communications, IFB; David Horton, president and CEO, IFB; Erik Cobham, director Business Development, Government and Defense, Milliken; and Danny Kelly, executive vice president, IFB. Middle row (left to right): Sean Murphy, Senior Account Manager, Government and Defense, Milliken; Silas Martin, COO, IFB; and Randy Buckner, vice president, Asheville Manufacturing, IFB. Back row (left to right): Bruce LaFlam, vice president, sales and marketing, Government and Defense, Milliken; and Matt Gilreath, CFO, Textile Division, Milliken
SPARTANBURG, S.C. — June 15, 2021 — Milliken & Company has been named Partner of the Year by IFB Solutions. In its 15th year, the prestigious award is given to the partner who has stood out as an organization that has gone beyond the board room to support opportunities for people who are blind. Milliken was selected from more than 400 IFB vendors.
“It’s an honor to receive an award of this caliber from a partner like IFB,” said Chad McAllister, executive vice president of Milliken & Company and president of the Textile Division. “IFB has shined a light on how to do business for good, going above and beyond to positively impact their community. We are honored to call them a partner and look forward to continuing to support their mission for years to come,” he adds.
Milliken has been working with IFB, a US-based manufacturer who provides employment to people who are blind or visually impaired, since 2008 as a U.S. military fabric supplier. Since then, the partnership has provided more than 245,000 hours of work for people who are blind or visually impaired. In addition to the business relationship, Milliken has donated more than $30,000 to IFB over the years to support jobs, training and services for the blind.
“All of us at IFB Solutions are incredibly grateful to the Milliken & Company team for their contributions to our mission. As a non-profit, our mission is to provide opportunities for people who are blind or visually impaired in need of training, employment and services. For more than a decade, our partnership with Milliken has provided countless opportunities for adults and children who are blind all over the country resulting in thousands of lives changed for the better,” said David Horton, president and CEO of IFB Solutions.