When brands talk about sustainability, they often cite that the primary objective is to “raise awareness”. By “raising awareness” brands can better engage customers, communicate their initiatives and better promote their sustainable products and ethos. But now it’s time to evolve the conversation. To remain competitive and more importantly, achieve greater sustainability results, brands should look to evolve their messaging from awareness to action.
Actioning sustainability goals and objectives is the only way forward to achieve the results needed to be truly eco-friendly. Consumers today will prioritize fashion brands that embed sustainability into their operations, set realistic ambitions, and make positive change. Brands that create sporadic and ineffectual campaigns, which function as an extension of greenwashing, will be left behind.
Sustainability Has A Domino Effect
Change starts with the brands and manufacturers at the beginning of the textile supply chain, and when they take action, their efforts create a domino effect that cascades through the supply chain onto the customer. Efforts to reduce carbon emissions and curb the reliance on fossil fuels don’t go unnoticed by consumers. In fact, the emergence of the “conscious consumer” has provided brands with the ability to reconcile the need to meet business objectives while doing good for the environment. This is evidenced by changing consumer habits.
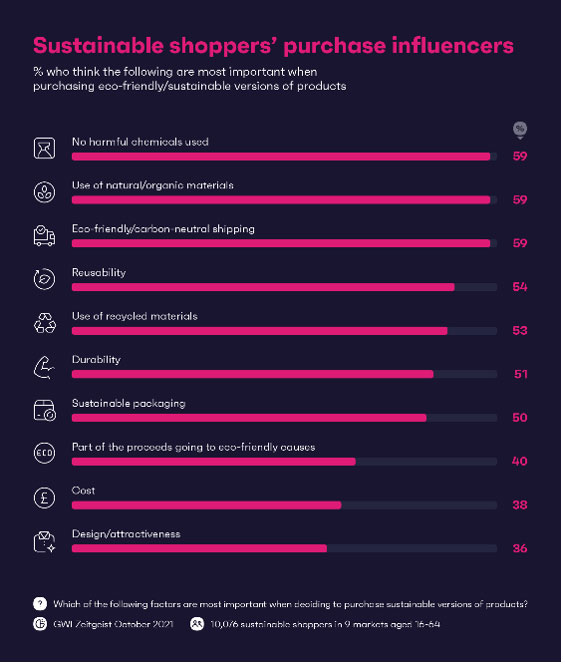
Source: GWI Zeitgeist October 2021
According to a survey conducted by Global Web Index, nearly two in three consumers who describe themselves as fashion-conscious would rather pay more for an eco-friendly product.* Sustainable shoppers are guided by a myriad of factors, but three factors are highlighted as the most important considerations when making a purchase decision — no harmful chemicals, use of natural/organic materials and eco-friendly/carbon-neutral shipping. The challenge for brands is how they justify an increased cost on their products as a result of catering to these factors. Only by being transparent about their manufacturing and communicating their sustainable value proposition to consumers can they differentiate. Consumers should be shown exactly how an increased cost for their garment, yields mutual benefits for their wardrobe and their planet.
Brands That Go Green, Make Green
Fast fashion is easy to produce, it provides an abundance of choice and can be made in mass quantities. Many brands often turn to man-made fibers like polyester to produce their garments. However, in order to really preserve our environment, the industry has a collective responsibility to adopt sustainability in all levels of the supply chain, from fiber, consumption, recycling and disposal.
To implement sustainability for brands, action is key. Half measures and reputational band-aids do little to alleviate the disastrous impact that fossil fuel reliant synthetic fibers have on both the environment and people[2]. Instead, brands and manufacturers must calibrate their revenue approach to include sustainable consumers with big pockets. They can do this by developing impactful campaigns, setting achievable sustainability goals and finding creative ways to involve their consumers beyond just selling clothing to them. This post-sale brand interaction and ongoing education to consumers is where sustainable brands can gain a competitive advantage and really perform in the market for the long run.
How We Do Campaigns: #MakeItFeelRight In Action
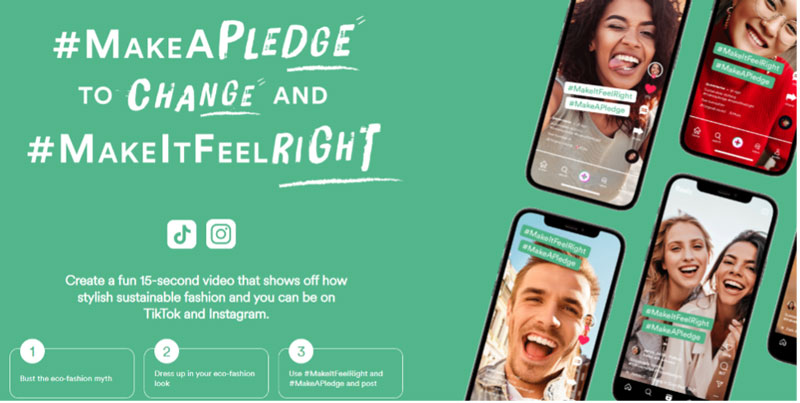
When Lenzing’s TENCEL™ brand’s #MakeItFeelRight campaign launched back in 2019, it did so with the firm objective to raise awareness around the negative environmental impacts caused by the fashion industry. Last year, the campaign sought to garner social media pledges from consumers who created fun and exciting posts that showed off their sustainable clothing. For the initiative, TENCEL™ partnered with One Tree Planted, an environmentally conscious NGO which planted a tree for every pledge generated.
Image courtesy of Lenzing
This effort to debunk the myth that sustainable fashion is not stylish generated more than 8,000 pledges, a huge contribution to global reforestation efforts.
Any brand that wants to uphold their sustainability commitment should inspire their supply chain partners to follow suit, transition awareness to real action and most importantly practice what they preach!
* GWI, Fashion for good: why sustainability is on trend https://blog.gwi.com/chart-of-the-week/sustainable-fashion/ ** Changing Markets Foundation: Fossil Fashion Report https://changingmarkets.org/portfolio/fossil-fashion/
Editor’s Note: Harold Weghorst is global vice president, Marketing & Branding, Austria-based Lenzing AG
By Mark Sollman, Product Manager EMEA, Mimaki Europe
With the all-important COP26 Climate Change Conference having taken center stage in November, there is no time like the present for the fashion world to rally together in stepping up sustainability efforts and getting carbon emissions under control. Globally, the fashion industry is now estimated to account for around 10 percent of greenhouse gas emissions and 20 percent of wastewater*, making the pursuit of greener production methods more pertinent than ever before. Thankfully, we are seeing a new era of production enter the fashion arena, with the increasing emergence of technologically advanced, highly automated microfactories.
Along with reducing unnecessary waste through on-demand production, microfactories have a smaller ecological footprint than traditional garment production and require no water use during the production process, making it not only a faster solution, but a greener one too.
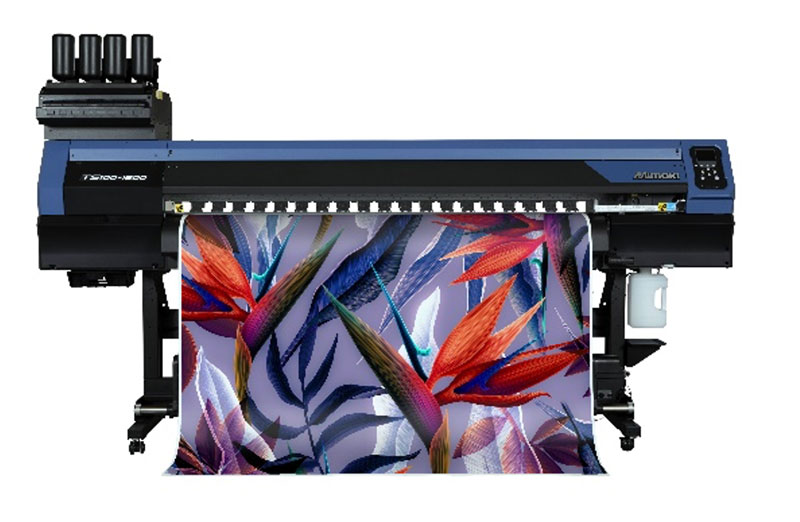
Last year’s FESPA saw Mimaki team up with fashion designer Carolina Guzman to bring her designs to life in real time at the show, setting up its own working microfactory live on-site to take her designs from screen to garment within just a day. Guzman’s designs were created using Mimaki’s TS100-1600 Sublimation Printer, before being transferred to textile, digitally cut and finally pieced together. Devised with a string of ethical and environmental objectives threaded throughout, the microfactory also exclusively utilised eco-friendly Greentex fabric, and any remaining material was donated to Sheltersuit: a wind- and waterproof coat that can be transformed into a sleeping bag, which is provided free of charge to homeless people and refugees.
Through working with a number of strategic partners — including transfer printing expert, Klieverik; paper solutions specialist, Neenah Coldenhove; and digital cutting equipment provider, Summa — Mimaki was able to produce a collection of unique, high-quality garments live on the stand during the tradeshow, demonstrating to visitors from more than 100 countries some of the key reasons that microfactories seem set to change the future of fashion…
Unparalleled speed and versatility
Where traditionally, apparel manufacturing has centered on a production chain model of sourcing materials and producing garments in bulk, microfactories are now enabling on-demand, on-location production, making it possible to create everything from unique, one-off pieces and samples right through to entire product lines – all at unprecedented speeds. This means greater flexibility and customization, enabling designers to modify or update designs and respond to market trends as they occur.
Simplified Supply Chains And Minimised Risk
The microfactory setup brings production in-house and on-demand, minimizing the cost of not only storing stock, but also of shipping it and responsibly disposing of unsold items. Where recent geopolitical events have highlighted the fragility of global supply chains, microfactories offer a unique independence from these systems, empowering garment manufacturers to future-proof their businesses, become less reliant on external systems and suppliers, and reduce the risk of disruptions.
A Boosted Bottom Line And A Greener Future
Facilitating savings in a whole line of resources, from physical storage and production space to time and energy, microfactories ultimately have the potential to significantly increase profitability for garment manufacturers, with the additional benefit of being easily scalable as production increases. Perhaps even more compelling, however, are the environmental considerations. Demonstrated on a small scale through Mimaki’s recent project, the environmental benefits inherent to microfactory production will have an even greater impact as it becomes more prolific and commonplace throughout the fashion world, with the potential to effect meaningful environmental change as adoption increases in the years to come. In short, watch this space!
Penn Textile Solutions Relies On Process Control From Mahlo
TW Special Report
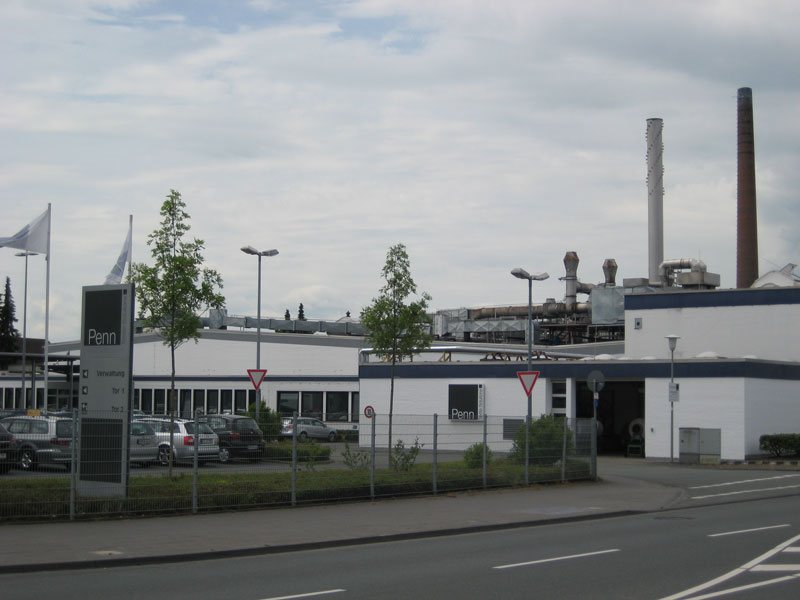
When you think of a textile production hotspot, Paderborn, Germany, may not be the first place that comes to mind. It should though! Because this is where Penn Textile Solutions GmbH has been based since 1959. The company is one of the world’s leading manufacturers of elastic fabrics for under-wear, corsetry, sportswear and swimwear, as well as highly functional textiles for technical applications. The fully integrated company with its own warping, circular knitting, warp knitting, dyeing and finishing facilities currently employs around 150 people.
“Over the past several years, one of the areas Penn has specialized in is the production of custom-fit, close-contour compression knits. These are increasingly being used in the sporting goods sector,” noted Operations Manager Franz Schütte. “Customers can expect a unique design with highly functional wearing comfort from our articles at the same time.” The production of these textiles requires the corresponding know-how as well as the appropriate production and process technology for the production of the surfaces as well as for the finishing and quality assurance. In order to continue to meet these high demands, Penn wanted to further optimize its tenter frame processes.
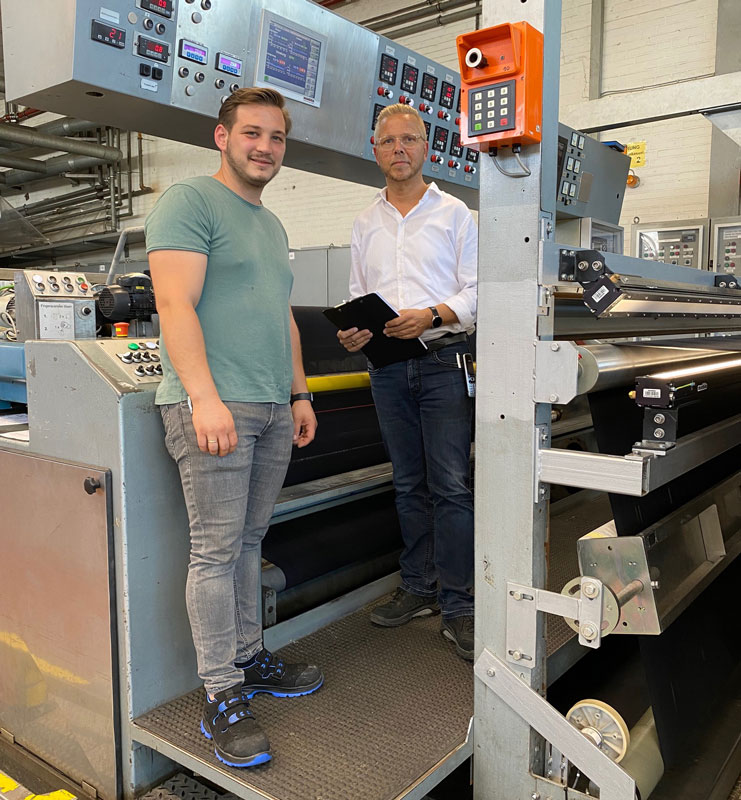
Tugsan Vural, deputy head of the equipment department (left) and plant manager Franz Schütte trust in Mahlo quality.
Many of the products are made from so-called compression knits, in which different constructions are integrated within one quality. Penn produces the compression knitted fabrics on special raschel looms. “The compression zones place accurately in the finished element. The balance of the agents plays an important role here.” In the subsequent finishing process, a textile surface with the required stretch behavior, the appropriate repeat lengths and basis weights should be created, particularly in the drying and fixing process. The measuring and control system in the tenter frame process must realize and guarantee these requirements over the entire length of the section. Not an easy task!
Penn Has Long Relied On Mahlo
To achieve its own high quality targets day after day, Penn has relied on the cooperation with Germany-based Mahlo GmbH + Co. KG, based in Bavaria, for years. The manufacturer of measuring, control and automation systems for web-shaped goods has decades of experience in the field of process control. “We have been using Mahlo systems for more than 30 years and have always been able to rely on excellent results,” says Schütte. Until the summer of 2020, the textile manufacturer had been using a basis weight measurement system in the tenter frame outlet with beta radiation and manual control. “When the krypton preparations had passed their half-life, we had to make a decision: Exchange or replace the system right away.”
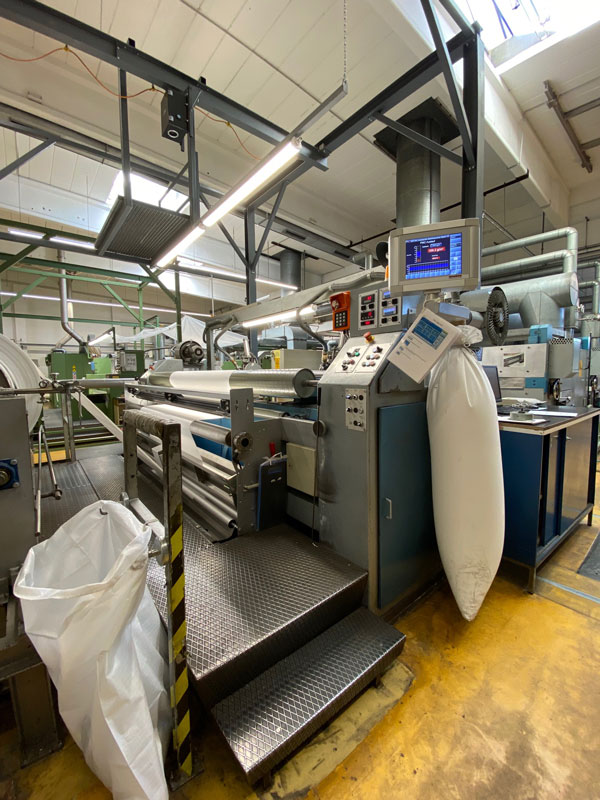
The Famacont PMC integrated in the production line
They sat down with Mahlo representatives and looked for the best solution. Since the systems had already reached a high operating age and the measurement was limited to the basis weight, a new concept was decided upon. “Mahlo made us the best price-performance offer.” The new system should be even more efficient and easier to operate for the special makes.
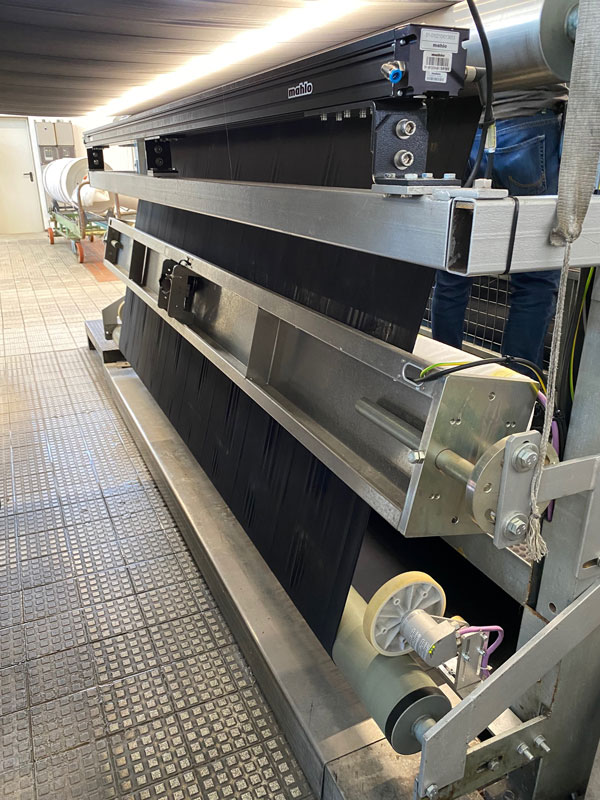
The compression zones of the functional fabric create corresponding distortions within the textile surface in its raw state, which have to be smoothed out in the fixing process. This work is now taken over by a process control system. The Mahlo Famacont PMC-15 with two measuring points automatically controls the leading of the stenter frame by continuously and contactlessly determining the mesh density. In addition, the Patcontrol PCS-20 process control system ensures that the dimensions of the different zones are recorded and also automatically controlled. “The previous beta-radiation facility was not able to collect this kind of data,” explained the Penn operations manager. Another important aspect for the textile manufacturer: the complete and costly radiation protection is no longer necessary with the new systems.
Thanks to the Patcontrol PCS process control system, the zone fabric is detected and also automatically controlled.
Despite very good experience with Mahlo in the past, every change naturally involves a risk. Penn did not have to rely on theoretical considerations, however, but carried out tests in advance with appropriate sample material in the Mahlo test laboratory. The results convinced the decision-makers. “In addition, appropriate internal considerations and external consultations provided us with the necessary certainty for the investment decision. The risk was therefore manageable,” Schütte said. The investment has already paid off. “The new measurement and control technology enables consistent compliance with our desired parameters.” Scrap in the form of manufacturing waste due to mismatched quality parameters has decreased by 5 percent. Due to the success of the production process, a further measuring station for thread density and basis weight was put into operation this summer.
Highly engineered woven narrow fabrics can be the substrate in critical consumer applications that require superior properties.
Selecting the textile construction method that ensures end item performance
ByTed Fetterman
Woven narrow fabrics can serve as structure or substrate for components in critical customer applications that require superior properties. End product designers and engineers should understand weaving technology and how it differs from other textile production so they can correctly select a textile construction method that ensures end item performance.
Weaving narrow fabrics — the basics
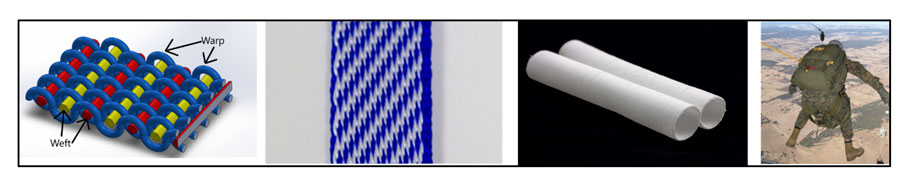
Weaving is a method of creating a structural textile by interlacing fibers and yarns in a way that maximizes specific fiber properties. Weaving yarns are interlaced in a perpendicular manner, with both longitudinal yarns (x-direction), and horizontal yarns (y-direction). Known respectively as warp and weft or filling yarns, they are oriented at 90 degrees to each other.
Weaving produces a stable construction in both the x and y directions. In fact, of all the available methods used to create textile material, weaving provides the most stable and versatile construct. Key properties include high strength, elongation, energy absorption, optimum strength to weight ratios, flexibility, and sewability.
Narrow fabrics are generally divided into two types: webbing and tape. Webbing, narrow fabrics 12 inches wide or less, refers to fabric with a longitudinal strength equal to or greater than 1000 pounds per inch of width. Tape refers to narrow fabrics with a longitudinal strength of less than 1000 pounds per inch of width.
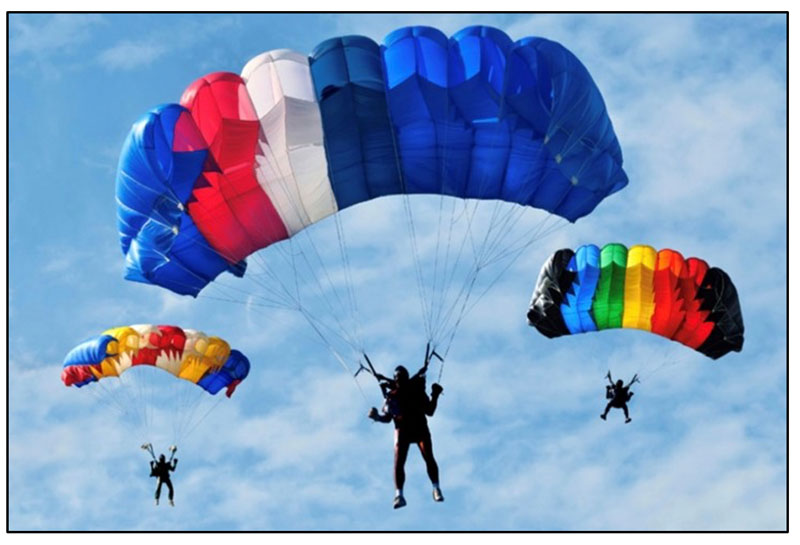
Both shuttle looms and needle looms are used to manufacture both structural webbing and tape. The needle loom is designed for speed and is the best option for large runs of production material. A shuttle loom enables more weave design versatility and provides structural, uniform, and woven edges that results in more even loading across the webbing’s width. This method is preferred for applications requiring maximum weave design flexibility. Flat woven, tubular material and 3-D fabrics can all be produced with perfect symmetry on both edges of the woven substrate. This provides uniform edge loading during, for example, high-speed deployment of parachutes.
Left to right: Plain weave, twill weave, tubular weave, and stuffer construction — a tubular weave to which a stuffer yarn and a binder yarn are added to a multilayer woven fabric to add strength.
Weave design options
Several weave designs are available to meet specific application requirements.
Plain weave is the simplest form of weaving. The filling/weft is inserted up and down every other warp yarn. Edge binding and reinforcement tapes utilize plain weave designs due to their need for high structural stability and minimum surface abrasion.
Twill weave involves passing the filling/weft yarn over or under two more warp yarns. It is generally softer and more pliable than a plain weave and has increased tensile and decreased elongation properties. Twill constructions are used to bind edges with complex curves and tight corners and for high strength applications that require maximum strength of the woven warp yarns.
Tubular weave joins two sets of warps yarns at the edges. When woven on a shuttle loom, the fabric created is completely seamless, resulting in a fabric with a uniform water porosity and air permeability property. Often designed into filtration and other medical device applications, tubular webbings are also utilized for their hoop strength in inflatable vessel constructions.
Stuffer yarn constructions are those with a tubular weave to which a stuffer yarn and a binder yarn is added to multilayer woven fabrics to add strength. One example is industrial belting applications that use woven thermoplastic fibers around aramid stuffer yarns used for its high tensile properties. The method is also used in parachute harness webbing to improve webbing strength and stiffness. The binder yarns act as woven sewing type stitches that help to stabilize the weave and lock in the jacket fibers with the stuffer yarns.
Many variables affect the success of a specific webbing. Questions to consider during the design process include:
What performance properties will be required in the final weave design?
What is the stiffness requirement? How should it feel when held?
What type of hardware will be required?
What termination method will be used?
Does the end-use application require specific consideration?
For composite applications, what are the specific properties of different fibers required?
Fiber Size And Strength
Weaving yarns are composed of bundles of individual filaments of a specified number. When these filaments have long continuous lengths, it gives the yarn optimum strength and tensile resistance.
All types of man-made fibers are specified for size. Comparisons are made among fibers by referring to their denier, which equals the mass in grams of 9000 meters of weaving yarn. For example, a 220 denier nylon is composed of a smaller bundle of continuous filament fibers and has less mass than a 440 denier nylon, so it is less strong. The strength to mass ratio is in direct proportion; for example, 440 denier nylon 6,6 has two times the strength as 220 denier nylon 6,6 from the same batch of fiber.
Fiber producers publish tenacity values that can be valuable for comparison purposes, but actual tensile strength yields of woven fabrics will be less than these published numbers. This is due to a concept known as translational strength, defined as a comparison of the properties of a fabric to that of the input base fiber. Due to many weaving process variables, translational tensile strength yields are typically 20-40 percent less than published fiber tensile strengths. It is critical to understand the many trade-offs needed to achieve performance characteristics and the relationship between variables and performance.
Fiber selection is an important aspect of woven fabric design
Fiber selection
Fiber selection is an important aspect of woven fabric design. Available options include natural fibers, standard man-made fibers, and high-performance advanced fibers.
Natural fibers: Cotton is the most typical natural fiber used in webbings, especially for packing material for mechanical bearings and flame wick applications. Preferred for next-to-skin contact, cotton is not used for most industrial applications.
It is difficult to produce structural cotton webbings using US cottons that meet United States Military Standard (MIL-SPEC) specifications for thickness, strength, and weight. However, the Berry Amendment requires that fibers be grown in the US for US DOD contracts. This can present challenges when using cotton webbing for technical applications and may require that end users consider nylon or polyester webbing as an alternative.
Man-made fibers: Man-made fibers include such standard options as nylon, polyester, polypropylene, and rayon. Nylon is used on many webbing applications because of its toughness, strength, durability, and dyeability. Nylon will elongate under load, which absorbs energy, making it a good choice for parachutes and PPE/fall protection applications. Nylon is also hygroscopic, meaning it absorbs moisture. While all fabrics will wick moisture, the nylon fiber itself will gain moisture content.
Polyester is another common standard manmade fiber used in webbing construction. With a strength similar to nylon, polyester has a lower elongation property, making it a good option for automotive and aircraft seatbelts. Polyester is hydrophobic, so it has minimal moisture regain and can be used for applications at or around fresh and salt water. Polyester is dyeable but must be dyed at a higher temperature and pressure than nylon.
High-performance fibers feature greater strength to weight ratios, high-temperature resistance, chemical resistance and minimized elongation.
High performance/advanced fibers: Advancements in polymer chemistries have given high tech fibers desirable inherent properties, for example, greater strength to weight ratios, high temperature resistance, chemical resistance, and minimized elongation properties. Key examples include aramids, UHMWPE (ultra-high molecular weight polyethylene), PPS (polyphenylene sulfide), and PBO (polybenzoxazole).
Webbing used in critical applications requiring superior properties
BRM designs, engineers, and manufactures woven materials that serve as structure or substrate for components in critical customer applications that require superior properties, including:
For example, polytetrafluoroethylene (PTFE) fiber chemistry makes fibers resistant to specific chemical exposure and gives them a natural lubricity. BRM uses this type of fiber on the webbing surface to impart a wear-surface.
One successful application is as a wear surface for structural components of highway bridges. The other fibers used in this proprietary construction are high strength aramid, which gives the fabric the strength needed to survive the tensile and compression forces on concrete and steel bridge structures from high-weight vehicle travel and thermal expansion and contraction.
Another example is PPS, used in industrial filtration and air cleaning, where high concentrations of sulfuric acid must be removed from effluent air from power plants and other industrial processes.
A final example is a woven composite belting/narrow fabric being utilized in a proprietary application as a drive/control belt in a machinery process. The customer pursued the use of DuPont™ Kevlar® aramid, whose high strength and low elongation seemed ideal. However, Kevlar tends to degrade from bending fatigue. To counteract this negative property, BRM added polypropylene fibers to the outer jacket of the woven material to provide some protection. The final item is heated to approximately 300 degrees F, at which point the polypropylene melts around and through the Kevlar fibers, completely encapsulating the aramid fiber and providing a wear surface and protection from flexural fatigue.
Understanding the art and science of weaving
Weaving is both an art and a science. Many variables affect the success of a specific webbing, irrespective of predictions based on bench top design. With its years of experience, BRM understands how to control many of these variables, but such knowledge does not necessarily always improve strength yields. That is why BRM always runs rigorous trials at the loom to test properties and understand the trade-offs that must be made to ensure fabric performance. Using a careful iterative process to create innovative new fabric prototypes, BRM designs solutions with fabrics that meet a wide range of property requirements for highly engineered applications. After all, we have material on the planet Mars!
Editor’s Note: Editor’s Note: Ted Fetterman is vice president, sales and marketing, Bally Ribbon Mills, Bally, Pa.
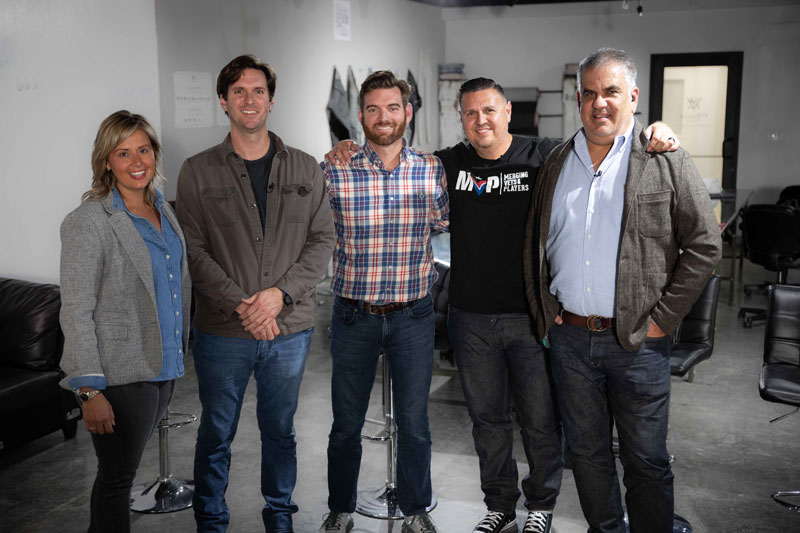
Jennifer Crumpler, Fiber Development manager with BASF is joined by Marshall and Mead Hardwick of Hardwick Planting Company, Trinidad Garcia III, founder of Trinidad3 and Eric Goldstein, executive vice president of Vidalia Mills.
TW Special Report
National fashion and textile editors recently took a break from their busy deadlines and embarked on a virtual trip called Farm to Fashion: an e3 Sustainable Cotton event. Led by BASF Fiber Development Manager Jennifer Crumpler, editors traveled on a sustainable cotton journey, beginning in the field and ending with jeans.
“The purpose of the e3 Farm to Fashion event is to bring together voices from all parts of the cotton supply chain,” said Crumpler. “We’re proud that our partners provide cotton and end products that are sustainable and made in the U.S.”
Traveling With Cotton: From Seed To Jean
Those partners included Louisiana cotton farmers Marshall and Mead Hardwick, who together with their parents, run Hardwick Planting Company. The family farms approximately 9,000 acres of cotton, corn, soybeans, wheat, and sorghum.
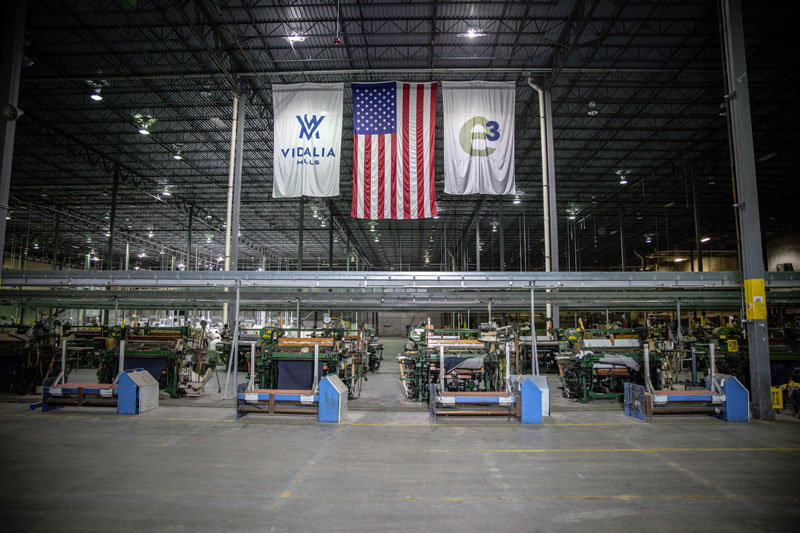
After hearing from the Hardwick’s about their operation in Newellton, LA, guests “traveled” a short distance to Vidalia, LA, where Eric Goldstein, executive vice president at Vidalia Mills, shared the story behind the mill. Because of their commitment to a completely tracebable supply chain, the mill exclusively uses e3 sustainable cotton.
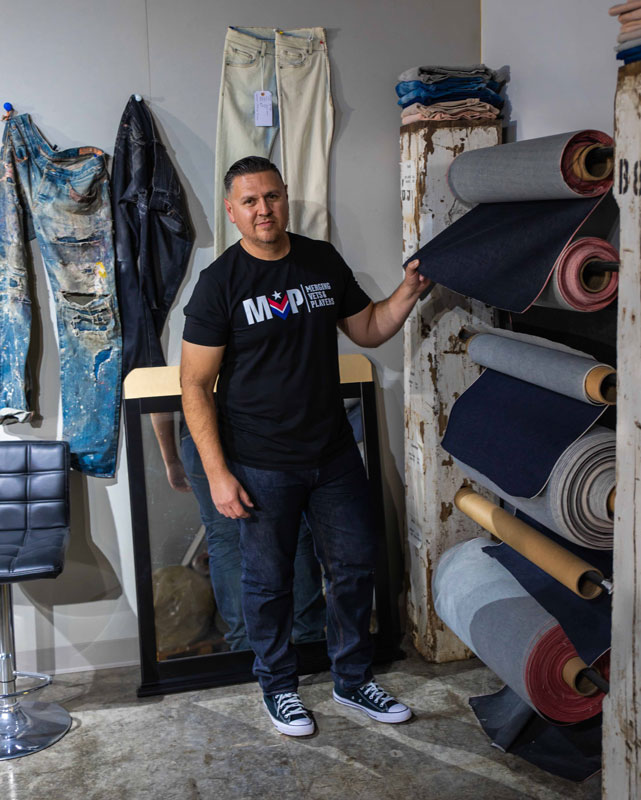
Guests then took a virtual trip to Los Angeles, and listened to the compelling story of Trinidad Garcia III, founder of Trinidad3 Jeans and United States Marine Corps. veteran. His swap from machine guns to sewing machines and passion for community and underserved veterans is interesting enough on its own, but Garcia is also committed to only sourcing cotton and materials from the U.S.
Trinidad Garcia III, founder of Trinidad3
Educating Consumers On Sustainability Red Flags
After hearing from the speakers, the media was then invited to participate in a live Q&A session and discussed topics like supply chain issues (there are none when all your labor and materials are sourced from within the U.S.), product labels, and sustainability.
Betsy Cribb, editor at Southern Living magazine, asked if there were any red flags that consumers should watch out for when purchasing cotton items, like with the word “organic” used in the food industry.
Goldstein answered, “Yes, there are a lot of words, and that issue runs deep, but the word ‘organic’ is misused in the fashion industry nearly as much as it is in food.” Goldstein and Garcia both agreed that there are no government label restrictions, meaning brands can put the word organic or “used less water” on their materials without having to validate those claims.
“That is essentially why we are here,” said Crumpler. “No one is delivering the traceability data and transparency like the e3 Sustainable Cotton program and our partners right here.”
And Vidalia Mills is taking that traceability one step further with the goal of having the entire supply chain — from cotton fiber to finished goods — under one roof.
“The e3 cotton program is very important to us,” said Goldstein. “Our customers want traceable, sustainable cotton and we get that from our e3 cotton. We’re proud that we can show consumers things like when their cotton was harvested and how much water was used growing it. Other brands are claiming this, but only e3 has the data to back up their claims.”
“Brands like ours have to lead by example because consumers are putting their trust in us,” said Garcia. “They deserve a well-made product and to be told the true story behind how it’s [jeans] made.”
And that story starts on the farm.
“As fourth-generation cotton farmers, our job is to leave the land better than we found it,” said Marshall Hardwick. “How we grow our e3 cotton is of the utmost importance and knowing that cotton travels from our gin to Vidalia Mills and then on to brands like Trinidad3 makes us proud to be part of a program that delivers the data and transparency consumers deserve.”
What is the e3 Sustainable Cotton program?
e3 Sustainable Cotton is the only cotton sustainability program that provides traceability starting from the cotton seed and farmer right through to the gin, mill and retailer.
It’s the only cotton sustainability program that tracks environmental outcomes back to each farmer’s individual cotton field and each bale. Using the MyFarms digital platform, the e3 sustainable cotton program tracks 8 sustainability measures:
Irrigation water use and water quality
Pesticide management and usage
Soil conservation and fertility management
Greenhouse gas emissions
Energy use and conservation
Worker health and safety
Identity preservation
Soil carbon.
Editor’s Note: For more information on the e3 Sustainable Cotton program by BASF, visit e3cotton.us.
It was on March 13, 2011, when my friend Craig Wylde was brutally assaulted. Having previously served as Infantry soldier in the British Army, Wylde ultimately became a prison officer at the Category A (high security) Frankland Prison, in Durham, England. One morning he opened a prisoner’s cell door, the prisoner had a broken glass bottle in his hand, he slashed Craig under his arm, he severed his artery, muscle, tendons, ligaments and also created severe nerve damage. Days later the Ministry of Justice changed the law and declared the use of glass bottles and glasses in the prison setting illegal.
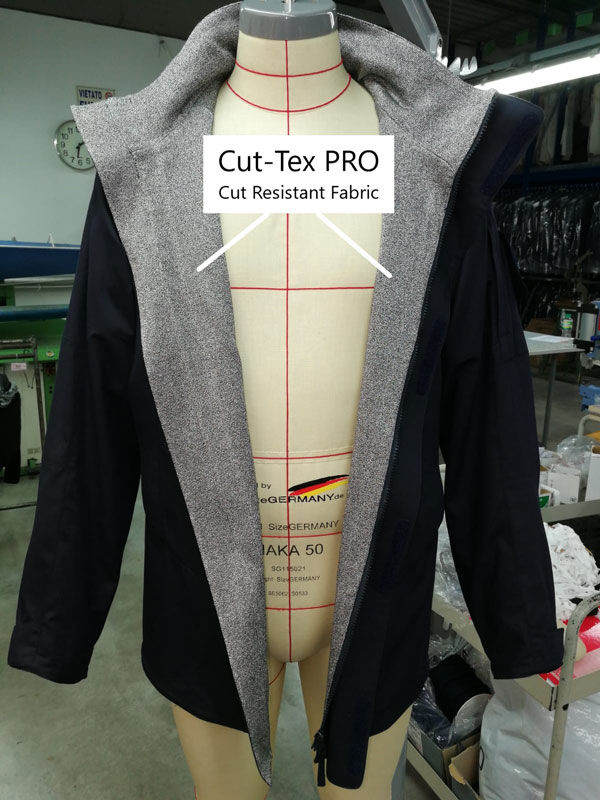
This was an exceptionally tragic incident, which ultimately led to the development, design, and engineering of a high-performance cut resistant fabric known as Cut-Tex® PRO. I had already worked on some type of cut resistant fabrics, but I soon came to realize that “good performance” wasn’t good enough. So, I ended up traveling the world, meeting, and consulting some of the most respected textile engineers on the planet. Thoroughly field tested, this fabric is now allowing us and other protective clothing producers to design and produce protective clothing, reducing injuries and saving lives all over the world.
Other manufacturers of cut resistant fabrics will most likely have their own reasons for having created such type of fabric. Maybe their intentions were of similar nature, maybe they felt it was of commercial interest or it simply fit their existing product portfolio.
Homeland security and law enforcement agencies, prison services, border force, immigration, customs, counter terror units and surveillance teams have all identified a need for cut resistant fabrics and clothing, besides body armor.
We understand that muscles, tendons, ligaments and nerves of these men and women require such level of protection, preventing cut injuries and subsequent, potential rapid blood loss and shock, loss of life or simply immobility — which in certain circumstances can result in loss of life due to lack of the ability to further defend yourself.
We also must acknowledge that significant and life-altering injury can occur even when a wounded officer survives. Too soon and too often the attention wanders and the incident fades into background, while the recovering officer flounders in a morass of work comp, medical bills and looming unemployment.
“Slashing” or “slash injuries” are extremely under-reported. Historically “knife injuries” have been reported as “stab injuries,” hence we have been made to mis-believe that both mean the very same.
However, “a retrospective survey of hospital admissions data suggested that 63 percent of wounds attributable to sharp edged weapons were SLASH events,” stated Ian Horsfall and Mathew Arnold, of the Impact and Armour Group within the Department of Engineering and Applied Science at Cranfield University, Defence Academy of the United Kingdom.
Moving away from slashing, additional markets had their fair share of cut injuries, and subsequently learned to understand the incredible benefits of lightweight and comfortable cut resistant fabrics.
Industries, such as flat/float glass and sheet metal processing, as well as air conditioning companies and recycling facilities have also reported extremely serious accidents resulting in sometimes horrendous cut injuries that needed urgent medical attention, hospital treatment and even long-term care. It is no longer good enough to purchase cut resistant gloves to protect the wearers hands. We have to learn to understand that other areas of the body are of equal or even greater risk.
Mental health care facilities, special educational needs schools, psychiatric nurses, social workers, care homes and others have also identified a need for bite resistant clothing, again made from a cut resistant fabric offering additional protective properties.
We need to stop thinking that everything will be ok. We need to stop believing that nothing is ever going to go to happen, simply based on that fact that the past has been very kind to us, and no one has been injured in our company, facility or organization yet.
The legal, financial and operational consequences for ignoring or neglecting basic health and safety regulations can be severe. The moral consequences for not looking after our workforce and dealing with the aftermath of avoidable injuries can be profound.
Cut resistant fabrics exist and they can effectively help create garments and uniforms, preventing injuries and ultimately save lives. It’s worth it.
Editor’s Note: Robert Kaiser is the CEO and Founder of England-based PPSS Group. Several great video demonstrations of him being subjected to knives, machetes, axes, shanks, other types of edged weapons, as well as blunt objects can be viewed online. Cut-Tex® PRO cut resistant fabric is produced by PPSS Group.
Jingzhi Wang, corporate representative of Luannan Deshun Spinning Mill
TW Special Report
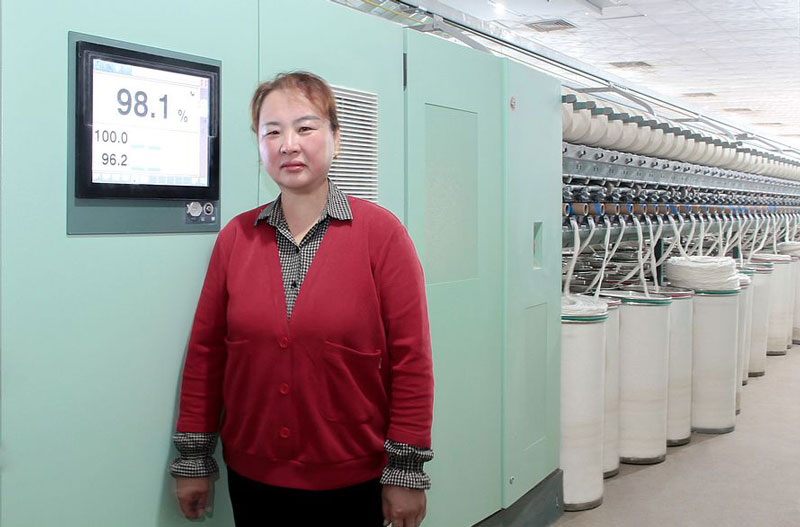
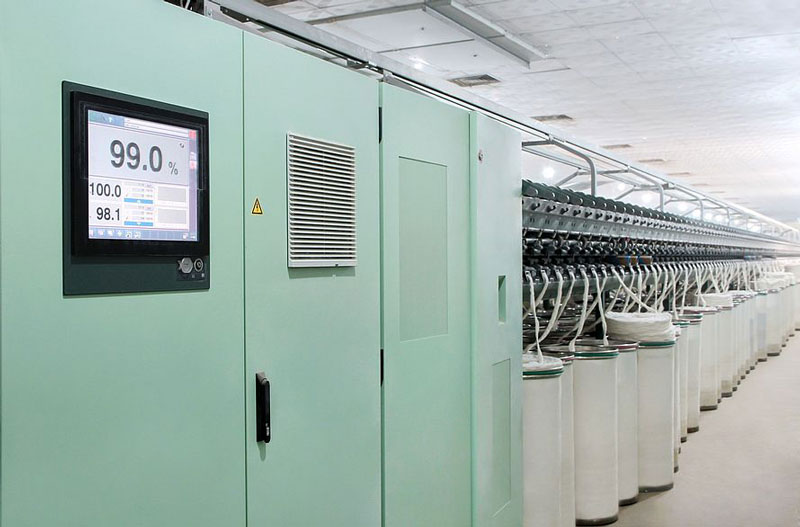
Luannan Deshun Spinning Mill produces Ne 10 recycled cotton soft knitting yarn on semi-automated rotor spinning machines. Located in Tangshan City, Hebei Province, China, the company sells its highly appreciated yarns mainly to customers in Foshan City, Guangdong province and other local areas. The company needed to expand the existing mill set-up of about five to six tons a day to meet the huge demand for recycled cotton yarns. Therefore, Deshun was looking for an efficient rotor spinning machine that could handle the challenges of recycled raw materials and keep up with the market’s fast pace.
The Challenge
The processing of recycled cotton tends to cause higher numbers of ends down. The unstable quality resulting from the material and the opening can cause problems in the downstream processes. The challenge is to get the maximum yield from the given material with the optimum settings and technology. Spinning mills using recycled cotton as a raw material need to find the optimum balance between high production, good yarn quality, high raw material yield and low operating costs.
High yarn quality at delivery speed
The Solution
Based on the raw material data and the existing fiber preparation it was obvious, that the Rieter semi-automated rotor spinning machine R 37 would be the best solution. The spinning box of this machine offers decisive advantages in processing recycled cotton thanks to a higher level of trash extraction. Short fibers are guided well in the feeding and opening areas and most trash, neps and yarn ends which are not fully opened are removed. More good fibers are kept in the spinning process than with other machines. This guarantees better evenness and IPI values which results in lower ends down rates and in economic production. The low energy consumption of the R 37 further reduces the customer’s operating costs.
The Customer’s Benefits
The R 37 produces Ne 10 recycled soft knitting yarn with a delivery speed of 142 m/min. The overall efficiency of the machine is as high as 98 to 99 percent with fewer ends down and stable yarn quality. Deshun reports that the R 37 is more energy efficient and easier to operate compared to its former machines. There is no need to use tools when maintaining the spinning box. The rotor bearings can be lubricated without disassembly. Better fiber utilization and low energy costs increase the benefit. The company is proud of its effective mill management and good cost control. With the R 37 installation, Deshun achieved its goal of zero complaints from downstream customers. Even better, customers now pay a quality bonus.
Yarn demand remains strong across the board, with many spinners, depending upon labor availability, operating at or near capacity.
“The biggest problem remains available human resources,” said one executive. “Even before COVID, many plants were struggling to fill positions. Essentially, it’s been one thing after another, from shutdowns, to enhanced unemployment benefits, to, now, the highly contagious Omicron variant of the disease, which is causing a lot of absenteeism.”
The good news, according to scientists and medical experts, is that the new variant, while more contagious, generally produces less severe symptoms. Also, countries, such as South Africa, that first reported a meteoric rise in Omicron, are now reporting the variant is subsiding just as quickly.
Since the beginning of the pandemic, governmental leaders, scientists, health officials and companies have worked diligently to ensure that, should such a situation develop in the future, nations will not be caught short-handed in their ability to protect their citizens. At the beginning of the COVID-19 pandemic, protective medical gear is such short supply that even critical first-line healthcare workers were not adequately protected.
Medical Textiles Production To Increase
NCTO worked with the U.S. government to ensure the future onshoring of personal protective equipment (PPE) manufacturing. Now, it seems, the rest of the world is on board in increasing overall medical textiles production. According to a new study by market research company Technavio, the medical textiles industry is expected to increase by $3.36 billion from 2020 to 2025. That accounts for a compound annual growth rate of more than 5 percent.
As the study indicates, medical textiles include PPE and a wide range of other products. Nonwoven medical textiles are utilized in items such as absorbent pads, incontinence products, and patient and staff attire. Baby diapers, bed linen, blankets burn dressings, gowns, disposable underwear, dressings, medicine delivery devices, face masks, filter media, nasal strips, pillows, shoe covers, sponges, sutures, tissue scaffolds, towels, wraps, and other products include these substances.
Natural and synthetic fibers are employed in the production of nonwoven medical textiles. Wood-pulp, cotton, and rayon are examples of natural fibers used in non-woven medical textiles. Wood pulp is used because of its obvious absorbency, mass, and low cost, whereas cotton and rayon are soft enough to be used on wounds directly.
Taking Care Of The Environment And People
Last month, it was reported that, Unifi Inc. — among the textile industry’s leading innovators in recycling and sustainability — has now transformed more than 30 billion post-consumer plastic bottles into its REPREVE® brand recycled performance fibers that are used by hundreds of the world’s leading brands. In addition to Unifi, a number of other companies are undertaking far-reaching sustainability initiatives. For example, Elevate Textiles, a global provider of advanced, high-quality products and mission critical textile solutions, recently became the first global textile manufacturer to receive validation of its Science Based Target (SBTi) goals related to reducing greenhouse gas emissions at the highest recommended levels.
As part of its commitment, Elevate recently increased its original greenhouse gas emission reduction target from 2.5 percent to 4.2 percent per year across its portfolio brands of American & Efird (A&E), Burlington, Cone Denim, Gütermann and Safety Components.
Not only are companies in the industry investing in maintain a cleaner, sustainable environment, but they are also working to help better their communities in other ways. Standard Textile Co. Inc., which serves the healthcare and hospitality textile markets, announced on January 18 a national program to combat homelessness. Through partnership with non-profit organizations across the United States that provide mobile shower services to people dealing with homelessness or insufficient housing, the company met its goal of supporting 80,000 showers by the end of 2021.
“On any given day, more than a half million Americans experiencing homelessness may not have regular access to basic essentials many of us take for granted, including a shower or a soft towel. A shower can do so much more than offer personal hygiene; it can restore dignity, something everyone deserves,” said Gary Heiman, Standard Textile’s President and CEO.
Fiber Industries Expands
Fiber Industries in mid-January announced plans to expand operations in Darlington County, S.C. The company’s more than $30 million investment will create 50-plus new jobs.
A full-service manufacturer, Fiber Industries produces polyester staple fiber for high-end performance fabrics, workwear, knit goods, the automotive industry and more.
Currently employing more than 300 people, Fiber Industries’ expansion includes increased capacity through the restoration and modernization of production lines. The company will also use the additional investment to install state-of-the-art control systems and increase warehouse space.
The expansion project is expected to be completed in early 2023.
“We are excited about the continuing growth of our facility which is now even better positioned to serve the needs of the American textile industry,” said Fiber Industries CEO Don Bockoven. “We also are proud to be part of the wider effort to reshore jobs and bring textile manufacturing back to the USA. We thank the state of South Carolina as well as Darlington County for their unwavering support.”
CLEVELAND, Ohio — January 17, 2022 — Rich Gojdics has been named senior vice president of Industrial Sales at National Safety Apparel (NSA). Rich joined NSA through the recent acquisition of Enespro LLC where he held the position of vice president, Business Development.
In his 27 years in the protective apparel industry, Gojdics has successfully led industrial sales teams in protective fabrics and finished PPE. These teams consistently delivered impressive results and significant returns for established companies and new ventures. He also partnered with hundreds of end users to enhance their education of industry standards and help them write PPE specifications.
In his new role as senior vice president of Industrial Sales at NSA, Gojdics will be responsible for developing NSA’s sales strategy, organizational structure, sales budgets and for leading NSA’s industrial sales team.
NSA CEO and Owner Chuck Grossman, shared: “Rich’s extensive experience in the protective apparel market brings a seasoned, skilled leader to lead NSA. I am confident that his proven sales results and long-term relationships in the industry will drive organic sales for National Safety Apparel.”
Mike Enright, newly-named NSA President and former Enespro president & CEO, echoes Chuck’s sentiments about Gojdics: “I’ve worked with Rich for more than 20 years, and his commitment to continuous improvement, and to helping the people he leads become successful, has shown in the profitable results he has delivered. He has also brought a tremendous amount of value to the entire PPE marketplace over the years.”