GÅNGHESTER, Sweden— March 25, 2019 — With more than 5,000 tailored installations for a range of industries installed in over 60 countries, Eton Systems, headquartered in Gånghester, Sweden, has established a reputation as a clear leader in the field of complete material handling systems.
At ITMA 2019 in Barcelona from June 20-26, the company will be demonstrating a complete installation based on a future production concept, with advanced software providing real-time information covering every aspect of the process.
“Our systems are a natural fit with the major Industry 4.0 networked manufacturing plants that are now being constructed worldwide for sectors such as the garment and home textiles manufacturing and automotive industries,” said Eton’s Sales and Commercial Director Roger Ryrlén. “We have had a very busy last 12 months, with more major projects in the pipeline. We understand, however, that one solution does not fit all situations, which is why we think in terms of custom-made solutions matched to specific customer needs. Buying a system from us, is buying a solution and a partnership. Each system includes support, service, training and knowledge built on more than 70 years of experience. When a customer invests in an Eton System the increased efficiency normally results in savings of between 40-60 percent.”
A typical system consists of overhead conveyors with individually-addressable product carriers which automatically steer their way through programmed operation sequences. They are monitored by a computer providing all the necessary data for optimally measuring and managing processes. The systems are also highly flexible and can be rapidly modified to changes in the production line or the need for expansion.
Options for smart factories
Eton’s Flexible Productivity Concept (FPC) is based on two system platforms with a wide range of options, including:
Multiple rails for sorting at workstations.
Buffering.
Automatic loading devices, pick-ups and work delivery robots.
Bridges and elevators that link systems and floors.
Historical links to products after completion.
Module-based software.
Via an addressable product carrier, an Eton system transports all the components of a complete product through the manufacturing process.
“The result is fully automated flow with complete control of every component for the end product — where they have been, where they are now and where they are going” Mr Ryrlén explains. “These are real Internet of Things installations and every component has its own unique identity due to the integrated transponder in each carrier.”
Eton is a member of TMAS — the textile machinery association of Sweden which will have a significant presence at ITMA 2019 in Barcelona.
“Eton Systems is truly embracing the latest Industry 4.0 concepts for fully automated work flows that are now revolutionising the textile industry,” said TMAS Secretary General Therese Premler-Andersson. “There will be many more innovations on show from our members at ITMA 2019.”
Eton Systems will be at stand A214, in Hall 2 at the Barcelona exhibition.
Posted March 25, 2019
Source: TMAS – The Textile Machinery Association Of Sweden/Member Eton Systems
SCHWÄBISCH HALL, Germany — March 25, 2019 — FONG’S EUROPE, based in Schwäbisch Hall, Germany, will celebrate the 100th anniversary of its flagship THEN brand for advanced dyeing technology with a special reception for customers and agents at ITMA 2019 in Barcelona.
The company, which has been a member of the CHTC FONG’S group since 2004, has its origins in the German city of Chemnitz, where back in 1919 Rudolf Then founded a barrel-making business which soon branched out into piece dyeing machines.
The company’s reputation for innovation began early, with the introduction of ceramic linings for dye baths, which were then made of wood, in order to avoid staining and allow easy cleaning. At the end of the 1920s, Rudolf Then was also quick to recognise the acid-resistant advantages of stainless steel for dyeing vessels.
Relocating to West Germany after World War 2, Rudolf Then ran a number of businesses in Schwäbisch Hall, eventually founding THEN in 1955 with partner Karl Kurz, who later took over the business specializing in dye vats and other textile equipment.
Milestone
Throughout the 1960s and 70s, the company continued to further improve its technologies, but it was the introduction of the first THEN AIRFLOW system at ITMA 1983 in Milan which significantly boosted the company’s fortunes, representing a milestone in the development of dyeing machines.
Prior to this, the dyeing of just one kilo of fabric required around 150 litres of water and THEN’s AIRFLOW system, invented by engineer Wilhelm Christ and colleagues, drastically reduced the requirement to between just 35-40 litres. Instead of the traditional dye liquor used for hydraulic fabric transport it efficiently distributed much smaller amounts of dye liquor via aerosol. This technology has subsequently been further developed in successive machine models and has made an enormous impact on sustainable dyeing operations.
Now, as Fong’S Europe, the company continues to innovate, and at ITMA 2019 is showcasing the THEN SMARTFLOW TSF hydraulic high temperature dyeing machine, designed to achieve the lowest possible energy and water consumption rates available on the market for jet dyeing.
The company has a number of patents pending on the innovative new features of this machine, including the SMARTFLOW’s fabric transport design. This is based on a smart, winchless fabric transport system which eliminates the need for a loading rope, and a circular plaiter with programmable rotation speeds which provides full filling of the drop zone.
Its newly-developed nozzles and reel-less transport, in combination with smart controlled circular plaiting and variable chamber adjustment, provide even fabric treatment without entanglements and the highest loading capacity with the lowest kier volume
“Further developments, including the new THEN AIRFLOW PLUS system with a round design are in the development pipeline and will once again result in further reductions in power consumption without sacrificing performance,” said Fong’s Europe Sales Director Richard Fander. “Similar innovations are being made to our hydraulic long shape machine, the THEN SUPRATEC LTM. The ability to transport fabrics with reduced tension and without the need for a transport winch which is being introduced on all of our recent machines will allow new fabrics to be created and further increase the efficiency of textile finishing.
“Fong’S Europe has invested significantly in research and development activities over the past few years, in order to deliver these unique and patented developments for discontinuous dyeing machines to the market,” Fander concluded. “The innovation will continue.”
Fong’s Europe will be at stand D101 in Hall 2 at ITMA 2019.
HIGH POINT, NC — March 25, 2019 — American Silk Mills today announced that Todd H. Nifong has joined the company as director of Residential Sales and New Business. Nifong will report to David Corbin, CEO of American Silk Mills, and will lead a sales team that will focus on the residential, jobber, designer and e-commerce end markets. Under his direction, Nifong will be responsible for the development of the company’s sales and marketing strategies, as well as exploring and validating growth opportunities in adjacent markets.
Nifong has more than 17 years of experience in the home furnishings and textile industries, with executive positions at Altizer & Co. Decorative Textiles and Swavelle Performance Fabrics LLC. Nifong also serves as chairman of the International Textile Alliance (ITA) Educational Foundation, and has been a past recipient of the ITA Future of the Industry Award as well as the ITA Best in Innovation Award.
“Todd brings an excellent blend of entrepreneurial skills with extensive general management and sales experience to American Silk Mills, and he knows this industry well,” said David Corbin, CEO at American Silk Mills. “Todd is the type of individual that will roll up his sleeves and get things done, and we believe he will help implement strategies and solutions that will drive organic and acquisition growth opportunities for the company.”
Nifong will be a part of the leadership team at American Silk Mills, and will recruit and expand the sales force to better service top priority markets and territories. He will also be responsible for gathering unique customer insights and market knowledge that will help increase the speed-to-market of American Silk Mills innovations.
“I am looking forward to leveraging the operational synergies that now exist with American Silk Mills and Sutlej Textiles and Industries Limited, as they will enhance our ability to produce a market-leading range of luxury textiles more cost effectively,” said Nifong. “Customers will benefit from faster response times, a more versatile product assortment, and a wider range of price points for our products. I can’t imagine a better time to be joining American Silk Mills.”
Posted March 25, 2019
Source: American Silk Mills / Sutlej Textiles and Industries Limited
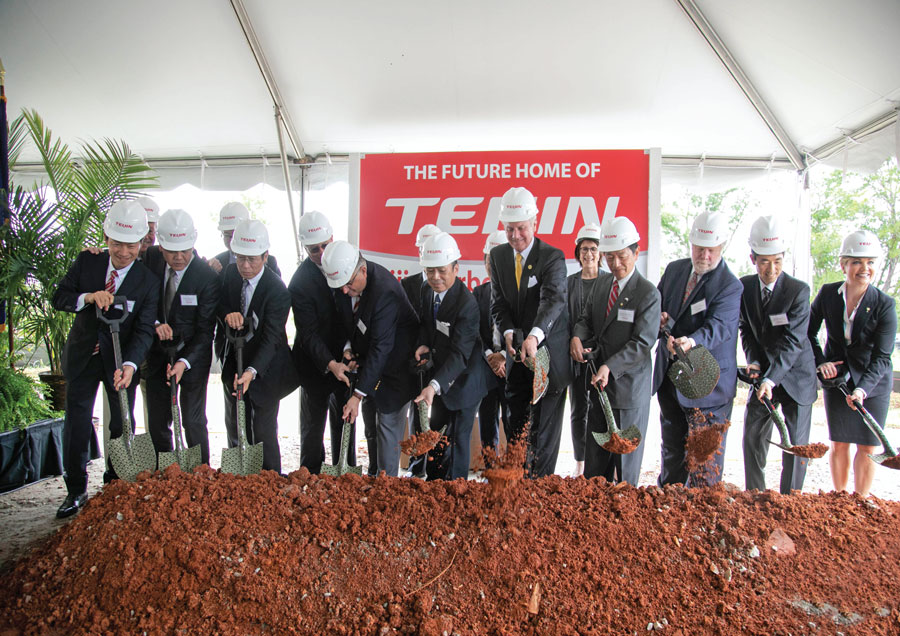
Teijin celebrated the groundbreaking ceremony for its $600 million carbon fiber production facility in Greenwood, S.C.
The United states continues to attract investment, both foreign and domestic, in a range of industry sectors.
TW Special Report
U.S. manufacturing continues to progress in 2019. The latest Manufacturing ISM® Report On Business® published by the Tempe, Ariz.-based Institute for Supply Management® (ISM®) continues to report positive news: “Economic activity in the manufacturing sector expanded in February, and the overall economy grew for the 118th consecutive month, said the nation’s supply executives.” And the same report stated that of the 18 manufacturing industries, 16 reported growth in February, with the “Textile Mill” sector ranking third out of the 16 sectors.
Challenges Continue
The challenges facing the U.S. textile industry no-doubt continue and international trade law is still in flux, but the current industry sentiment and capital spending are bright signs for the future. And the influx of foreign direct investment speaks positively for manufacturing in the United States. The following reviews Textile World investment news headlines from the past year as a recap of recent textile business activities. Keep in mind, there are many quieter projects taking place that never make the news.
Carbon, Composites Investment
Last year, Tokyo-based Teijin Ltd. broke ground on a new carbon fiber plant in Greenwood, S.C. The plant will be part of its wholly-owned subsidiary Teijin Carbon Fibers Inc. (TCF). The total investment is expected around $600 million by 2030, and the TCF facility is expected to employ 220 people.
“We look forward to this new chapter of Teijin’s expansion in the U.S.,” said TCF president, Yukito Miyajima. “We are strengthening its global upstream-to-downstream carbon fiber business. We have been leveraging research and development to expand carbon fiber business in the aircraft and automotive fields. Throughout this process, we looked at multiple locations, but ultimately, with the support of local and state government officials, we chose Greenwood as the ideal location for our new U.S. carbon fiber facility.”
More recently, Teijin announced that its Tenax carbon fiber and carbon fiber thermoplastic unidirectional pre-impregnated tape known as Tenax TPUD were qualified by Chicago-based Boeing and registered in its qualified products list. Teijin said it will supply Tenax TPUD as an intermediate advanced composite material for primary structural parts for Boeing.“Going forward, Teijin intends to further strengthen its carbon fiber and its intermediate material business as a leading solution provider for aircraft applications, targeting annual sales in this field in excess of $900 million by around 2030,” reported Teijin.
In other Teijin investment news, the company just announced that it has agreed to acquire Renegade Materials Corp., a Miamisburg, Ohio-based supplier of highly heat-resistant thermoset prepreg for the aerospace industry. Renegade will become a wholly-owned subsidiary of Teijin.
“Teijin will benefit from Renegade’s well-established proprietary technologies and solution capabilities in heat-resistant thermoset prepregs to expand its business in aerospace field including next-generation aircrafts’ engine parts,” stated a Teijin press release about the acquisition. “Renegade’s products will reach wider markets thanks to Teijin’s expertise in carbon fibers and intermediate materials as well as its large product lineup and global sales network. Global marketing initiatives will be supported by Teijin’s carbon fiber business, including Teijin Carbon Fibers Inc., which plans to launch a new carbon fiber production facility in South Carolina by the end of FY 2020; Teijin Carbon America Inc., a carbon fiber sales base in Tennessee; and Teijin Carbon Europe GmbH, a core company of the carbon fiber business in Europe.”
Traditional Textiles Moving Forward
Late last year, Gastonia, N.C.-based Beverly Knits Inc., announced the expansion of its manufacturing footprint. In addition to purchasing new finishing equipment, Beverly Knits also established a new company named Altus Finishing LLC.
According to the company, Altus Finishing will offer commission finishing services for the bedding, industrial and apparel markets. Dyeing, heat-setting, tumbling, shearing and specialty coatings are among the services offered.
“Beverly Knits is excited to add dyeing, finishing and coating to our manufacturing capabilities,” said Ron Sytz, owner of Beverly Knits and Altus Finishing. “The Altus Finishing team is experienced in many markets and will complement the capabilities of the Beverly Knits companies including Creative Fabrics and Creative Ticking.”
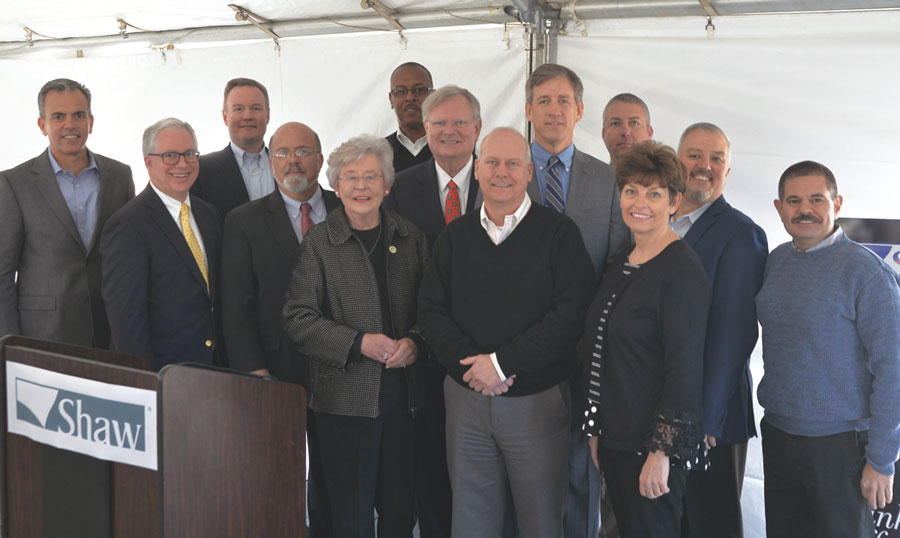
Alabama Governor Kay Ivey, Andalusia Mayor Earl Johnson and Covington County Commission Chairman Greg White joined Shaw Associates to celebrate its modernization investment.
Floorcovering Not To Be Out Done
At the end of last year, Dalton, Ga.-based Shaw Industries Group Inc. announced that it will invest $250 million in its Andalusia, Ala., manufacturing facility, which creates fiber used to manufacture residential carpet.
The company reports that the project includes construction of new and expanded building assets, and installation of substantial amounts of new manufacturing equipment. The changes will create better efficiency, production, ergonomics, and safety for the more than 1,200 associates who work at the plant.
David Morgan, Shaw Industries’ executive vice president of operations, stated: “At Shaw, our vision is to create a better future for our associates, our customers, our company, and our communities. We can only achieve that vision through continued investment in our people, our products, our facilities, and our operations. We continually bring customers the forward-thinking products and services they expect from Shaw.”
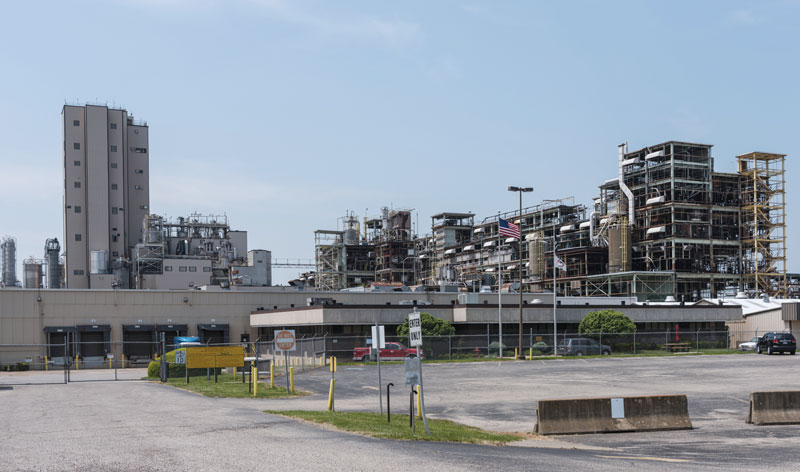
Corpus Christi Polymers LLC — a joint venture between IVL subsidiary Indorama Ventures Holding, Alpek S.A.B. de C.V. and Far Eastern Investment (Holding) Ltd. — entered into an asset purchase agreement with M&G USA Corp. to acquire its integrated PTA-PET plant under construction in Corpus Christi, Texas.
Indorama Ventures Dominates The Headlines
It seems that Bangkok-based Indorama Ventures Public Co. Ltd. (IVL) is continually announcing an expansion of its global footprint.
One of the company’s U.S.-related investments was announced at the beginning of last year when IVL and South Korea-based Huvis Corp. (HC) said they planned to join forces and develop, construct and operate of a low melting fiber (LMF) plant in the United States in a 50:50 joint venture (JV).
Huvis Indorama Advanced Materials LLC represents a $48 million investment and is located at Auriga Polymer Inc.’s campus in Spartanburg County, S.C. Annual capacity at the state-of-the-art plant is expected to be 60,000 metric tons, and the plant will create 50 new jobs. Initial volumes of LMF will be sold in the United States, “with its new low tax environment and the potential to significantly expand its scope into neighboring regions over time,” according to IVL. LMF sales are expanding at a rate of 8-percent a year as manufacturers have been converting from conventional chemical adhesives to thermobonding methods, reports the company.
Other recent IVL investment-related headlines include:
An agreement to acquire a polyester (PET) recycling facility from Custom Polymers PET in Alabama. The facility consists of two production lines — recycled PET (rPET) flake and food-grade rPET Pellets, with a combined capacity of 31,000 metric tons per year.
The acquisition of INVISTA Resins & Fibers GmbH, a specialty chemicals asset located in Gersthofen, Germany. The Gersthofen site has a combined capacity of 282,000 metric tons per year and employs approximately 140 employees.
An agreement to acquire UTT Beteiligungsgesellschaft mbH. UTT is a supplier of airbag fabrics and other highly specialized solutions in the field of technical textiles. The company has two sites in Germany and Mexico producing approximately 70 million square meters of fabrics with approximately 420 employees.
A JV to purchase M&G USA Corp. and form Corpus Christi Polymers LLC. The purchase agreement provided M&G with a binding bid of $1.125 billion in cash and other capital contributions.
IVL plans to acquire M&G Polimeros Brazil S.A. in Ipojuca Brazil. The plant is the largest PET facility in Brazil.
The acquisition of a 65.72-percent stake in Avgol Industries 1953 Ltd. An Israel-listed global manufacturer, Avgol is the third largest manufacturer of nonwovens for hygiene applications in the world, and holds a global market share of 10 percent.
Recycling Investment In The News
DAK Americas LLC, an Alpek polyester company, recently signed an asset purchase agreement with Perpetual Recycling Solutions LLC for its polyethylene terephthalate (PET) recycling facility in Richmond, Ind.
The operation has an approximate capacity of 100 million pounds per year of high-quality, rPET flake. Terms of the agreement were not disclosed. The Perpetual acquisition will fit in well with Alpek Polyester’s Argentina-based food-grade PET recycling facility as well as its Fayetteville, N.C.-based fiber-grade recycling joint venture, according to the company. “The addition of this facility will allow us to expand our sustainability initiatives,” said Jon McNaull, vice president, PET Resins, DAK Americas.
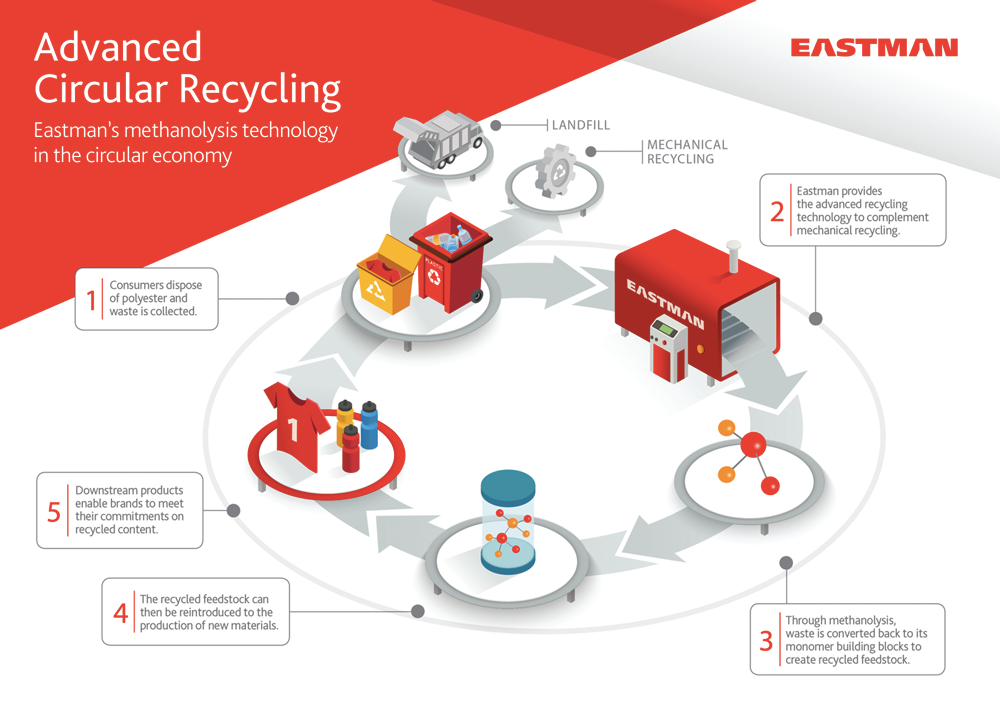
Most recently, Kingsport, Tenn.-based Eastman announced that it is conducting “an engineering feasibility study on the design and construction of a commercial scale methanolysis facility to meet the demands of our customers and has engaged in initial discussions with potential partners across the value chain on the development of such a facility.” Methanolysis is an innovative advanced circular recycling technology that uses polyester waste that cannot be recycled using currently available mechanical methods. The process breaks down polyester-based products into polymer building blocks to be reintroduced into the production cycle for new polyester-based polymers. According to Eastman, the company was “one of the pioneers in developing methanolysis technology at commercial scale and has more than three decades of expertise in this innovative recycling process.”
Eastman’s advanced circular recycling complements basic mechanical recycling, using methanolysis to return polyesters back to their polymer building blocks.
Eastman reports its goal is to open a full-scale, advanced circular recycling facility in the next two to three years.
“We recognize that plastic waste is a complex problem that needs advanced solutions,” said Mark Costa, Eastman’s board chair and CEO. “As we have engaged potential partners, it is clear there is high interest across the entire value chain. Our long history of technical expertise in chemical processes, including methanolysis, and our leading position in copolyester chemistry, enables us to provide this innovative solution to address the growing challenges of plastic waste in our environment.”
Polypropylene Investment
Irving, Texas-based ExxonMobil recently announced it will soon begin construction on a new polypropylene production unit in Baton Rouge, La., that will expand capacity of polypropylene along the Gulf Coast by up to 450,000 tons annually. Startup is expected by 2021, and the facility will employ 65 once operational. The company sees demand for polypropylene in everyday consumer products, but especially in lighter-weight auto parts for increased fuel efficiency.
“Growth in feedstock supply along with the increase in global demand for chemical products continues to drive our strategic investments and expansion along the Gulf Coast,” said John Verity, president, ExxonMobil Chemical Co. “We’re well positioned to meet the demand for these high-performance products and investing further in Baton Rouge enhances our facility’s competitiveness.”
Advanced Materials On Deck
Last fall, ShayoNano USA Inc. announced plans to construct a new manufacturing facility in Chester County, S.C. An innovative developer of advanced materials, Shayo-Nano’s $14.7 million capital investment is projected to bring approximately 40 new jobs to the community.
According to the company, its nanomaterials — including synthesizing additives that improve the profitability and performance of a variety of products — support a variety of applications such as coatings and paints, fire retardants, and nanocomposites.
Investment Continues
According to the Washington-based National Council of Textile Organizations (NCTO): “The U.S. textile industry invested $20 billion in new plants and equipment from 2006 to 2016. Recently, U.S. manufacturers have opened new facilities throughout the textile production chain, including recycling facilities to convert textile and other waste to new textile uses and resins. And, U.S. textile mills have increased labor productivity by 60 percent since 2000.”
That doesn’t sound like an industry in decline, just take a look at the headlines!
Figure 1: The team plotted where these initial markets were with respect to the Gartner Hype Curve to illustrate why they had to pivot.
A team of researchers from NC State University’s Wilson College of Textiles embarked on a journey to learn about commercializing a smart fabric technology.
By Dr. Raj Bhakta and Dr. Jesse S. Jur
We have smartphones, smart TVs and smart cars, but where are the smart clothes? This question has been asked several times, and it’s a question also asked by researchers in wearable technology and smart fabrics. When it comes to clothing that can say monitor health and well-being, it was assumed if it was made, people would buy the technology. But markets don’t behave that way, and not all technology sees the light of day in the marketplace. Many of the world’s discoveries are still sitting in research labs all around the world in what is commonly known as the “valley of death.” A team of wearable technology and smart fabrics researchers from the Wilson College of Textiles at Raleigh, N.C.-based North Carolina State University (NC State) didn’t want to be stuck in that valley — their goal was to cross the valley.
The NEXT research team consisted of Dr. Jesse Jur, a NC State Wilson College of Textiles associate professor of Textile Engineering, Chemistry and Science, and thrust leader in Wearability at the National Science Foundation (NSF)-funded Engineering Research Center on Advanced Self-Powered Systems of Integrated Sensors and Technologies (ASSIST); Entrepreneurial Lead doctoral student Raj Bhakta; as well as seasoned entrepreneurial executive Bob Sheehan, who had served as a national sales executive at Gillette and numerous pharmaceutical companies. Excited by the prospect of making an impact in the industry of smart textiles, the team set out to see what opportunities were out there for this burgeoning space.
Most often, researchers ask probing questions, identify hypotheses, and design experiments to validate the hypotheses — also known as the scientific method. In the world of science, discoveries are non-linear and require both analytical and qualitative thinking. Having worked through this method, the research team wanted to dive deep into the fundamental problems from a business standpoint and determine why we don’t have smart clothes that monitor one’s health among other futuristic features.
Before getting into the nitty gritty of the research team’s journey towards bringing a smart fabrics technology to market, let’s talk about what are smart clothes and some history about this field.
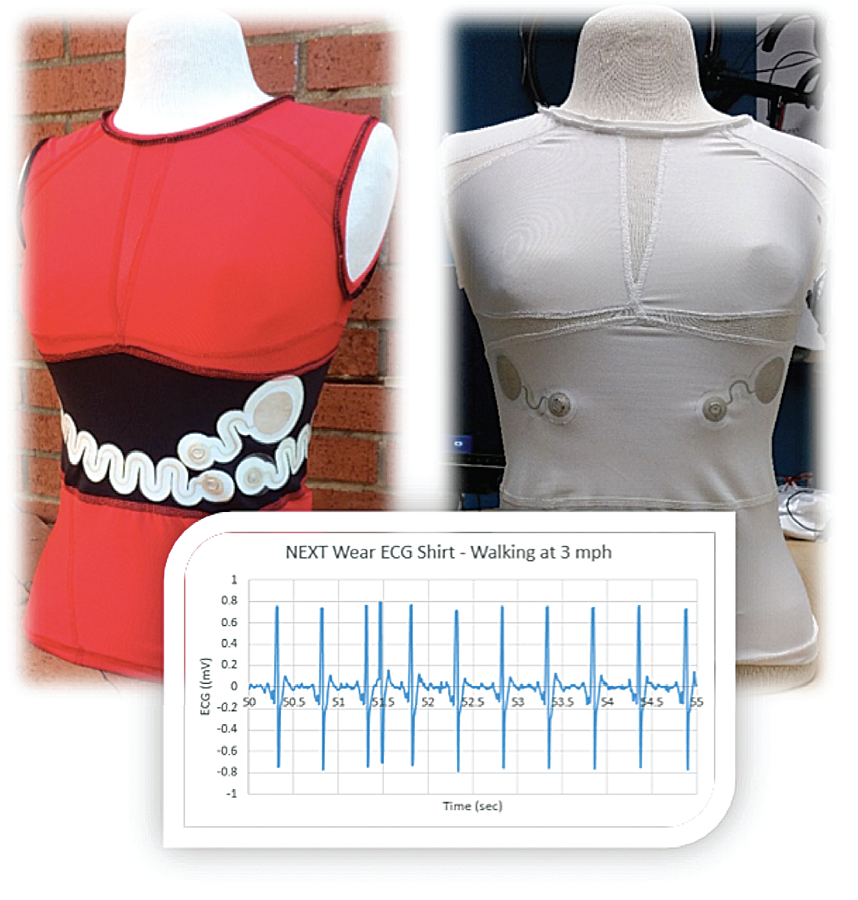
Figure 2: The smart garment that the researchers were proposing as their solution to the pain point of tracking law enforcement officer’s stress levels.
What Are Smart Clothes?
Clothes are integral to the human condition — they’re used to express identity, protect from the environment, and now are being used in health applications. There’s a wide variety of use-cases, but the first documented idea for an intelligent shirt came from Atlanta-based Georgia Institute of Technology professor Dr. Sundaresan Jayaraman who coined his invention “Smart Shirt.” His vision was to add computing technology into a shirt that could measure one’s vital signs and become an interface between a patient and doctor. This early 1990s vision was ahead of its time, and it is seen today used in the form of remote health monitoring applications. However, in this case — in the world of textile electronics, or textiles that have electronic features — the clothing acts more like an electronic device rather than just a piece of clothing. Research performed at NC State and the ASSIST engineering research center deals with making clothing smart and integrating sensors in a way that’s comfortable for the wearer. For example, the team has demonstrated a garment for monitoring electrocardiogram (ECG) for health analysis that is powered by a wearer’s body heat.
Where Are Smart Clothes?
The NC State research team found out about a program called NSF Innovation-Corps (I-Corps™), which is part start-up accelerator and part start-up boot camp. The NSF reports that the program “prepares scientists and engineers to extend their focus beyond the university laboratory and accelerates the economic and societal benefits of NSF-funded, basic research projects that are ready to move toward commercialization.” Its mission is to teach entrepreneurship to scientists using the scientific method of entrepreneurship called the “Lean Start-Up Methodology” started by Steve Blank. It’s a sharp-shooting, intense, and hyper-focused crash course in whether a scientific invention has any value to the greater marketplace that comes with guidance from established entrepreneurs.
Because its their area of study, the NC State research team was naturally interested in smart clothing with the capability to measure a person’s vital signs; however, they always questioned who would use these garments and why, and if they would be treated like regular clothing? These questions kept spinning in the team’s minds, and as they got into the NSF I-Corps Fall 2016 cohort in Los Angeles, they finally had a chance to pursue those questions and learn all about the Lean Start-up Methodology.
The team arrived at the boot camp with a modernized version of the business plan known as the “Business Model Canvas.” The business model canvas was filled out with the first initial market and the hypothesis the team was looking to test. The team presented “Corporate Wellness” as their first market and shared their assumptions on stage at the boot camp, then split up to conduct interviews with the large companies, the California Department of Transportation and health care providers. After extensive qualitative interviews, the team discovered that corporate wellness was a saturated market.
The team dived deeper into identifying who exactly would use the technology and interviewed actual consumers. They went to strip malls and popular sporting goods stores like Lululemon and Dick’s Sporting Goods and interviewed consumers about wearable technology and whether they’d buy smart shirts that were more accurate than a Fitbit and Apple Watch. Most of the interviewed consumers were millennials but still didn’t care much about the technology of smart clothing.
After a day of interviews, in addition to learning that the corporate wellness market was saturated, the research team also discovered that consumers thought wearables were “nice to have”, but didn’t care too much about fancy smart shirts when a Fitbit was “good enough.” Good enough sometimes is the best solution, and the team learned the hard way that no matter how great the technology is, if no one wants it you don’t have a real business. It was a good lesson.
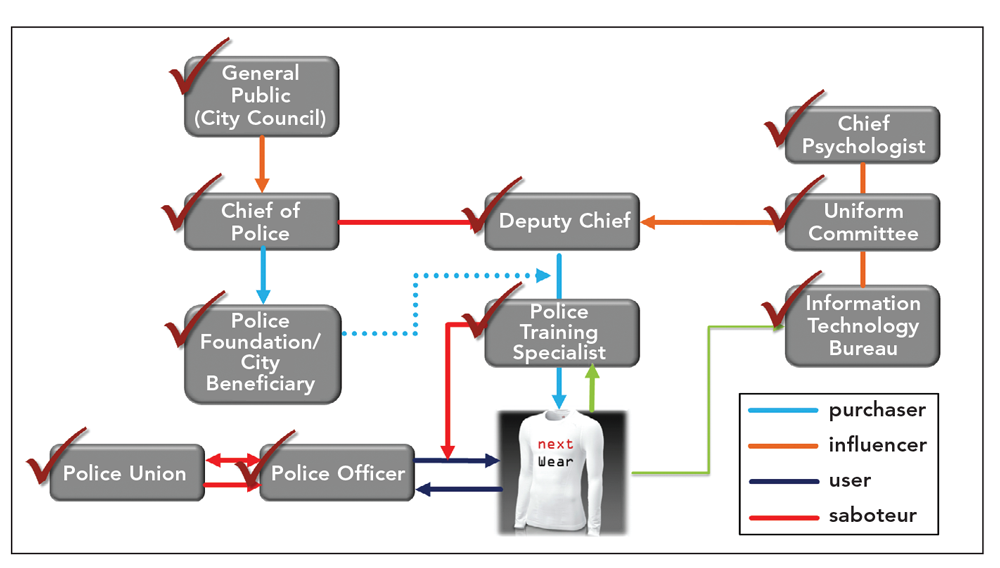
Figure 3: The value chain ecosystem of stakeholders that were interviewed to understand the market need, potential buyers for the solution and what design specifications the garment needed to meet.
Pivots, Pivots, Pivots
The team shifted focus. One of the key interviews conducted during the Los Angeles journey was with law enforcement officers. The researchers found that if there was a way to track stress during law enforcement training and allow new officers to understand when stress is increasing, the officers can learn to manage the stress and prevent adverse outcomes from occurring. Managing stress in this way can save the law enforcement agency money and operational burdens, as well as increase the well-being of the officers and citizens. It sounded like a win-win for everyone. The team decided law enforcement would be its “beachhead market” — a market that’s currently underserved and would be open to a technology launch.
As the team continued its customer discovery in the market of law enforcement, it found that buying cycles, budgets, and the total addressable market wouldn’t make for a sustainable business. In addition, the most critical thing learned was that the unit economics — or the amount of money that can be earned from the lifetime of a customer to the amount it takes to acquire and sustain that customer — did not make sense. The fundamental reason for this is that the technology for smart clothing and the greater smart clothing market wasn’t making much profit. It is a small niche market and manufacturers who are able to make these textile electronic devices didn’t have the automation to lower the costs. To put things into perspective, the researchers found that the cost of a smart shirt produced in Asia was $60 and took around 3 hours using a skilled team of 20 people. This was a shocking discovery for the team, and a bit humbling at the same time. The reality is that most smart garments were made using conductive yarns to embroider and stitch, which at the time was a process utilizing little to no automation. In an industry where labor is a large component of the product manufacturing, the addition of complex electronic features adds a layer of complexity that the industry is not accustomed to. The NC State team found when diving deep into the smart fabric supply chain that there’s an inherent need for automation to produce these next generation pieces of smart clothing. This was not a pivot just for the business case, this was a pivot for the team’s technology. The researchers learned that they should instead go back to the lab and work on the technology to enable the proper unit economics that wearables and smart clothing in general will fit into.
The Path Forward
As wearables become a fact of digital and personalized health, it’s only a matter of time until clothing becomes part of the value chain of healthcare. The clothing companies of the future will integrate more and more technology into their products and provide additional value to their consumers. This transformation will usher in a new functionality for fashion and clothing. Imagine a world where clothing is a point of care for health. To make that vision a reality requires researchers to solve the technological problems to enable use-cases with unit economics that can create sustainable new ventures.
Editor’s Note: Dr. Raj Bhakta is a recent Ph.D. graduate from NC State’s College of Textiles and the ASSIST self-powered wearables research center, whose research was focused on smart textiles manufacturing and next-generation wearable technologies. He is the cofounder and CEO of Funxion, an early-stage start-up company working to create smart fabric products all the way from “Atoms-to-Apparel.” Dr. Jesse Jur is an NC State Wilson College of Textiles associate professor of Textile Engineering, Chemistry and Science; Thrust Leader in Wearability & Data at the ASSIST self-powered wearables research center; and principle investigator of the NEXT Research Group. He’s actively involved in the commercialization of technologies as well as innovation within the greater sphere of smart fabrics. To learn more, visit next.textiles.ncsu.edu; or follow the group on Instagram @ncstate_nextresearch.
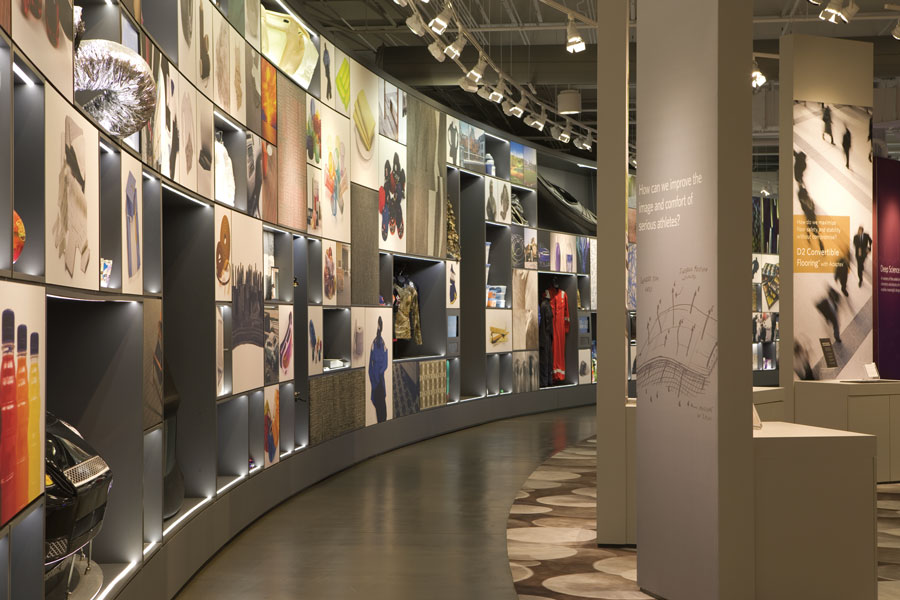
Milliken’s Roger Milliken Center features an Innovation Gallery showcasing the company’s advanced textile technologies.
A new Milliken website helps clients access the depth and breadth of Milliken’s technology trove of innovative, amazing textiles.
TW Special Report
In many ways innovation in the textile industry is synonymous with Spartanburg, S.C.-based Milliken & Company. Founded in 1865, the company’s history in textiles stretches back more than 150 years.
Milliken & Company’s strong culture of innovation, which was shaped personally by the late CEO Roger Milliken, began in 1945, when the company formally established its research group. Milliken bet the company’s future on continuous product development — making a corporate commitment to conceptualize and create cutting edge textiles. To do so, Roger Milliken personally involved himself in reviewing research and invited preeminent minds in engineering and chemistry to help guide future projects. Milliken also challenged his research associates to look for the very best brains in the world. He commissioned his scientists to contact schools that were prominent in chemistry, chemical engineering and mechanical engineering to find the best students of the previous 10 years. This recruitment effort was at the core of a serious research commitment that continues to this day.
The Roger Milliken Center (RMC) recently celebrated its 60th anniversary. RMC is home to the company’s global headquarters and corporate innovation center — one of the world’s largest privately-held textile research facilities.
Today, Milliken operates three divisions — Performance and Protective Textiles, Floor Covering, and Chemicals. With innovation firmly woven into Millken’s DNA, staying on the forefront of technological advances is a priority. When challenged to solve a problem, Milliken’s team of researchers, chemists, engineers and developers work together to create best-in-class technical solutions, while investments in innovative technologies ensure the company remains cutting-edge.
Milliken’s team of researchers, chemists, engineers and developers work together to create best-in-class technical solutions.
Improving Access To Milliken’s Technologies
Through its Performance and Protective Textiles division, Milliken serves a range of industries including apparel, automotive and transportation, building and infrastructure, hospitality, industrial, military, interiors, and protective markets.
The company’s new website, launched under the tagline “Textiles from a Different Perspective” and located at textiles.milliken.com, unifies the diverse portfolio of the Performance and Protective Textiles division, showcasing its breadth of capabilities and highlighting the company’s expertise and next-generation products. The website also illustrates the successful history of Milliken textiles, its legacy and ability to collaborate with customers to solve complex problems.
“Milliken is synonymous with credibility within textiles,” said Jeff Price, president of the Milliken Performance and Protective Textiles Division. “Milliken innovations speak for themselves, and this website helps convey our story and fortify our reputation in a cohesive online platform.”
Taming Complexity
Previously, exploring the vast array of textiles available through the division presented challenges because of the sheer number of textiles available. Now, using the new website, customers can navigate through the portfolio by choosing market or by searching key performance characteristics to find solutions that best fit their needs. The advanced search page lists the eight markets served by Milliken’s Performance and Protective Textiles division and 28 key fabric properties.
As an example, if a customer were searching for fabrics with moisture wicking or antimicrobial characteristics, 10 search results are returned. Among the results are Biosmart® Technology — a patented technology engineered to bind chlorine in wash water to the surface of a fabric to inhibit the growth and spread of bacteria — and ResQ™ DH — a National Fire Protection Association certified fabric enhanced with moisture wicking properties and high breathability to keep firefighters cool and comfortable.
“Milliken’s Performance and Protective Textiles website displays the value of Milliken front and center,” Price said. “We are enhancing our world through well-thought-out products, crafted to fill a need and manufactured responsibly.”
Milliken designs fabrics for performance, but also takes environmental responsibility into consideration intentionally incorporating sustainable measures from product conception to production. The company continually assesses its net impacts, seeks greater efficiencies and develops new technologies to avoid using harmful materials. Many of Milliken’s manufacturing facilities also have obtained ISO 14001 certification — the highest global standard for environmental responsibility. Company records also document its first recycling policy and the fact that it was reusing packaging and textile materials in its operations in the early 1900s. With one of the most ambitious environmental policies in the industry today, sustainability truly is and always has been an important part of the company and everything it does.
In addition, Milliken has the honor of being named one of the “World’s Most Ethical Companies” for 12 years running. The list, published by Ethisphere Magazine, is compiled by the Ethisphere Institute, a leader in defining and advancing the standards of ethical business practice. Milliken is one of only 12 companies to receive the honor every year since its inception.
With new tools in hand, Milliken’s diverse textiles portfolio, built on more than 150-years of industry experience and award-winning research and development, has never been more accessible to customers looking to solve challenges using innovative fabrics. “Our keen attention to detail and unsurpassed quality result in superior textiles that add value to people’s lives,” Price said.
Editor’s Note: This article appears in Textile World courtesy of the National Council of Textile Organizations (NCTO) as part of the “American Textiles: We Make Amazing™” campaign. NCTO is a trade association representing U.S. textile manufacturing. Please visit ncto.org to learn more about NCTO, the industry and the campaign.
Marty Moran, Chairman, National Council of Textile Organizations, and CEO, Buhler Quality Yarns Corp. (a Samil Spinning Co.)
Why NCTO matters more than ever.
TW Special Report
The U.S. textile industry is experiencing an exciting and dynamic period. A new policy environment has evolved in Washington that places a greater emphasis on domestic manufacturing. Combined with a desire for shortening production and sourcing cycles, investment in U.S. textile production capacity, including foreign direct investment, has been invigorated, as many look to our shores to grow their capacities.
I have seen this investment story firsthand. The company for which I have the privilege of serving as CEO, Buhler Quality Yarns, was launched in 1996 by Hermann Bühler AG, a Switzerland-based textile manufacturer originally founded in 1812. This 200-plus-year-history added a fresh chapter when it was purchased by Korea-based Samil Spinning. Our new ownership represents a sea-change — Samil Spinning has invested in Buhler Quality Yarns for growth — they see clear benefits and great potential in Western Hemisphere production.
This is not just a single data point to exemplify a trend. Consider a recently published McKinsey study1 demonstrating that apparel manufacturing is returning to our hemisphere in a way thought impossible only a few short years ago. Retail, in almost all sectors, stresses the need for speed-to-market manufacturing processes, underscoring the need for optimized and more local supply chains.
A Brave New World
Opportunity is potential, and potential is full of as much uncertainty as it is excitement. Let’s make no mistake — we are in uncharted territory. Growth is certainly welcome news, but prosperity can often be guided by nearsighted intentions, causing us to be the architects of unintended consequences further down the road.
This is why our industry needs the National Council of Textile Organizations (NCTO) now more than ever. Our core mission, to “preserve and enable the prosperous future of U.S. textile manufacturing,” is being put to the test under new light.
Consider the uncertainty of a potential trade war with China. The U.S. Government recently placed duties on many products under 301 Authority.2 This position has touched many products in the supply chain, affecting many textile companies — some positively, some negatively. Navigating these new constructs, and anticipating next moves by both countries, has become a significant challenge not just for textile companies, but for brands and retailers as well.
In addition, the Trump administration has renegotiated the North American Free Trade Agreement (NAFTA), America’s regional free trade agreement with Canada and Mexico. Since U.S. textile exports to the combined Mexican and Canadian markets totaled nearly $12 billion in 2017, it is critical that any transition to the U.S.-Canada-Mexico Agreement (USMCA) be smooth for all parties.
How The U.S. Factors
Many brands and retailers are now faced with the decision to either maintain their current sourcing strategies, or adopt — or in many cases, create — new strategies that feature Western Hemisphere sourcing.
Trade challenges factor heavily, but it is also critical for brands and retailers to recognize the need to contract sourcing lead times and to avoid supply disruption.
David Sasso — vice president of Sales at Buhler Quality Yarns, and a veteran expert in textile supply chains — has made a very strong argument for Western Hemisphere sourcing in two recent articles. In “Responsive Retail”3 and “What TPP’s Death Means for U.S. Apparel Brands and Supply Chain Management in Uncertain Times”4 he argues that, because of the trend-based, mercurial nature of the fashion industry, it is important to be able to react quickly. Shotgun approaches to fashion can cause two major issues. First, when an item is ordered in large quantity and sales don’t meet expectations, the result is markdowns and lost revenue. A second possible negative outcome is when an item sells in far greater quantities than anticipated. Supply chains dependent on overseas sources, and shipping constraints often lead to stockouts, leaving profits on the table and customers looking elsewhere for similar styles.
A brand’s sourcing strategy that moves at least a portion of its sourcing chain to the Western Hemisphere reduces lead times, solving both issues. A Western Hemisphere supply chain holds net-positive potential for brands, retailers, and consumers alike.
“The United States and our partners in the Western Hemisphere supply chain are making investments to better serve brands and retailers — and ultimately, consumers. Strategic business partnerships are important, but they must also be combined with a strong voice in Washington to ensure that the investments and relationships are allowed to prosper.”
— Marty Moran, Chairman, National Council of Textile Organizations, and CEO, Buhler Quality Yarns Corp. (a Samil Spinning Co.)
The Task At Hand
The United States and our partners in the Western Hemisphere supply chain are making investments to better serve brands and retailers — and ultimately, consumers. Strategic business partnerships are important, but they must also be combined with a strong voice in Washington to ensure that the investments and relationships are allowed to prosper. This is a strategy that must be recognized and championed — and that is exactly why NCTO exists.
We must ensure that those working to craft trade and procurement policies hear our voice, understand our challenges, foresee those policy decisions that may have net-negative consequences for our industry, and enact policy engineered to further our interests. Governmental policy makers are not textile supply chain experts who live and breathe this industry. We are, and thus only we, as a united industry, can communicate our interests.
I am proud to serve this industry as chairman of the NCTO, and proud to work with and on behalf of all of our members.
The opportunity is ours to seize. It is a truly exciting time to be in American textiles.
Editor’s Notes: NCTO Chairman Marty Moran has been part of U.S. textile manufacturing for more than 26 years. A native of North Carolina, he serves as CEO of Jefferson, Ga.-based Buhler Quality Yarns Corp. (a Samil Spinning Co.). Buhler is known not only for its high-quality yarn spinning, but also for its deep supply chain expertise, placing Moran at the center of this complex and ever-shifting industry.
This article appears in Textile World courtesy of the National Council of Textile Organizations (NCTO) as part of the “American Textiles: We Make Amazing™” campaign. NCTO is a trade association representing U.S. textile manufacturing. Please visit ncto.org to learn more about NCTO, the industry and the campaign.
Stefan Flöth was named a managing director of Germany-based A. Monforts Textilmaschinen GmbH & Co. KG effective January 1, 2019.
John Sobchak was appointed to the newly created position of CFO for Gelest Inc., Morrisville, Pa.
Aurora Specialty Textiles has named Erik Nees sales account manager where he will oversee industrial sales including tape, bedding, medical and technical textiles applications.
Downlite, Mason, Ohio, has named Lisa Pruett chief sales and marketing officer.
Katia Walsh was named chief strategy and artificial intelligence officer for San Francisco-based Levi Strauss & Co.
Atlanta-based brrr° recently added Molly Kremidas and Valentina Henao to its sales team.
Switzerland-based SSM Schärer Schweiter Mettler AG has named Roman Haefeli head of sales.
Ketty Pillet has joined Gerber Technology, Tolland, Conn., as vice president of global marketing.
Austria-based The Lenzing Group has named Jürgen Eizinger vice president of Global Business Management nonwovens division effective March 1, 2019. His focus will be on creating awareness for the VEOCEL™ sustainable brand, as well as leading the development and implementation of various business strategies.
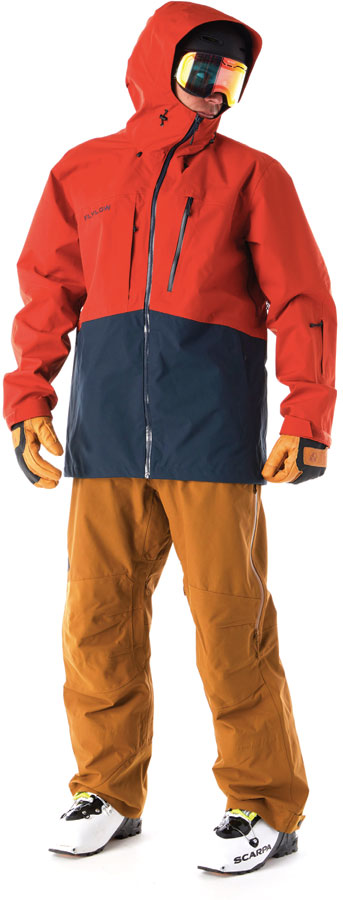
Flylow Gear’s men’s Quantum Pro Jacket and Chemical Pant are treated with Bolger and O’Hearn’s OmniBloq™ DWR for high performance in demanding conditions.
Bolger & O’Hearn’s OmniBloq™ was engineered to keep apparel dry and consumers comfortable even in pounding rain and squall conditions.
By Rachael S. Davis, Executive Editor
Fall River, Mass.-based Bolger & O’Hearn recently introduced a new type of durable water repellent (DWR) to the market called Stormproof/ Breathable™ OmniBloq™. The company reports OmniBloq is an “ideal DWR in even the harshest snow storms, rain and squalls,” and has been engineered to deflect heavy, wind-driven rain and provide laminate-like rain resistance when applied to a single-ply, woven man-made fabric. OmniBloq also maintains a fabric’s breathability without compromising fabric hand or wearer comfort.
“Single-ply fabrics having specific woven constructions can be finished with OmniBloq and will retain the original fabric’s air permeability and moisture vapor transmission rate, while providing excellent water holdout in addition to the outstanding resistance to soaking in extreme rain exposure,” said Shawn Honeycutt, sales manager.
According to Bolger & O’Hearn, typical DWR finishes deposit a semi-organized layer of coating onto the textile fiber, which provides enough of a barrier to resist gentle water spray and other contaminants. However, this disorganized finish arrangement reduces long-term durability and makes the fabric vulnerable to high-impact rain and snow.
What sets OmniBloq apart from typical DWRs is that the chemistry forms a highly ordered layer on the textile fiber that is strongly repellent. This near-perfect organization of the OmniBloq coating also ensures it remains adhered to the fiber over time, so the fabric maintains its ultra-repellency in adverse environmental conditions even after repeated laundering. “Fabrics based on man-made fibers such as polyester, nylon and blends with spandex can be home laundered more than 30 times and still retain outstanding storm-resistant properties,” Honeycutt said.
The chemistry is a bluesign-approved, non-perfluorooctanoic acid (PFOA) technology that also provides protection against oils and stains. OmniBloq is suitable for application on single-ply fabric constructions, but can “super charge” laminated waterproof/breathable fabric constructions as well,” Honeycutt said.
Fabrics treated with OmniBloq pass the American Association of Textile Chemists and Colorists’ (AATCC’s) Rain Test 35-2013; resist wetting out anywhere from three to 20 times longer than the same fabric treated with a traditional DWR; and also maintain the highest rating on the Bundesmann water repellency test after more than 30 minutes of exposure to impact equivalent to full force rain, according to the company.
OmniBloq is suitable for all types of performance apparel and gear, as well as boat and car covers, military uniforms and soft goods, footwear, and awnings.
Denver-based outerwear and apparel company Flylow Gear recently adopted OmniBloq DWR introducing four of its best-selling winter designs treated with the finish at the recent Outdoor Retailer + Snow Show — the Quantum Pro Jacket and Chemical Pant for men; and the Billie Coat and Nina Pant for women.
“We’re stoked to be the first winter sport brand to use OmniBloq DWR, and we specifically chose to use it on pieces that are favorites of some of the hardest skiing men and women on the mountain” said Dan Abrams, president, Flylow Gear.
For more information about Stormproof/Breathable™ OmniBloq™ DWR, contact Shawn Honeycutt shoneycutt@bolgerohearn.com; omnibloq.com
BIRMINGHAM, Ala. — March 22, 2019 — Hibbett Sports Inc., an athletic specialty retailer, today announced the planned retirement of Jeff Rosenthal, president and CEO. The Board will commence a search process to identify the company’s next CEO, and Rosenthal will remain at the company in his CEO capacity until a successor is named. He will assist the Board with the search and the execution of the transition. Upon the completion of the leadership transition, Rosenthal will continue to serve as a member of the Board of Directors.
Commenting on Rosenthal’s decision, Mickey Newsome, chairman of the Board, stated, “We are fortunate to be able to have a seamless transition of leadership at Hibbett Sports. Jeff has served Hibbett for over 21 years and has contributed significantly to its growth. He has worked tirelessly over the past several years leading the company in a very difficult retail environment. He has created a foundation for the company’s success as we move forward, and we thank him.”
“I have been privileged to lead Hibbett Sports over the past nine years as president and CEO,” Rosenthal stated. “I am proud of our accomplishments during that time having built a world class e-commerce website and most recently completing our first significant acquisition. I believe that the Company is well positioned, and it is an appropriate time to begin a transition. I am committed to working with the management team in a smooth transition and subsequently working alongside my Board peers.”