Colorado’s Hospital Cooperative Laundry Achieves Renewal For Hygienically Clean Healthcare

ALEXANDRIA, Va. — January 15, 2021 — Hospital Cooperative Laundry (HCL), with locations in Pueblo and Denver, Colo., has recently qualified for renewal of the Hygienically Clean Healthcare certification. The recertification reflects its continued commitment to best management practices (BMPs) in laundering as verified by on-site inspection and its capability to produce hygienically clean textiles as quantified by ongoing microbial testing. HCL provides laundry processing, pack room services and hospital linen distribution services to its owner member hospitals, serving more than 40 hospitals and clinics throughout the greater Denver and southern Colorado areas.

The Hygienically Clean Healthcare certification confirms the organization’s continuing dedication to infection prevention, compliance with recognized industry standards and processing healthcare textiles using BMPs as described in its quality assurance documentation, a focal point for Hygienically Clean inspectors’ evaluation. The independent, third-party inspection must also confirm essential evidence that:

  • Employees are properly trained and protected;
  • Managers understand regulatory requirements;
  • OSHA-compliant; and
  • Physical plant operates effectively.

To achieve certification initially, laundries pass three rounds of outcome-based microbial testing, indicating that their processes are producing Hygienically Clean Healthcare textiles and diminished presence of yeast, mold and harmful bacteria. They also must pass a facility inspection. To maintain their certification, they must pass quarterly testing to ensure that as laundry conditions change, such as water quality, textile fabric composition and wash chemistry, laundered product quality is consistently maintained. Re-inspection occurs every two to three years.

This process eliminates subjectivity by focusing on outcomes and results that verify textiles cleaned in these facilities meet appropriate hygienically clean standards and BMPs for hospitals, surgery centers, medical offices, nursing homes and other medical facilities.

Hygienically Clean Healthcare certification acknowledges laundries’ effectiveness in protecting healthcare operations by verifying quality control procedures in linen, uniform and facility services operations related to the handling of textiles containing blood and other potentially infectious materials.

Certified laundries use processes, chemicals and BMPs acknowledged by the federal Centers for Disease Control and Prevention (CDC), Centers for Medicare and Medicaid Services, Association for the Advancement of Medical Instrumentation, American National Standards Institute and others. Introduced in 2012, Hygienically Clean Healthcare brought to North America the international cleanliness standards for healthcare linens and garments used worldwide by the Certification Association for Professional Textile Services and the European Committee for Standardization.

Objective experts in epidemiology, infection control, nursing and other healthcare professions work with Hygienically Clean launderers to ensure the certification continues to enforce the highest standards for producing clean healthcare textiles.

“Congratulations to Hospital Cooperative Laundry on their recertification,” said Joseph Ricci, TRSA president and CEO. “This achievement proves their commitment to infection prevention and that their laundry takes every step possible to prevent human illness.”

Posted January 15, 2021

Source: TRSA

Borealis And TOMRA Open State-Of-The-Art Plant For Post-Consumer Plastic Waste Sorting And Advanced Mechanical Recycling

VIENNA, Austria— January 14, 2021 — Borealis and TOMRA have today announced the operational start of their advanced mechanical recycling demo plant in Lahnstein, Germany, the result of a partnership that marries chemistry with technology for unsurpassed results.

“This plant embodies the principles of the EverMinds™ platform founded by Borealis, which seeks to innovate plastics circularity through collaboration,” says Lucrèce Foufopoulos, Borealis Executive Vice President Polyolefins, Innovation & Technology and Circular Economy Solutions. “Offering brand owners and converters top quality recycled material, suitable for use in highly demanding applications is Borealis’ latest contribution to a more circular economy of plastics. Life demands progress, and through collaboration we re-invent for more sustainable living.”

The state-of-the-art plant processes both rigid and flexible plastic waste from households. And unlike many current recycling plants, it will produce the advanced solutions necessary for use in high-demanding plastic applications in various industries, including automotive and consumer products. With high purity, low odour, high product consistency and light colour fractions, these Borcycle™ M grade recycled polymers will meet customer quality requirements across the value chain.

The purpose of this demo plant is to generate material for brand owners and converters to qualify, validate and prove fit for use in their highly demanding applications. Technical success will set the groundwork for a commercial-scale advanced recycling plant.

“This plant is just the beginning of what’s possible when key players in the value chain come together to make a truly significant impact in the market,” says Volker Rehrmann, Executive Vice President and Head of Circular Economy at TOMRA. “Having just launched the new Circular Economy Division, it is clear what a large role waste management and pivotal projects like this have on moving towards a sustainable future. We are proud to have initiated one of the most advanced mechanical recycling plants when it comes to post-consumer polymer waste. This will become an important enabler as we accelerate the transformation to a circular economy in the years to come, and we are excited to be a part of this pioneering project.”

Operation of the plant is a joint enterprise between Borealis, TOMRA and Zimmerman. Borealis is responsible for the plant’s commercial success and contributes its expertise and knowledge in innovation, recycling and compounding. Likewise, TOMRA contributes as a provider of technology-led solutions and brings its proven expertise, established process and market knowledge, which, in turn, enable the circular economy through advanced collection and sorting systems. Zimmerman is a waste management company with experience in sorting multiple types of waste, including plastics, and is responsible for successful plant operations and product quality.

“At P&G we are making packaging with the ‘next life’ in mind to help drive a more robust circular economy.  We must increase the supply of high quality recycled plastic to enable the industry to deliver on this vision,” says Gian De Belder, Procter & Gamble (P&G) Technical Director, R&D Packaging Sustainability. “The innovative new approach that Borealis is taking shows potential to step-change both the quantity and quality of PCR available for our brands, and help us to achieve our 2030 goal to reduce our use of virgin plastic in packaging by 50%, or 300 kilotonnes annually. Early tests of the material looks very promising!”

“One major challenge towards more circular packaging is the availability of high-quality recycled plastics that can be used in the packaging of our brands,” comments Thorsten Leopold, Director International Packaging Technology Home Care at Henkel. “We are, therefore, very excited that this project brings together three proven experts along the value chain with the ambition to lift mechanical recycling to a new level.”

Posted January 15, 2021

Source: Borealis & TOMRA

Arizona-Based Apparel Partnership Reaches Manufacturing Milestone; 500,000 Reusable Isolation Gowns Produced For Healthcare Workers During Pandemic

TEMPE, Ariz. — January 14, 2021 — The Fashion and Business Resource Innovation Center (FABRIC) announced today that partners operating within its facility during the pandemic have collaborated to make 500,000 FDA-approved, reusable, level 2 and 3 isolation gowns for medical professionals.

AZ Fashion Source, Falcon Engineering, Wulff Contracting, On Point Manufacturing and Katchina Apparel Manufacturing collaborated with FABRIC to produce the American-made and reusable isolation gowns, which can be worn and washed 100 times.

“With 500,000 gowns produced to date, the reusable gowns have kept 50,000,000 disposable gowns out of landfills,” said Sherri Barry of AZ Fashion Source and co-founder of FABRIC. “The gowns have also helped keep costs down for healthcare providers of all sizes, with a price-per-wash that is lower than a disposable gown.”

FABRIC, a public social cooperative enterprise that works with private industry, local government and nonprofits to support apparel entrepreneurs, pivoted quickly when the pandemic hit the U.S. in March. Local donors, including the Flinn Foundation, Virginia G. Piper, Charitable Trust, Pakis Center for Business Philanthropy, Tempe Innovation Development Association, Thunderbirds Charities, BHHS Legacy Foundation, Silicon Valley Bank, PCA Skin, AZ Community Foundation, and AZ Bio, supported the effort to transform FABRIC’s space into a manufacturing hub for PPE when pandemic-related shortages were widespread.

The ramped-up manufacturing efforts also provided hundreds of essential manufacturing jobs, and garnered a visit from President Elect Joe Biden and Vice President Elect Kamala Harris during their October visit to Arizona.

Proceeds from the gown sales made by AZ Fashion Source have been donated back to FABRIC Tempe. This new nonprofit aims to support apparel entrepreneurs with equipment, training, guidance, industry resources and access to no-minimum manufacturing.

Angela Johnson, a co-founder of FABRIC and FABRIC Tempe, says that with the manufacturing pivot, there is now even more opportunity to help meet the mission.

“Because of our generous donors, we believe that FABRIC Tempe will help establish Arizona as a modern fashion industry capital,” says Johnson. “Leveraging a technology-based, sustainable, closed loop ecosystem that attracts and supports direct-to-consumer apparel brands, apparel entrepreneurs will have incredible opportunities to create, manufacture and grow their dreams.”

Posted January 15, 2021

Source: FABRIC Tempe

VDMA: Webtalk On Material Efficiency And Fiber Recycling In Textile Spinning

FRANKFURT — January 15, 2021 — The first VDMA technology webtalk in 2021 is scheduled for January 21, from 2-4 p.m. (CET). The topic will be “Material efficiency and fiber recycling in textile spinning: Approaches for circular economy”.

The experts will give an overview of the recycling processes that can turn old clothes into high-quality yarns and fabrics.

The presenters and their topics at a glance:

Dr. Bettina Temath, Truetzschler Group will demonstrate how production waste from spinning preparation can be recycled. She will also present solutions to process recycled fibers made from postconsumer textile waste and explain how the best possible quality can be achieved.

Title of the presentation: “From waste to value: Recycling processes in spinning preparation”

www.truetzschler.com

René Bucken, Saurer Group: “The use of regenerated fibers increases the share of short fibers in the sliver which tends to decrease spinning mill efficiency. Saurer offers solutions for different materials and fiber compositions in order to optimize spinning for all kinds of fibers.”

Title of the presentation: “Efficiency in spinning regenerated fibre”

www.saurer.com/en

Michael Wolf, imat-uve imat will show, using a specific project as an example, how high-quality yarns can be developed and produced from old clothing using blended fibers.

Title of the presentation:“New life for old clothes – Mixed fibre recycling for high demands”

www.imat-uve.de

After the presentations, the three experts will be available to answer the participants’ questions.

Registration is possible via this link (no participation fee):

https://register.gotowebinar.com/register/6986770085191034892

Posted January 15, 2021

Source: VDMA

Polyfab USA Announces New Parasol™ Color Additions For 2021

MANHATTAN BEACH, Calif. — January 13, 2021 — Polyfab USA is pleased to announce that they have added 4 new shades to the color range of Parasol™ Commercial Grade Economy Shadecloth, giving the range a total of 19 colors.

Parasol is a commercial grade knitted shadecloth for tension structures and other heavy-duty applications. It is manufactured using a combination of high-density monofilament and tape which offers a higher degree of protection from UV radiation, known to cause sunburn and skin cancers.

For ease of fabrication and improved performance, Parasol shadecloth has been “heat-set” before rolling, to improve lay-flat characteristics and dimensional stability. Parasol is designed for Australian conditions and made to stringent quality and manufacturing specifications. It is available from a number of Polyfab USA distributors throughout the Americas.

Parasol™ is 9.6 oz. per square yard/325 gsm and 9.8 feet/3.0 meters/118 inches wide. It is a premium product at an economy price! Fabricators can contact their local distributor for more information.

Posted January 15, 2021

Source: POLYFAB USA LLC

Hologenix, Kelheim Fibres Launch Celliant Viscose

KELHEIM, Germany — January 14, 2021 — Hologenix, creators of Celliant®, infrared responsive technology, and Kelheim Fibres, manufacturer of viscose specialty fibers, have partnered to launch Celliant Viscose at ISPO Munich 2021. Celliant Viscose is a finalist in Best Products by ISPO and will be showcased in the Fibers & Insulations Category for ISPO Textrends, where realistic views and 3-D simulations will be available for each material.

The introduction of nature-based Celliant Viscose will be the first in-fiber infrared sustainable solution on the market and meets a consumer demand for more environmentally friendly textiles. An alternative to synthetic fibers and extremely versatile, Celliant Viscose blends beautifully with cotton, micromodal, lyocell, wool varieties including cashmere. It also has many applications across industries as it is ideal for performance wear, luxury loungewear, casual wear and bedding.

Celliant Viscose features natural, ethically sourced minerals embedded into plant-based fibers to create infrared products that capture and convert body heat into infrared, increasing local circulation and improved cellular oxygenation. This results in stronger performance, faster recovery and better sleep.

“We are confident the exciting introduction of Celliant Viscose will resonate strongly with brands as well as the end consumer,” said Seth Casden, Hologenix Co-Founder and CEO. “It is a sustainable infrared solution that can be integrated into everything from cotton to luxury wools and cashmere and offers myriad applications.”

Celliant Viscose provides all the benefits of being a viscose fiber — lightweight, soft, highly breathable, excellent moisture management — as well as fiber enhancements from Celliant infrared technology. Celliant’s proprietary blend of natural minerals allows textiles to capture and convert body heat into full- spectrum infrared energy, resulting in stronger performance, faster recovery and better sleep. In addition, Celliant is durable and will not wash out, lasting the useful life of the product it powers.

“Sustainable products for a healthy lifestyle and wellbeing — that’s what both Hologenix and Kelheim Fibres stand for. This shared vision of the future is the sound basis for our seamless cooperation,” said Dr. Marina Crnoja-Cosic, head of New Business Development and Member of the Board at Kelheim Fibres. “Combining our technological expertise and our innovative spirit, we have opened the way for an entirely new range of possible applications.”

An Affordable, Long-lasting Solution With Diverse Applications

As opposed to other IR viscose products which are coatings based, Celliant Viscose’s in-fiber solution increases wearability and longevity with a soft feel, durability from washing and longer life. The combination of Kelheim’s distinctive technology and the Celliant additives creates this unique fiber that provides full functionality without the need for any additional processing step — a new standard in the field of sustainable IR viscose fibers. This single processing also makes Celliant Viscose more cost-effective and time-efficient than coatings.

In addition, Kelheim’s flexible technology allows targeted interventions in the viscose fiber process. By modifying the fiber’s dimensions or cross sections or by incorporating additives into the fiber matrix, Kelheim can precisely define the fiber’s properties according to the specific needs of the end product.

Highly Sustainable

Celliant Viscose is a plant and mineral-based solution for brands seeking an alternative to synthetic fibers. It contains natural raw materials that are from the earth and can return safely to the earth.

Nature-based Celliant Viscose is certified by FSC® or PEFCTM, which guarantees the origin in sustainably managed plantations, and is part of the CanopyStyle initiative to protect ancient and endangered forests. The production of Celliant Viscose takes place exclusively at the Kelheim facilities in Germany, complying with the country’s strict environmental laws and guaranteeing an overall eco-friendly product.

Backed by Science

Celliant is rigorously tested by a Science Advisory Board composed of experts in the fields of physics, biology, chemistry and medicine. The Science Advisory Board has overseen 10 clinical, technical and physical trials, and seven published studies that demonstrate Celliant’s effectiveness and the benefits of infrared energy.

Posted January 14, 2021

Source: Kelheim Fibres GmbH

No Sustainability Without Innovation – True To This Motto, TINTEX And BRÜCKNER Strive For New Paths Together

LEONBERG, Germany — January 14, 2021 — The Portuguese textile company TINTEX Textiles S.A. and the German textile machinery manufacturer BRÜCKNER Textile Technologies GmbH & Co. KG make a big step into the future together. A completely new developed process technology for coating bi-elastic knitted fabric opens new markets and new possibilities for both sides.

The modern textile company TINTEX is located in Villa Nova, not far from the Spanish border in northern Portugal. The company was founded in 1998 in the region of Porto. The product range includes functional tricot fabrics for well-known fashion, sports and lingerie brands. TINTEX is convinced that fashion can truly make a difference in tackling climate change. That is why their engineers are constantly developing new strategies and environmentally friendly concepts throughout the whole production process. The technologists’ expertise covers the entire textile supply chain, including dyeing and finishing techniques as well as coatings.

“No sustainability without innovation“

True to this motto, TINTEX is constantly researching for fabric innovations to develop and produce intelligent, functional and high-performance textiles. To round off the concept, a few years ago it was decided to cooperate with the German textile machinery manufacturer BRÜCKNER. Their product range includes machines and complete lines for coating and finishing of textiles, technical textiles, nonwovens and floor coverings. With their own production site in the south of Germany, completely rebuilt in 2018, BRÜCKNER has become even more flexible and competitive. The family-run company was founded in 1949 and is today managed in the second generation by Regina Brückner and her husband Axel Pieper. Still valid today, the values and visions of the company founder are the key to success: the production of high-quality lines, the development of sustainable and innovative technologies and the competent and comprehensive advice of their customers.

Since both companies, TINTEX and BRÜCKNER, share the same philosophy, the basis for constructive and goal-oriented product development was quickly established. The vision of TINTEX was to be able to achieve completely new effects on bi-elastic knitwear and to produce fabrics that did not even exist before. This was followed by numerous tests in the Technology Centre at BRÜCKNER in Leonberg and on a BRÜCKNER line in an institute for textile and process engineering near Stuttgart. So a new, revolutionary line concept was worked out together, which has unbeatable benefits especially with regard to the requirements of temperature uniformity, the thermal treatment of synthetic fibre blends and other constructive issues. Even very difficult knitted fabric with high elastane content can now be directly coated or functionalized. Until now, such coatings were only possible in an indirect coating process.

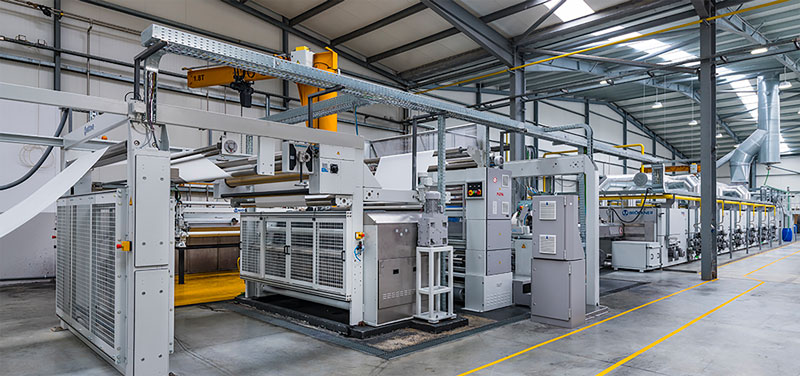
The heart of the new line is the proven, but constantly further developed and optimized POWER-FRAME stenter frame dryer. The inlet and outlet components are specially designed for sensitive fabric and ensure a tensionless fabric run. A special, newly developed coating unit is integrated in the infeed stand of the stenter frame. Due to its variable design, two different application processes are possible on the same line. In the so-called screen coating process, water-based pastes and stable or unstable foams are applied onto the fabric with high precision by means of a driven, cylindrical screen and a squeegee system integrated in the screen.

For paste coating, the machine parameters can be adjusted in such a way that a single-side coating is possible even on light knitwear made of cotton or viscose, provided the paste is of a suitable viscosity. For the stable foam coating, the coating medium is mixed to foam with an exact foam/liter weight of 150 to 300 g/l. With an integrated feed pump, this foam can be precisely dosed and applied to the textile through the screen. Also in the case of unstable foam coating, the coating medium is foamed up with a mixer and applied to the textile in exact doses. Here the foam/liter weight is 30 to 100 g/l.

As the unstable foam collapses shortly after leaving the screen, a single-side functionalization with a very low pick-up of less than 10 to 20 percent can be achieved. This is a minimum application with the corresponding benefits, e.g. considerable energy and thus cost savings in the subsequent drying process. If you want to coat somewhat more stable fabric or apply higher coating weights, the unit can be quickly and easily converted from screen coating to a knife-over-cylinder system. The counter pressure roller is then used as coating cylinder.

A laminating/embossing calender integrated in the outfeed of the tenter allows various effects to be achieved on the fabric, e.g. a leather grain. If the applied stable foam coating has a certain layer thickness, this effect can be achieved after the drying passage in the laminating calender by means of a fed release paper or an appropriate embossing roller. Even with sensitive, directly coated knitted fabric, this calender can be used to apply e.g. a film, a membrane or a second textile web onto the fabric. For this purpose, the calender is additionally equipped with an electric short-wave infrared dryer.

For simple heat-setting processes a special roller has been developed which can be inserted into the coating unit instead of the screen and thus acts as the upper infeed roller. Even very tension-sensitive knitwear can be run with an overfeed of up to 60 percent before heat-setting.

This new multifunctional line can therefore be used for heat-setting, drying and coating processes. It can be used to manufacture products comparable to those previously produced with indirect coating — but without having to rely on cost-intensive release paper. At TINTEX in Portugal, production on this line has already been running for some time and research into completely new types of textiles is continuing. At Munich Fabric Start, TINTEX even won the Hightex Award with such newly developed products, as well as the Innovation Award at Techtextil in Frankfurt.

BRÜCKNER is very proud to have customers like TINTEX who act with foresight and do not strive for short-term profit optimization. The goal is always to think and act with a long-term perspective, because this is the only way how BRÜCKNER and their customers can be successful in the long run.

Posted January 14, 2021

Source: BRÜCKNER Textile Technologies GmbH & Co.

Glen Raven Expands On Industry-Leading Warranty For Sunbrella® Fabrics

BURLINGTON, N.C. — January 14, 2021 — Glen Raven Custom Fabrics announces an enhanced warranty for Sunbrella® fabrics to include replacement labor costs in all categories, including residential and commercial upholstery, shade and marine applications in the rare instances when replacement fabric may be needed.

With the inclusion of replacement costs, Sunbrella fabrics are backed by the most comprehensive warranties in the industry. Sunbrella is currently the only performance fabric brand to guarantee against loss of color and strength, plus pilling and abrasion, with a five-year limited warranty for upholstery fabrics that now includes labor coverage for the first three years in addition to fabric replacement. The brand’s shade and marine fabrics hold an industry-leading 10-year limited warranty with labor costs covered for the first five years.

“For 60 years, Sunbrella fabrics have set the standard for industry-leading performance with fabrics designed for countless applications,” said Dave Swers, president of Glen Raven Custom Fabrics. “Our proven expertise and proprietary technologies allow us to demonstrate our commitment to quality by expanding our industry-leading guarantee and support to collectively benefit our retailers, manufacturers, fabricators and consumers. This gives our partners and end users even more confidence to purchase and apply Sunbrella fabrics to sofas, casual furniture, awnings or boats knowing that Sunbrella stands behind its products and its customers.”

Posted January 14, 2021

Source: Glen Raven Custom Fabrics

U.S. Cotton Trust Protocol Welcomes First Members In Latin America

MEMPHIS, Tenn. — January 14, 2021 — Today the U.S. Cotton Trust Protocol welcomed its first Latin America-based members: Central America Spinning Works El Salvador, Cone Mills, Colhilados, Fabricato, Gama Textil, Global Textiles, Grupo Industrial Miro, Grupo Vivatex, Hilanderia de Algodon Peruano, Honduras Spinning Mills, Industrias Cannon de Colombia, Industrias Merlet, Industria Textil del Pacifico, Junior de Mexico (OGGI Jeans), Manufacturas Kaltex, MT Textiles, OA, Playeras Mark, Premium Knits, Quality Knits, Ropa Siete Leguas, SJ Jersey Ecuatoriano, Tavex, Textufil, Textiles Marie Lou, Textil del Valle, WT Sourcing and Zagis. Among other benefits, membership enables these mills and manufacturers to prove that the cotton fiber element in their textiles is more sustainably grown.

“We are pleased that these companies have joined the Trust Protocol as the textile industry works to improve the transparency in their supply chain that brands and retailers are asking for,” said Dr. Gary Adams, president of the U.S. Cotton Trust Protocol. “The Trust Protocol is providing verified, reliable data about cotton growers’ responsible growing practices in six key areas — water use, greenhouse gas emissions, energy use, soil carbon, soil loss and land use efficiency — and shows how sustainability is constantly improving through the entire supply chain.”

Mills and manufacturers who become members have access to the Trust Protocol credit system to validate consumption of cotton and associated credits. The combination of a unique credit accounting system and the Permanent Bale Identification (PBI) system enables brands to have transparency throughout the supply chain to finished product.

In December 2020, the Trust Protocol also announced the membership of Gap Inc. as part of their integrated sustainability strategy and to help achieve their commitment to use only 100% sustainably-sourced cotton by 2025. December also saw the announcement of the first 10 U.S. mills to join the Trust Protocol: Buhler Quality Yarns, Cap Yarns, CCW, Contempora Fabrics, Cotswold Industries Inc., Frontier Yarns, Hamrick Mills, Inman Mills, Parkdale Inc. and Swisstex Direct.

The Trust Protocol has been invited to join Cotton 2040 and its CottonUp guide and is also on the Textile Exchange’s list of 36 preferred fibers and materials that more than 170 participating brands and retailers can select from as part of Textile Exchange’s Material Change Index program.

Posted January 14, 2021

Source: U.S. Cotton Trust Protocol

Davlyn Group Appoints Vice President And General Manager: Stephen Tang To Manage The Company’s Norfab-Amatex Division

SPRING CITY, Pa. — January 13, 2021 — Davlyn Group, a portfolio company of Emko Capital, has announced that Stephen Tang has joined the company as vice president and general manager, Norfab-Amatex.

Stephen was most recently with ITW, where he was the Industrial Business Unit Manager for Brooks Instruments. Prior to ITW, he held several general management and engineering roles at Micross Components and Kulicke and Soffa, including an expat role in Switzerland.

“Stephen’s experience working across a range of small and large companies, combined with capabilities in areas such as lean and ITW’s 80/20 process, make him a great fit for leading our recently acquired Norfab-Amatex business,” said Mauricio Zavatti, Davlyn Group CEO. “I also want to recognize John and Tom Weber, Dick Howard, and the rest of the Norfab-Amatex leadership team for all of their support during our integration process, and look forward to the company’s next phase of growth.”

“I am excited to join Davlyn Group’s leadership team,” commented Tang. “Norfab-Amatex’s customer-centric culture, best-in-class manufacturing capabilities, and history of innovation within the thermal protection and personal protective equipment (PPE) segments provide a solid foundation for growth.”

Stephen holds a BS in Materials Science and Engineering from Cornell and an MBA from Columbia University.

Posted January 13, 2021

Source: Davlyn Group

Sponsors