Wrangler: Proudly Naming Names In Jeans, T-Shirt Supply Chain

(left): The Wrangler Rooted Collection™  features five state-specific pairs of jeans — the Alabama Jean, the Georgia Jean, the North Carolina Jean, the Tennessee Jean and the Texas Jean
The Wrangler Rooted Collection™ features five state-specific pairs of jeans — the Alabama Jean, the Georgia Jean, the North Carolina Jean, the Tennessee Jean and the Texas Jean

Wrangler recently announced The Wrangler Rooted Collection™, a jeans and T-shirt program featuring cotton garments grown, milled, cut and sewn in the United States.

TW Special Report

For more than 70 years, Greensboro, N.C.-based Wrangler® has been committed to bringing consumers authentic American style through its apparel collections for men, women and children in jeanswear and casualwear. Recently however, the company has taken “Authentic American” a step further as it introduced The Wrangler Rooted Collection™. Wrangler is proudly naming names in its U.S.-based jeans and T-shirt supply chains beginning with family-owned cotton farms in five southern states and moving through the textile and apparel manufacturing supply chain, largely located in Georgia and the Carolinas.

Origins Of The Program

As an iconic western-wear brand, Wrangler has worked closely with the ranching community for decades and was inspired by ranchers who are at the forefront of land stewardship and regenerative agriculture. The company began exploring ways it could integrate such stewardship thinking into its own cotton supply chain.

The idea for the Rooted Collection was conceived of by the Wrangler Science and Conservation team — a collaborative group of scientists, farmers, nonprofits and industry experts working to identify and encourage best practices for land stewardship to maintain healthier soils and more viable and productive farms. This team helped Wrangler contract with some of the most sustainable cotton producers in the United States for the Rooted Collection.

“The Wrangler Rooted Collection reflects our commitment to strengthening local communities and supporting U.S. farmers,” said Tom Waldron, president, Wrangler. “Equally important, the introduction of this collection aligns with our goal to continually improve the environmental performance and traceability of our products.”

Cotton Grown In The USA

The Rooted Collection features five state-specific pairs of jeans — the Alabama Jean, the Georgia Jean, the North Carolina Jean, the Tennessee Jean and the Texas Jean — and the sustainable cotton used for each state’s jean is fully traceable to a family farm in that state:

  • The Alabama Jean — Newby Family Farms, Athens, Ala;
  • The Georgia Jean — McLendon Acres, Leary, Ga;
  • The North Carolina Jean — Lassiter Family Farms, Conway, N.C.;
  • The Tennessee Jean — Pugh Farms, Halls, Tenn.; and
  • The Texas Jean — Vance and Mandie Smith, Big Spring, Texas.

The design for each state-specific jean includes a unique wash, as well as trim and patch details featuring the state’s silhouette and other embellishments.

In addition, the collection includes two T-shirt designs for each state, as well as three national designs.

“The family farms supplying cotton to the Rooted Collection are the first growers in the Wrangler Science and Conservation program, which advocates for land stewardship and soil health best practices,” said Roian Atwood, director of sustainability, Wrangler. “These science-backed methods build crop resilience to weather disruptions while improving yield, reducing water and energy inputs, fighting erosion, and reducing greenhouse gas emissions. Wrangler aims to source 100 percent of its cotton from farms using land stewardship practices by 2025.”

A Healthy Textile/Apparel Supply Chain

Yarn and denim fabric used in the jeans collection is woven by Maudlin, S.C.-based Mount Vernon Mills at its Trion, Ga., plant. The company has been in continuous operation for more than 150 years and operates 13 production facilities making a wide range of products.

“As a longtime and trusted Wrangler supplier, we knew Mount Vernon would be the perfect partner for this collection,” Atwood said. “Mount Vernon ensured the yarn and fabric was kept traceable to the farmer by keeping the cotton laydowns separate through the carding process and into spinning. They cleaned out the machines between each run to ensure each state fabric was 100-percent made from each state’s cotton.”

The denim is cut and sewn by El Paso, Texas-based Excel Manufacturing, a garment manufacturer that opened its doors in 1977. The company employs more than 150 associates and maintains a 62,000-square-foot main facility, 20,000-square-foot cutting facility and a 30,000-square-foot warehouse. Excel makes various garments for the military, well-known apparel brands, and has a tactical products line.

A T-Shirt From Field To Final Garment

The T-shirt program uses a North and South Carolina manufacturing supply chain and features cotton grown by fifth-generation farmers Vance and Mandie Smith in Big Springs, Texas. The Smiths have been caring for their family’s land for the past 13 years and focus on sustainable farming methods and soil health.
KAWranglerTshirt
The Wrangler Rooted Collection™ features T-shirts manufactured using a 100-percent U.S.-based supply chain.

The Smith’s cotton is spun into yarn by Kings Mountain, N.C.-based Patrick Yarns Inc. Patrick was founded in 1963 and has continued to invest in state-of-art spinning technology. Interestingly, according to the company, Patrick Yarns’ legacy can be traced to the American War for Independence. According to the company: “Patrick family ancestors participated in the key battle of Kings Mountain, N.C., in which the British were soundly defeated. This tradition of rising to challenges and commitment to success is carried on by the current family ownership, and the main plants are still located [in Kings Mountain] today.”

Lumberton, N.C.-based Contempora Fabrics knits Patrick’s yarn into fabric for the T-shirts. Contempora is an employee-owned circular knitter founded in 1972. The company has more than 200 machines and a 2-million-pound-per-month capacity.

The knit fabric is dyed and finished by Gaffney, S.C.-based Carolina Cotton Works (CCW). Founded in March 1995, CCW’s primary focus is on dyeing and finishing knits and wovens for the apparel industry, however the company also serves non-apparel markets.

The dyed cotton knit fabric is cut and sewn into T-shirts by Andrews, S.C.-based Palmetto Apparel Service, and printed by Burlington, N.C.-based TS Designs — founded in 1977 as a small manual screen printer that grew over time into a fully automated printer with an environmentally conscious mind-set.

Full Transparency

The Wrangler Rooted Collection takes the unusual step of revealing the various members of the supply chains from cotton farm to finished product. In most instances, supply chain information is kept confidential and is often considered a competitive advantage. However, Wrangler has created a unique opportunity for the consumer to make a choice — to know and understand the origins of the garment they are purchasing and the farms and manufacturers they are supporting. “Authentic American” through and through.

May/June 2019
The Cloud Is Raining Pixels

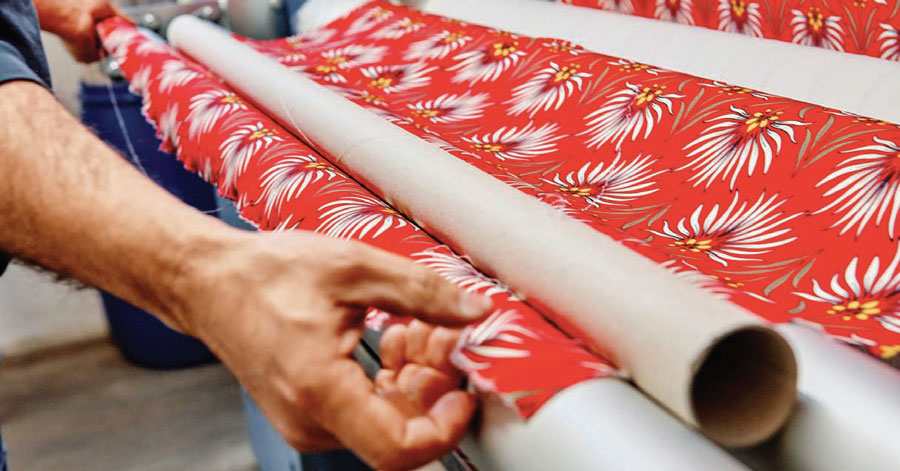
Printed fashion  fabrics created using  dye sublimination methods have brilliant, colorful designs.
Printed fashion
fabrics created using
dye sublimination methods have brilliant, colorful designs.

State-of-the-art, family-owned Neenah Coldenhove serves global customers with its innovative paper solutions.

By Mike Todaro

Everyone in the apparel industry has sent and continues to send nearly infinite volumes of digitized everything to the cloud(s), especially brilliant colorful designs and prints. Now it is time for the rain, for this tsunami of pixels to begin to fall and ironically, as important as the pixels that fall is the paper into which they land and dry. This paper is about … paper.

Shorter cycles are driving faster fashions with design-to-consumer turn times measured not in months but weeks. This fact is seen during Americas Apparel Producers’ Network (AAPN) meetings where the fiber, fabric, trim, factory and brand executives are all sitting in the same conference. Speed comes from ink and paper.

Inkjet Sublimation

The inkjet sublimation process starts with a high color fabric design that is printed onto special paper. Next, the paper is overlaid with a man-made fabric and run through high pressure rollers. During this step, the ink turns into a gas and combines with the fabric at the molecular level. The process creates designs that will never fade or run.

The apparel industry has seen countless trends and changes over the years including digitalization, globalization, computerization, fast fashion, short cycles, verticalization, 2D/3D systems, lean manufacturing, and so much more. Today, digital rules and nothing proves this more than inkjet sublimation.

Anyone in today’s supply chain located in between the designer and the consumer, is seemingly in the way. Advances in inkjet sublimation have even in some cases made the designer and the consumer the same person! This technology allows 10-minute turn times for small shops and one-day turn times for 20,000 yards of fashion fabric for the major players.

It’s The Paper

The Atlanta-based AAPN recently visited member company Neenah Coldenhove, the Netherlands. Since 1661, Coldenhove has produced paper at its facility — a place chosen because of the clean, clear, soft water springs.

Trucks arrive at Coldenhove with virgin cellulose harvested from renewable controlled forests of fast-growing eucalyptus trees. The environment is an emotional issue and Coldenhove goes above and beyond in its sustainability efforts. It has been recycling and innovating its water and energy use for nearly 350 years.

Some 95 percent of this special regional water used in Coldenhove’s production goes right back into production. The other 5 percent is used in production elsewhere on site. This Dutch company ironically will soon install an energy windmill. The company has a written goal to reduce energy by 8 percent by 2020.

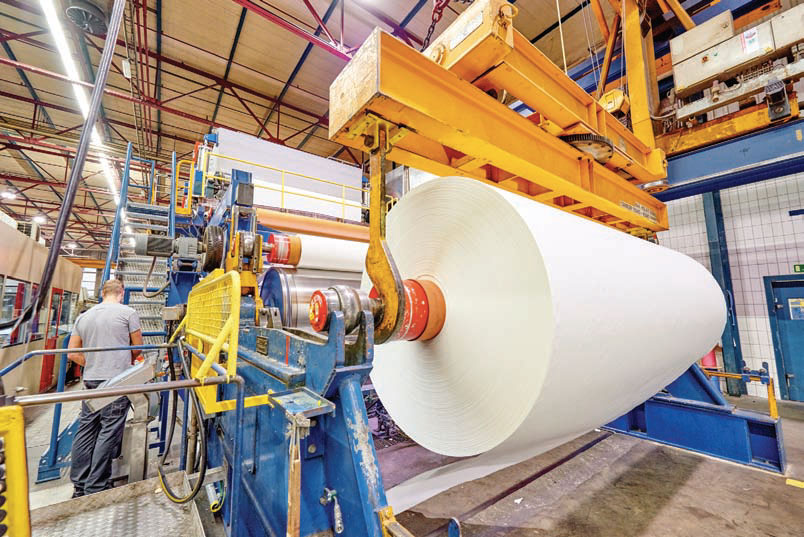
The sublimation paper manufacturing process starts with pulp, which is turned into paper in a continuous sequence. Fiber and filler are soaked in water, filtered, then run through an enormous machine out of which emerges massive rolls of coated paper, ready for inkjet sublimation. Coldenhove invented a coating that is key to full color transfer.

The company knows how to make paper of a consistent weight and strength that creates predictable prints at high speeds. Its special coating is added inline as an integrated part of the process, not later. Without this key coating, more than 35-percent of the ink is absorbed into the paper and never reaches the fabric.

It is this coating — the target for the pixels of ink — that delivers instant drying and quick release of nearly 100-percent of the expensive inks to create sharp images. Currently, this paper is delivered within 48 hours to 70 countries worldwide.

It’s The Culture

How does a company that began operations in 1661 find itself still hiring and growing and expanding its customer base today? The answer is by never stopping the creation process. As one senior manager reported: “It is not our machines or fiber or paper or coating, it is our culture that gives us a competitive advantage.”

This is why such a historical company has managed the exponential growth in volume and breadth of global coverage to more and more companies. Over this decade, for example, it has experienced double digit growth every year.

The paper Coldenhove produces is not a new technology, it’s what the company does that is so innovative. It is the company’s focus to keep ahead of the ever-changing standards of the fashion industry that matters. The speeds and flexibility of digital printing is bringing production back closer and closer to the designers, to the Americas.

ColdenhoveB
Coldenhove has been manufacturing paper at the same site in the Netherlands since 1661.

Ron Sportel, Coldenhove’s manager of innovation and development, saw the digital revolution coming in the industry. He invented digital inkjet sublimation paper, and the design that is used to apply the coating inline. Both inventions are key to Coldenhove’s value and brand name leadership in the industry.

In 2012, the industry saw a dramatic advance in the speeds of inkjet printers with increasing scale. This put enormous pressure on producers of both ink and paper. Coldenhove responded with its first product, JETCOL HTR 1000®. Today, the company offers 14 branded products with more in development.

Coldenhove prints sublimation inks on different polyester substrates with the knowledge that there is an optimum paper for every application, and countless applications. Some 43 percent of its market is in fashion, 30 percent in sporting applications, 15 percent in signage, and the balance is in home furnishing applications.

It’s The Speed And Accuracy

AAPN member El Salvador-based Textiles Opico SA de CV (TexOps) was founded in 2009. The company started slowly with inkjet sublimation printing and has reached a large scale of investment there today. TexOps has used Coldenhove paper from the very beginning.

“My partner David Ha went [to Coldenhove], very impressive place,” said TexOps President Juan Zighelboim. “They are a key vendor to us, very good reputation, make a high-quality product. We are very loyal due to quality, service and value. We don’t switch out for cheaper knock-offs available in the market.”

One mill in Europe that prints fabric for Zara’s dresses uses a single pass high-speed inkjet printer with six bridges of 100,000 nozzles each firing pixels of 3 picoliters of ink onto paper passing underneath at 2 meters per second. Think about that. If the mill receives a digital file in the morning, it can ship 20,000 yards of fashion fabric that evening. This is not only amazing speed, but can also be accomplished with monumental accuracy. This is design at its best, at speeds that are the world’s fastest for garment cycle times with margins no other brand can touch.

In her presentations, Coldenhove marketing executive Reshma Bhansing quotes Thomas Fuller who said: “All things are difficult before they are easy.” Pair that with Margaret Mead’s quote: “Never doubt that a small group of thoughtful, committed citizens can change the world. Indeed, it’s the only thing that ever has,” and this sums up Coldenhove’s team.

The power of this process is in its simplicity — printer, ink, paper, press and polyester fabric. The surprise, the secret ingredient, the piece of the puzzle that delivers exponentially more color and value than you ever imagine comes wrapped to you as what it is — the paper, the target of the designs you want to matter.


Editor’s Note: Mike Todaro is managing director of the Atlanta-based Americas Apparel Producers’ Network (AAPN).


May/June 2019

HP Launches HP Stitch S Digital Printers

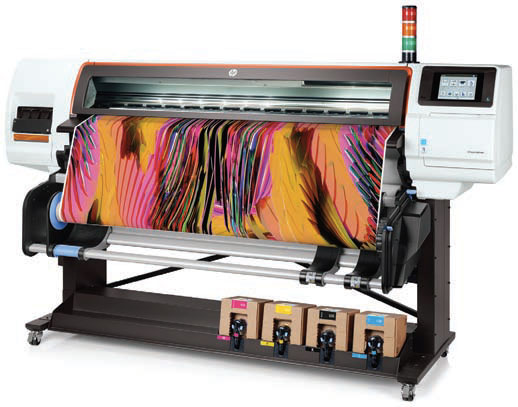
The HP Stitch S500  digital textile printer
The HP Stitch S500
digital textile printer

Palo Alto, Calif.-based HP launched its first digital textile printers. The HP Stitch S series features HP Thermal Inkjet printhead technology and uses industry standard dyes for high-quality prints using transfer paper or short-run direct-to-fabric methods. HP also offers preventative support through HP Proactive Services.

According to HP, a built-in spectrophotometer enables fast color matching within the printer, in the Raster Image Processor and in the cloud. The Stitch is currently available in three versions — the HP Stitch S300 64-in Printer, the HP Stitch S500 64-in Printer, and the HP Stitch S1000 126-in Printer. In addition, HP introduced a line of transfer papers compatible with the Stitch series machines.

The HP Stitch S300 also offers a user-replaceable printhead, which reduces downtime and service costs. “Our experience with HP Stitch S300 has been much easier and faster than other dye sub printers we’ve previously used,” said Teunis Roos, Color Concepts. “Most printers require manual action in terms of head maintenance and alignment, but the HP Stitch S300 is more proactive and automated when it comes to performance.”

May/June 2019

Kornit Introduces Presto, NeoPoly Technology

Israel-based Kornit Digital has introduced the Kornit Presto, an industrial single-step solution for direct-to-fabric printing capable of running of speeds of up to 450 square meters per hour. According to the company, the Presto eliminates the need for pre- or post-treatment of the fabric, and may be used on a wide variety of fabric types. The Presto also is a water-free process that uses the new NeoPigment™ Robusto pigment-based inks. Kornit reports that the fast physical and chemical bonding characteristics of the Robusto inks offer a significant reduction in curing time. Presto is targeted toward on-demand fashion and home décor applications. The system will be commercially launched at ITMA 2019 in Barcelona.

“We were thrilled to be able to test the new system and found the Presto to be in a class by itself; it prints beautifully on all kinds of fabrics, in a single-step, with an environmentally friendly dry process, and now at a multiple of productivity,” said Gart Davis, CEO, Spoonflower — a web-based service for custom, on-demand fabric and design creation and a long-time Kornit customer.

In other company news, Kornit also introduced the Kornit NeoPoly Technology for high-quality printing on polyester. Kornit’s Avalanche Poly Pro is the first system equipped with the new NeoPoly Technology, which is aimed at the T-shirt and sport apparel market, where polyester is a key substrate.

“Kornit is on a mission to reinvent the textile printing industry with game-changing sustainable technologies for growing market segments,” said Omer Kulka, Kornit’s vice president of marketing and product strategy. “We continually work to break technology boundaries, so that our customers can innovate and open new markets and new business opportunities, while being more operationally efficient.”

May/June 2019

Siris Capital Affiliate To Acquire EFI™

Fremont, Calif.-based Electronics For Imaging Inc. (EFI™) reports it has entered into an agreement to be acquired by an affiliate of Siris Capital Group LLC, New York City — a private equity firm focused on investing in technology companies that provide mission-critical solutions and are facing technology transitions.

The all-cash deal is valued at approximately $1.7 billion. EFI’s board of directors has unanimously approved the terms, whereby the Siris affiliate will acquire all the outstanding EFI common stock for $37 per share. EFI maintains the right to solicit alternative proposals from third parties and may terminate the agreement if a superior proposal is found subject to the terms and conditions of the agreement. The proposed transaction is expected to close by the third quarter of 2019 subject to EFI shareholder and antitrust regulatory approvals.

EFI reports it anticipates first quarter 2019 revenue to be between $220 million and $225 million.

“We believe this transaction delivers superior and immediate value to our shareholders while providing us with a partner that can add strategic and operational expertise to our business,” said Bill Muir, CEO, EFI. “We are excited to partner with Siris’ highly experienced team on this next phase of growth for EFI.”

May/June 2019

Polartec Debuts Ready To Roll Program

Polartec, Andover, Mass., recently introduced a Ready to Roll program — featuring in stock, first-quality Polartec fabrics that are ready to be shipped. “Customers have long asked for in-stock inventory without the standard production lead times, and this announcement enables rapid order fulfillment in time for fall/winter 2019 production to meet increased demand,” said Gary Smith, Polartec CEO.

According to the company, Ready to Roll includes premium Polartec fabrics in most of the
popular styles as well as more rare styles — such as cooling, insulating and flame resistant technologies — and hard-to-find colors.

The Ready to Roll program is an extension of Polartec Eco-Engineering™, the company’s process for deploying recycled and biodegradable inputs, advanced production techniques, efficient logistics and rigorous testing and certifications.

The company also recently upgraded its production capacity to meet high demand for shearling and Sherpa fleece fabrics.

May/June 2019

Speedo Expands Fastskin

Speedo has issued the latest technology in its Fastskin range designed to allow a swimmer to achieve maximum speed in the water. Developed in partnership with Switzerland-based HeiQ, the new Fastskin LZR styles — Pure Intent and Pure Valor — are the latest generation of the technology, which was originally introduced in 2008. According to Speedo, LZR Pure Intent features the shark skin inspired technology developed with HeiQ, as well as a unique triple fabric construction that enhances compression and flexibility. LZR Pure Valor, codeveloped with HeiQ, was engineered to be light and flexible so swimmerscan reduce drag and increase power in the water.

“With almost two decades of improvements in our Fastskin technology, we are excited to partner with HeiQ to give our racers the ultimate advantage with drag reduction technology to improve their speed,” said Rebecca Bennett, materials specialist at Speedo. “We’ve worked very closely with our athletes and taken all their feedback on board to help them get the suit they need to perform at their absolute best.”

“We are proud to combine our in-depth knowledge in textiles with Speedo’s expertise in swimwear to develop a differentiating innovation,” said Carlo Centonze, HeiQ CEO. “This is the outcome of the close collaboration between Speedo and HeiQ’s research hubs in Australia and Switzerland.”

May/June 2019

FIT, IBM Partner On AI Projects, Innovation

The New York City-based Fashion Institute of Technology (FIT) has announced that its FIT/Infor Design and Technology Lab (DTech Lab) has partnered with IBM Corp. to leverage IBM’s artificial intelligence (AI) for fashion capabilities. IBM’s AI for Fashion application programming interfaces (API’s) were developed to help fashion companies improve customer service, product design, development and merchandising by leveraging deep learning, natural language processing and computer vision. The suite of API’s can be used individually or be incorporated into existing applications.

The DTech Lab partnered with IBM and Tommy Hilfiger in 2018 on the “Reimagine Retail” project, which was designed to show how AI can offer a brand a competitive edge. The project was successful to the point that FIT and IBM are continuing their partnership with innovative research and partner projects that will address challenges in product design, development, merchandising, planning and allocation, and customer sales and service. FIT also plans to integrate IBM’s AI tools into coursework for students.

“Reimagine Retail was a powerful example of what happens when fashion partners with a global tech leader to advance challenging innovations,” said Michael Ferraro, director of the FIT/Infor DTech Lab. “Embedding emerging technology into our lab where faculty and students are solving industry problems is the next step in our evolving relationship with IBM. We’re leveraging the fresh perspectives and new ideas of talented creative students in an agile research environment.”

May/June 2019

PVH, NIKE Enter Men’s Underwear Licensing Agreement

New York City-based PVH Corp. has entered into a licensing agreement — that includes design, sourcing, marketing and worldwide distribution — with Portland-based Nike Inc. for Nike-branded men’s underwear. PVH reports it will use its innovative underwear platform while adhering to quality standards and corporate responsibility. The agreement expands The Underwear Group at PVH and adds Nike to its existing brands: Calvin Klein; Tommy Hilfiger; Olga; Warner’s; and True & Co.

“We are incredibly proud to be working with NIKE, as this is an opportunity for two great companies to build on each other’s strengths, making it a win-win for everyone, especially consumers,” said PVH’s Cheryl Abel-Hodges, President of Calvin Klein North America and The Underwear Group.

May/June 2019

Static Free? — Ascend’s Nylon 6,6 Answer Is ENDUR

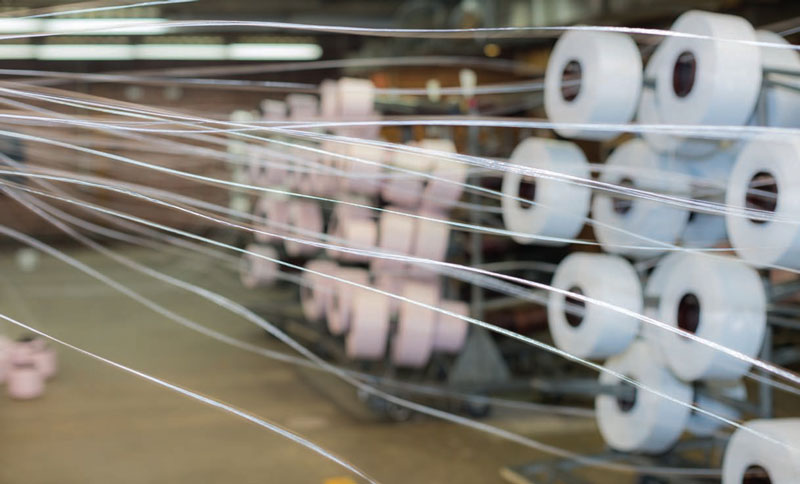
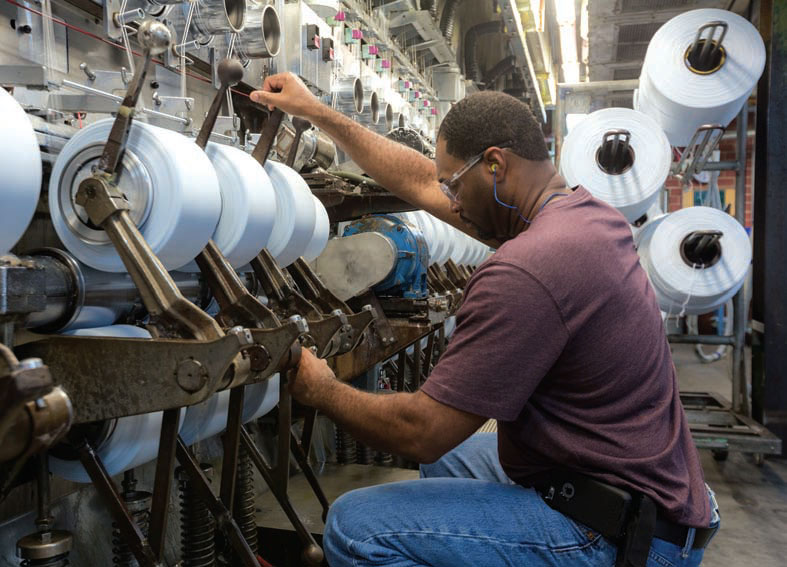
Ascend Performance Materials’ Fiber Center of Excellence in Greenwood, S.C., produces nylon 6,6 staple fiber.

Nylon 6,6 producer Ascend Performance Materials is solving problems with its antistatic, anticling ENDUR by Ascend™ yarn.

TW Special Report

Nylon is a material that plays a significant role in daily life, but its performance attributes and extensive applications are rarely recognized by the average consumer. This man-made polymer, first synthesized in 1937, is formed when specific chemical building blocks called monomers are brought together to create long chains known as polymers. Because of its versatility, nylon has traditionally been used to create products ranging from women’s stockings to Army parachutes and cording.

Nylon 6,6 is just one type of polymer used in textiles — other common textile polymers include nylon 6, polyester, rayon and polypropylene. Today, the uses for nylon 6,6 have grown to include all types of apparel, tires, automotive airbags and carpet, among other applications.

Houston-based Ascend Performance Materials is a privately owned, fully vertical nylon 6,6 producer, with roots going back more than 60 years. Ascend specializes in nylon 6,6 resins, fibers and compounds as well as specialty and intermediate chemicals used throughout the polymer value chain. In recent years, the company has expanded facilities including capacity increases across its intermediate chemicals and polymers portfolio. Today, Ascend has sales and technology offices throughout the world and six manufacturing facilities and a technology center in the United States. Globally, the company employs approximately 3,500 associates and contractors. In addition, Ascend has announced a $35.2 million investment in Greenwood County, S.C., that will create 30 new jobs.

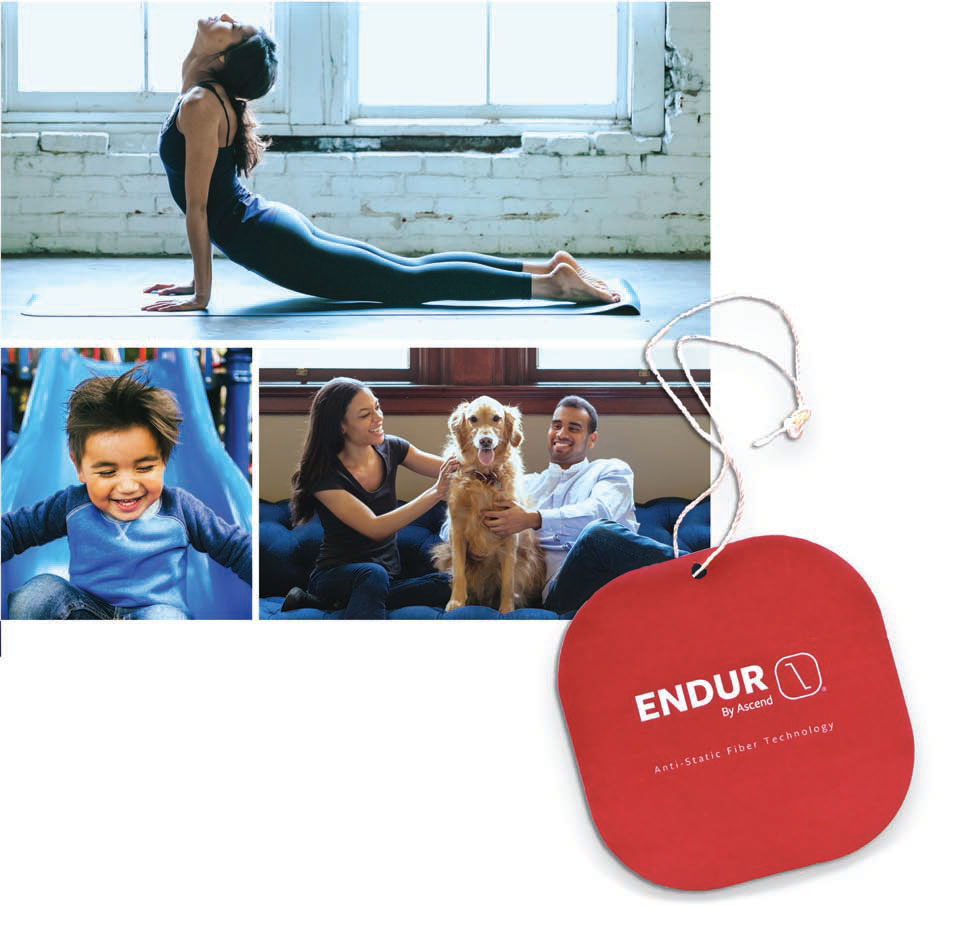
ENDUR by Ascend™ is a unique antistatic fiber technology that adds value to yoga and performance gear, loungewear, and childrenswear among other garments. The company also offers a hangtag program for customers using the fiber.

Adding Performance Beyond The Basic

Amongst Ascend’s line of products is ENDUR by Ascend™, a fiber product differentiated by its unique antistatic technology. It is a filament- or staple-fiber product that can be blended with other fibers and yarns to provide fabrics with permanent antistatic functionality because it is neither a garment treatment nor a coating that can wear off over time. The yarn has a bicomponent structure featuring one-part nylon 6,6, and one-part conductive carbon. These two components are joined together during the high-temperature yarn extrusion process to produce a fiber that, among other attributes, eliminates static electricity.

In Endur, the conductive carbon component of the fiber grounds and harmlessly moves electricity through the garment, preventing a build-up of static electricity and removing the possibility of an electric shock.

Harrie Schoots, Specialty Fibers Segment Manager, Ascend Performance Materials

“Endur is a speciality fiber product and the furthest down the value chain that Ascend sells,” said Harrie Schoots, Ascend’s Specialty Fibers Segment Manager. “It’s been exciting for me to take the product out to the brands, retailers and design folks and explain it to them and show them what it can do for their apparel products.”

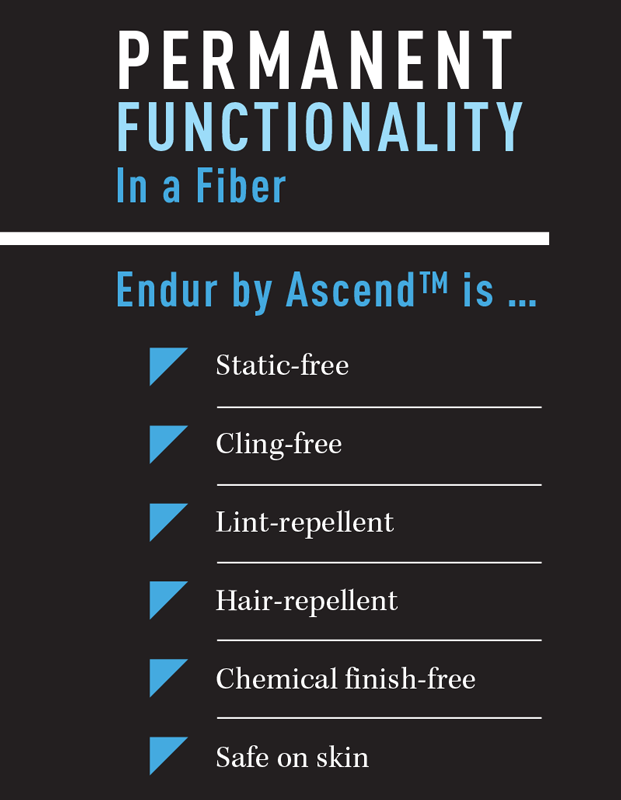
Beyond reducing static within a garment, Endur imparts other desired attributes to a finished product (see box).

These important properties help designers improve yoga and performance gear, loungewear, shapewear, eveningwear, childrenswear and medical garments. For example, Endur can help reduce bothersome and potentially harmful qualities in fabrics such as clinginess and lint and allergenic debris accumulation, while providing comfort in chemical-free, next-to-skin applications.

Futhermore, as a unique bicomponent fiber, Endur offers permanent value. As Schoots explained: “Because of the high temperature at which nylon 6,6 is melted and combined with the carbon, the fiber becomes very abrasion resistant and the carbon does not break off or flake away from the fiber, which is a very important property. In the past people have tried to weave or knit with a yarn that has been coated with carbon at a much lower temperature and the coating flaked off. If you have black specks of carbon on the machinery and then you run white fabric behind it, you can imagine what a problem that is.”

AscendBoxProof In The Testing

To demonstrate that static does not build up in fabrics developed with Endur, Ascend employed the American Association of Textile Chemists and Colorists’ (AATCC) Test Method 115 — Electrostatic Clinging of Fabrics: Fabric-to-Metal Test.

“AATCC’s cling test is a test I think I pulled out of the basement from the polyester leisure suit days — it tests the static cling of fabrics,” Schoots said. “But we also had to show that the static is not in the fabric, and that’s why our lab offers the static decay test for customers.”

Ascend’s static decay test charges a fabric to 5,000 volts, then measures the time it takes for 90 percent of that charge to dissipate. “In many cases, fabrics will take more than a minute,” Schoots said. “But in order to show that a material offers static reduction, the time measured has to be less than half a second. Typically, fabrics featuring Endur take 0.01 seconds to reduce the charge. Essentially, if you wear a dress or yoga pants with Endur on a very dry winter day, you would not generate any static electricity when walking or sitting for example.”

Ascend is openly committed to its employees and is dedicated to a safe, healthy and sustainable workplace.

Ascend: Making A Difference

Ascend, whose operations are based in the United States, has weathered the storm and resisted moving production to other countries. U.S.-based manufacturing has remained profitable for the company, and Ascend has never been more successful than it is today.

At the core of this success is Ascend’s open commitment to its employees. “The company values the communities and individual employees who are the lifeblood of Ascend,” Schoots said. “Our president and CEO, Phil McDivitt, is dedicated to a safe, healthy and sustainable workplace. Well beyond manufacturing a quality product, his goal is to have no incidents and zero accidents throughout the entire corporation, and he’s taken steps to ensure we all know that.”

The company also created the Ascend Cares Foundation in 2011 after employees of its Decatur, Alabama, facility were impacted by a tornado. According to the company: “The Ascend Cares Foundation is about making a difference in the lives of others. It is led by Ascend employees and supports Ascend families in their time of need, provides inspiring opportunities for community engagement and facilitates community leadership. Funded entirely by donations and company match, every dollar donated to the foundation supports the work of the foundation.”

Since its inception in 2011, Ascend reports the following tangible accomplishments made by the foundation:

  • Volunteers cleaned and repaired 55 homes and served more than 1,000 meals to employees impacted by Hurricane Harvey in Texas;
  • Volunteers have built five Habitat for Humanity homes on-site at Ascend’s Chocolate Bayou, Texas; Greenwood, South Carolina; and Decatur, Alabama, facilities;
  • Some 135 college scholarships totaling $205,000 have been awarded to team members’ children;
  • Children at Escambia Westgate School in Florida play on a new sensory playground that is the foundation’s largest project to date;
  • Volunteer events at Ascend sites help local organizations such as food banks, animal shelters and schools; and
  • A total of 206 families have received financial hardship support.

Ascend accounts for approximately one quarter of global nylon 6,6 production. According to the company, its “… vision is to be [a] recognized leader in the nylon 6,6 value chain, creating new possibilities with nylon 6,6 for everyone, everywhere, every day.”


Editor’s Note: This article appears in Textile World courtesy of the National Council of Textile Organizations (NCTO) as part of the “American Textiles: We Make Amazing™” campaign. NCTO is a trade association representing U.S. textile manufacturing. Please visit ncto.org to learn more about NCTO, the industry and the campaign.


May/June 2019

Sponsors