BTU-TECH Introduces BTU-GMAX, Delivering Premium Multiaxial Production Flexibility At An Entry-Level Investment Range

BTU-Tech-LogoISTANBUL — September 29, 2026 — BTU-TECH has announced the launch of BTU-GMAX, a next-generation multiaxial production line developed to deliver the flexibility of advanced multiaxial platforms at an investment level comparable to conventional entry-level machines.

With its fully programmable 0°–180° weft-angle capability, BTU-GMAX enables manufacturers to produce a wide range of multiaxial fabric architectures, mainly glass, aramid, carbon fabrics for composite industries, on a single platform. Operators can select new production angles directly from the interface without lengthy mechanical adjustments.
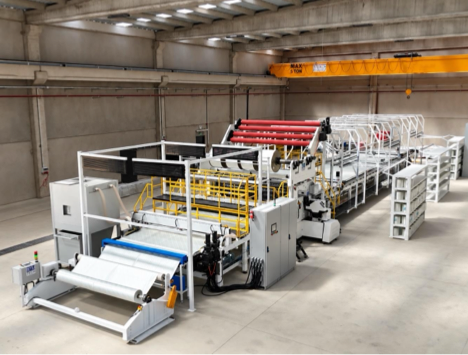
BTU-TECH PictureOne of the system’s key innovations is its ability to calculate weft paths directly on the industrial motion controller in real time. New production parameters can be applied within seconds without external computer software, CAM table generation, or a machine restart. This significantly reduces setup times and increases machine availability.

BTU-GMAX uses a heavy-duty trigger-belt-driven carrier architecture instead of conventional rack-driven systems. The design reduces wear and noise, improves positional accuracy, prevents jump-offs at high speed, and simplifies maintenance.

Built on BTU-TECH’s proprietary PC-free automation platform, the system combines real-time weft-curve calculation, automatic carrier synchronization at every production start, and electronic collision prevention. Integrated laser safety barriers dynamically monitor operator positioning, while Industry 4.0 connectivity allows production data and machine parameters to be transferred to ERP systems and factory networks via industrial communication protocols.

BTU-TECH Managing Partner Burçin Pak commented:

“Manufacturers have traditionally faced a choice between basic entry-level machines with limited flexibility and premium platforms requiring significantly higher investment. We developed BTU-GMAX to eliminate this compromise. Our goal was to combine premium production flexibility, advanced automation and ease of operation with an investment level comparable to entry-level alternatives.”

Developed entirely by BTU-TECH, BTU-GMAX brings together the company’s proprietary software, automation, motion-control, and mechanical-engineering technologies in a single production platform. After power-up, the machine boots, initializes, and self-calibrates in less than 10 seconds.

BTU-GMAX supports 380–480 VAC, 110–240 VAC, and 50–60 Hz power systems. Its electrical and hardware architecture has been designed in accordance with international CE compliance requirements, supporting straightforward deployment worldwide.

Optional add-ons—including a glass-fiber roving chopper, the BTU-TECH All-in-One Winder and a hook- pin break-detection system—allow the line to be configured for different production requirements.

Posted: October 8, 2026

Source: BTU-TECH

Teijin Frontier And Asahi Kasei Advance Complete Business Integration And Launch TA Frontier Co., Ltd.

TOKYO — October 1, 2026 — Teijin Frontier Co., Ltd., and Asahi Kasei Advance Co., Ltd., completed the integration of their business operations effective today, and have launched the new entity as TA Frontier Co., Ltd.

This integration combines the customer bases and business platforms that the two companies have developed, with the goals of building greater competitiveness, responding more effectively to rapidly changing market conditions and achieving sustainable growth.

TA Frontier, the new integrated company, embraces a corporate philosophy of “Creating new value that contribute to a healthy environment and a prosperous future.” It will provide solutions from textiles and apparel to industrial materials, construction materials and resin products that help address challenges in daily life and business across a wide range of industries.

“Through this business integration, we have taken a new step forward as TA Frontier Co., Ltd,” stated Susumu Kamata, President and Chief Executive Officer of TA Frontier. “By bringing together the experience, technologies and expertise cultivated by both companies, we will deliver products and services with even greater added value to address the diverse challenges faced by our customers. We will strive to become an attractive company that continues to earn the trust of our customers and society by responding to their changing needs and taking on the challenge of creating new value.”

Company Overview

Company Name TA Frontier Co., Ltd.
Representative President and Chief Executive Officer: Susumu Kamata
Head Office Location Nakanoshima Festival Tower West, 2-4, Nakanoshima 3-chome, Kita-ku, Osaka 530-8605, Japan
Principal Business Activities Manufacture, processing, sale and import/export of polyester and other yarns and staple fibers, textiles, apparel, automotive materials, chemicals, construction and interior materials, industrial materials and consumer products, etc.
Capital JPY 2.0 billion
Shareholders and Shareholding Ratios Teijin Limited, 80%; Asahi Kasei Corporation, 20%
Number of Employees Non-consolidated: 1,373 employees

(consolidated: 6,281 employees)

Website https://tafrontier-grp.com/english/

Posted: October 8, 2026

Source: Teijin Group

Chloris Strengthens Commercial Readiness Of Claessen Blue™ Through An Integrated Verification Framework

Chloris Colors logoWEST JORDAN, Utah — September 23, 2026 — Chloris is strengthening the commercial readiness of its flagship bio-based dye, Claessen Blue™, through a growing international verification framework covering bio-based origin, traceability, responsible chemical management and textile application.

Rather than treating individual certifications as standalone credentials, Chloris has organized them around the key questions brands, mills and manufacturers need to address when evaluating a new material.

Bio-based Origin — USDA BioPreferred® and OK biobased provide independent verification of bio-based carbon content, supporting clear and credible renewable-material claims.

Traceability — ISCC PLUS extends verification into renewable feedstocks and chain-of-custody traceability, connecting material sourcing with industrial production.

Chemical Safety — ZDHC MRSL Level 3 and OEKO-TEX® support chemical management and textile chemical safety requirements relevant to global sourcing and manufacturing.

Application Approval — GOTS Approved Input supports the use of Claessen Blue™ within GOTS-certified textile processing, subject to applicable requirements.

In parallel, Chloris uses Life Cycle Assessment (LCA) as a separate layer of quantitative environmental evidence.

While certification verifies attributes, processes and compliance pathways, LCA evaluates environmental performance within defined life-cycle boundaries. This provides brands and supply-chain partners with measurable evidence across relevant environmental indicators and helps translate sustainability from a material claim into data that can inform sourcing and ESG decisions.

Together, these elements create an increasingly integrated evidence framework around Claessen Blue™ — from renewable origin and traceability to chemical management, textile application and quantified environmental performance.

Produced through microbial fermentation using renewable feedstocks, Claessen Blue™ has been developed with three priorities in parallel: sustainability, product performance and commercial scalability.

For brands, mills and manufacturers seeking lower-impact color solutions, the objective is straightforward: make bio-based color not only innovative, but increasingly verifiable, usable and ready to scale.

Posted: October 8, 2026

Source: Chloris Colors

Selenis Acquires Polisan Hellas Assets And Expands Specialty Copolyester Production To More Than 200,000 Tonnes By 2028

PORTUGAL — October 8, 2026 — Selenis, the only specialty copolyester producer manufacturing in Europe, has acquired the production assets of Polisan Hellas in Greece for installation in Portugal. Including these assets, Selenis will operate more than 200,000 metric tonnes (MT) of annual installed specialty copolyester capacity by 2028, across production sites in Portugal, Italy, Tunisia and the United States.

The acquisition adds continuous polymerisation to a manufacturing base built on flexibility. Continuous production serves the high-volume markets, where standardisation, consistency and cost per tonne matter.

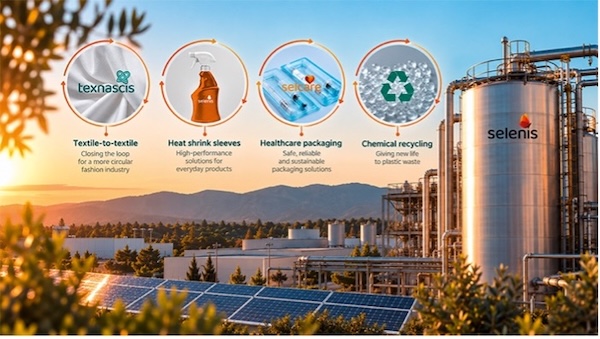
Selenis investment supports growth in four priority markets, Texnascis™, Shrink sleeves, Selcare® and Mimesis™

Batch production serves specialty and custom grades, where smaller volumes, fast changeovers and formulation depth are key. With both technologies now part of its manufacturing platform across four countries, Selenis can serve the full spectrum of the market, from high-volume applications to specialised grades, combining the scale and efficiency of continuous production with the flexibility of batch manufacturing.

“We believe Europe needs a strong specialty materials manufacturing base, and we are investing to build it,” said Duarte Matos Gil, CEO of Selenis. “When customers qualify our materials, they make a long-term commitment. Our responsibility is to invest ahead of their needs, to put more than one plant behind every grade and to give them a cost base that lets them compete. This acquisition puts industrial capacity behind that commitment, and further steps will follow.”

Supply resilience is central to the expansion. Selenis will work with customers to qualify selected grades at more than one manufacturing site, so a converter can hold the same specification from two plants, with no dependency on a single line or region and with the flexibility to move volume between sites as demand and logistics change. Qualification will follow the technical and approval requirements of each application. European converters are supplied from Europe and American converters from the United States, with shorter lead times and lower safety stocks than imported resin requires.

“Our ambition is to be the supplier customers choose for their next generation of products,” added Duarte Matos Gil. “That takes technical depth, dependable supply from more than one plant and the capacity to grow with them. We are building Selenis for that responsibility.”

The continuous assets also change the cost base. Continuous polymerisation runs at a lower conversion cost per tonne than batch, and Selenis will direct its standard grades for shrink sleeves, film and sheet onto that line. That competitiveness supports long-term supply agreements with customers who commit volume: multi-year, qualified and predictable on both sides.

The investment supports growth in four priority markets. Shrink sleeves, film and sheet, where the continuous line brings uniform high-volume grades at a competitive cost base, backed by the packaging know-how of the wider IMG Group. Healthcare, through Selcare®, where multi-site qualification and continuity of supply are conditions of doing business. 3D printing, where Mimesis™ product range supplies PETG and PCTG resin to filament producers serving industrial manufacturing, automotive, electronics, education and consumer markets, in applications from functional prototypes to end-use parts. And textile-to-textile recycling, where Texnascis™ works with chemical recycling partners to turn recovered monomers into new polyester; Selenis brings the polymerisation expertise and industrial scale these technologies need to reach commercial volume.

The Polisan Hellas assets will be installed in Portugal, in line with the capacity doubling already announced and underway. Selenis’ industrial footprint spans Portugal, Italy, the United States and Tunisia, and the Group is already assessing the next investments. “We are evaluating new investments in Germany in the bio-based field and in Tunisia, where we are exploring textile-to-textile opportunities through DMT technology. Each investment adds a capability to one manufacturing platform, and each is chosen for the markets where our customers see the strongest long-term growth,” said Eduardo Santos, Strategy & Integration Director at IMG Group.

Selenis’ expansion strategy is designed to provide long-term security, scale, and operational flexibility to customers requiring reliable global specialty copolyester supply across highly technical and demanding applications.

Posted: October 8, 2026

Source: Selenis

Reshoring Textiles Acquires Sans Fibers To Advance US Textile Manufacturing

Reshoring Textiles LogoSTONEVILLE, N.C. — October 8, 2026 — Reshoring Textiles has acquired Sans Technical Fibers, an American producer of high tenacity LDI nylon 6.6 and polyester yarns. Sans will operate alongside Spinnere as a sister company within Reshoring Textiles, and industry veteran John Garner has been named its CEO. Robert Antoshak has been named Chief Marketing Officer of Reshoring Textiles.

The acquisition adds domestic filament production for technical and specialty uses, including sewing thread and industrial textiles, giving Reshoring more to offer manufacturers in apparel and industrial markets.

“Reshoring is dedicated to helping American textile manufacturing grow,” said Josh Nieuwsma, CEO of Reshoring Textiles. “Customers need reliable long-term domestic sources of the raw materials their products require. Sans gives us an established operation with deep experience in specialty nylon and polyester. Alongside Spinnere, it will help us supply more of those needs from U.S. facilities, and support manufacturers and startups looking to grow and build their businesses here.”

Based in Stoneville, North Carolina, Sans has supplied high tenacity filaments for more than two decades. Its nylon yarns range from ultrafine to heavier deniers and offer UV stabilization and favorable dyeing characteristics. The company expanded into polyester in 2017, with new production equipment entering service in 2018 and in 2024. Sans now offers polyester yarns from fine deniers to heavy denier industrial. With new extrusion equipment on its way, Sans will be able to offer significantly more and different polymers to its customers.

Known for high strength and low shrinkage, Sans yarns are used in sewing threads, narrow fabrics, braided cords and other technical textiles. End markets include apparel and footwear, as well as medical, military, automotive and manufactured rubber products.

“Sans has built its reputation on consistent, high-performance fibers,” said John Garner, CEO of Sans Technical Fibers. “Our mission statement: to make it easy to do business in America. We don’t like the word no.”

Sans is ISO 9001 certified and manufactures all of its products in North Carolina from U.S.-made raw materials. Its products comply with the Berry Amendment and USMCA, and the company serves customers on five continents.

Posted: October 6, 2026

Source: Reshoring Textiles

Milliken Achieves Cradle To Cradle Certified® Silver Version 5.0 For Global Carpet Portfolio

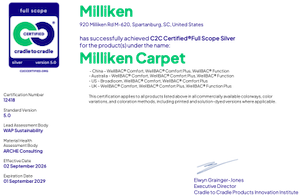
SPARTANBURG, S.C. — September 30, 2026 — Milliken & Company has achieved Cradle to Cradle Certified® Silver Version 5.0 for its global carpet portfolio, reinforcing the company’s longstanding commitment to material health, product circularity, and sustainability leadership. The certification provides architects, designers, and building owners with independent validation that Milliken products meet rigorous requirements across multiple sustainability categories.

Cradle to Cradle Certified® is one of the built environment’s most recognized sustainability certifications, evaluating products across areas such as material health, product circularity, clean air and climate protection, water and soil stewardship, and social fairness. Milliken’s certification covers the full scope of these requirements, demonstrating a holistic approach to responsible product design and manufacturing.

“For many customers, sustainability information has become increasingly complex,” said Allie Bruski, Vice President, Product Marketing for Milliken’s flooring business. “This certification provides confidence that when they specify Milliken flooring, they are choosing products that have been independently evaluated for material health, circularity, and broader sustainability performance.”

The certification also reflects Milliken’s broader legacy of transparency and product stewardship. For decades, the company has invested in helping customers better understand the materials that contribute to healthier, higher-performing spaces. Cradle to Cradle Certified® Silver provides trusted third-party validation of that commitment.

While sustainability remains a critical consideration, Milliken believes customers should not have to compromise on performance, comfort or design. In addition to meeting recognized sustainability standards, Milliken flooring solutions continue to deliver the versatility, durability, and occupant-focused benefits customers expect from a flooring leader. The company’s cushion-backed flooring platform further supports comfort, acoustics, and ergonomics, helping create spaces that perform as well as they inspire.

“This achievement validates the work our teams have done to embed sustainability into the way we design and manufacture products,” said Dale Kitchen, Director, Research and Development for Milliken’s flooring business. “It also gives customers one more reason to feel confident that Milliken flooring can help them meet both sustainability goals and performance expectations.”

For more information about Milliken’s flooring solutions, visit www.milliken.com

Posted: October 6, 2026

Source: Milliken & Company

UNIFI®, Makers Of REPREVE®, Launches Cofira™, Dual Function Yarn, And Expands Water Resistant Offerings With Resist2O™ Pro

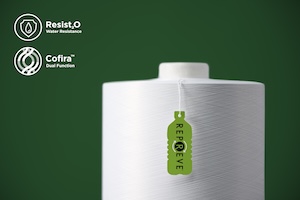
GREENSBORO, N.C.— September 30, 2026 — UNIFI, Inc., the makers of REPREVE® and one of the world’s innovators in recycled and synthetic yarns, today launches Cofira™, a versatile yarn that can be tailored with synthetic, blended, and functional fiber technologies for enhanced performance.

UNIFI - UNIFI®, Makers of REPREVE®, Launches Cofira™, Dual Function Yarn, and Expands Water Resistant Offerings with Resist2O™ ProThis innovation within UNIFI®’s portfolio delivers a fusion of filament and spun characteristics in one yarn, offering the advantage of spun yarn comfort with filament functionality.

Cofira offers broad design flexibility that supports the integration of sustainable performance technologies. Designed for versatility, it is ideal for applications including apparel, furnishings, gear, and accessories.

Key features of Cofira:

  • Combines spun yarn aesthetics with filament yarn performance in one construction;
  • Enables unique fabric aesthetics and hand feel;
  • Can be combined with other UNIFI technologies including: A.M.Y.®, ChillSense®, and ReFlexx® ; and
  • Available globally in virgin and REPREVE polyester yarns, including REPREVE Takeback™, with REPREVE options fully traceable via FiberPrint® technology and certified by U-TRUST®, GRS, and SCS for recycled content.

In addition, UNIFI also announces the launch of Resist2O™ Pro, an expansion of water-resistant offerings engineered for all types of fabric formation. Designed to deliver durable water resistance without compromising fabric performance, Resist2O Pro gives brands and manufacturers greater freedom to develop water-resistant fabrics for a wide range of textile applications, without the use of topical treatments or fluorinated chemistry. From apparel and footwear to furnishings and industrial, Resist2O Pro is ready to perform in a variety of applications.

Key Features of Resist2O Pro:

  • Minimizes water absorption;
  • Eliminates the need for traditional topical DWR finishes;
  • Fluorine free technology; and
  • PFOA-free technology (defined as below 5ppb).

“These new products bring true innovative solutions through their multifunctional capabilities,” said Eddie Ingle, CEO of UNIFI, “that help reduce complexities associated with high-performance products. Engineered with recycled materials, these high-performance tech yarns are both versatile and sustainable.”

UNIFI will showcase Cofira and Resist2O Pro technologies at Performance Days Munich (Booth #J18) in Munich, Germany on October 13-14 and the Functional Fabric Fair (Booth #730) in Portland, Oregon on October 26-28.

Posted: October 6, 2026

Source: UNIFI, Inc.

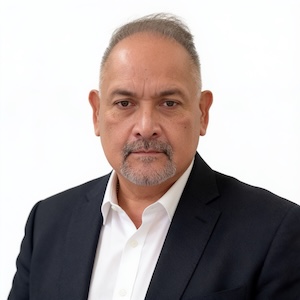
Humberto Medrano joins Herculite as Regional Sales Manager

EMIGSVILLE, PA — September 30, 2026 —  Herculite Products Inc., an innovator in High Performance and Custom Fabrics with recognized brands such as Coastline Plus and Patio 500, is pleased to announce that Humberto Medrano has been hired as Regional Sales Manager covering the Southwest to develop and grow relationships with End Product Manufacturers and related sales personnel for all Awning and Marine brands and to promote awareness, loyalty, and consumption of our industry-leading awning fabric brands through our distribution partners.

Herculite Products Inc. - Humberto_Medrano
Humberto Medrano

Humberto holds a Bachelor of Science in Electronic Engineering from DeVry University. He has more than 40 years of international and domestic sales and account management experience, including over 20 in the textile industry. He currently lives in Azusa, California, is a dad to four amazing grown children, and a grandfather to two beautiful little girls. Humberto enjoys baseball and has played and coached in his spare time; one of his children played at the college level, and the other played in the Mexican professional league.

At Herculite, we are committed to delivering the highest level of service, support, and innovation in the industry. We are confident that Humberto’s experience, communication skills, and customer-focused approach will make him a valuable addition to our team and enable him to contribute meaningfully to our mission.

Posted: October 6, 2026

Source: Herculite Products Inc.

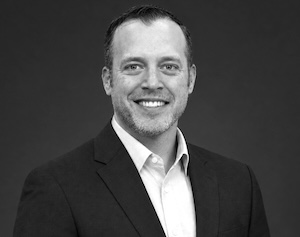
CPM Names Jeremy Patten Chief Executive Office

BLAINE, Minn. — October 2, 2026 —  CPM, a global provider of process equipment, engineered technologies and aftermarket support, announced today that Jeremy Patten has joined the company as Chief Executive Officer.

CPM - Jeremy Patten
Jeremy Patten

Patten brings more than 20 years of leadership experience across global industrial, manufacturing and technology-driven businesses. Most recently, he served as President of Modine’s Performance Technologies segment. Prior to Modine, he spent more than eight years with ATS Corporation, including serving as President of its Packaging and Food Technology Group. Earlier in his career, Patten held leadership roles with IDEX Corporation and Danaher Corporation.

“Jeremy brings the combination of operational leadership, commercial experience and focus on execution that makes him well suited to lead CPM,” said Simon Peckham, Chief Executive of Rosebank Industries. “CPM has strong market positions, longstanding customer relationships and significant opportunities for growth. We are pleased to have Jeremy leading the business as we invest to build on those strengths, grow the aftermarket and improve performance across the organization.”

Patten joins CPM as the company continues to focus on growth, operational improvement and strengthening support for customers throughout the full lifecycle of their equipment.

“CPM has strong brands, deep engineering expertise, long-standing customer relationships and a significant global installed base,” said Patten. “What attracted me to CPM is the opportunity to build on those strengths, grow the business and continue improving how we support our customers throughout the lifecycle of their equipment. I’m looking forward to getting to know our people, customers and businesses around the world.” 

Posted: October 6, 2026

Source: CPM

IND HEMP Invests In Premium Fiber Processing Line

IND HEMP Logo NEWFORT BENTON, Mont. — October 1, 2026 — IND HEMP, a producer, processor and supplier of industrial hemp materials in the USA, today announced a significant investment in new fiber processing equipment at its IH Fiber decortication facility in Fort Benton, Montana. The investment adds a secondary processing line, featuring multiple fiber refining technologies to perform opening, cleaning and cottonizing, that brings IND HEMP’s hemp fiber to a ready-to-spin quality directly at the source.

Yarn is the foundation from which nearly every fabric application is built. Once hemp fiber is spun into yarn, it can be woven or knit into a wide range of end products, from garments and home goods to technical fabrics such as composites. Historically, reaching that spinnable quality has required additional refining beyond standard decortication, work that has fallen to third-party processors, or to the spinners themselves, upgrading standard decorticated technical fiber before it can run on their equipment. The commissioning of IND HEMP’s new processing line brings that refining capability in-house, at the fiber’s source.

“Consumers are increasingly looking for natural materials and more transparent supply chains, and brands are moving quickly to try to meet that demand. Hemp is an incredible plant-based solution, but until now the U.S. hasn’t been capable of consistently delivering the quality and scale the global textile industry requires,” explains IND HEMP CEO Morgan Tweet. “By supplying ready-to-spin fiber directly from Montana, we’re removing one of the biggest barriers for manufacturers wanting to work with hemp. This investment gives American-grown hemp the opportunity to compete on the global market, ultimately making its way into more of the products consumers want to buy.”

“This investment is a strategic step in IND HEMP’s growth trajectory because it converts more of our existing processing scale into higher-value, market-ready fiber. By adding premium refining capability at our Fort Benton facility, we can serve a broader range of textile and nonwoven customers, improve consistency and supply-chain efficiency, and respond to growing demand in both domestic and international markets,” shares Trey Riddle, CFO, IND HEMP.

Multiple Grades, Ready to Run

The new line allows IND HEMP to offer multiple grades of premium, cottonized fiber directly from its Fort Benton facility, ready for spinners and nonwoven manufacturers to use as supplied. Because refining now happens at the source, fiber yields and quality are improved, giving customers a more consistent fiber with better overall economics.

Built for Global Supply

“IND HEMP was built to operate at industrial scale, and today’s textile supply chain is global,” said Tweet. “This investment gives us ready-to-spin fiber we can put directly into international supply chains. We’re already shipping fiber to international markets in Asia and the Americas, with additional export partnerships in development, and we invite spinners, weavers, and manufacturers around the world to connect with us as a reliable, scalable source for premium U.S.-grown hemp fiber.”

Posted: October 6, 2026

Source: IND HEMP

Sponsors